
Welding a Joint Over a Metre Long
Automotive trim panels, large fascias and storage boxes routinely have joint perimeters over a metre. Customers ask whether a 1.2-metre horn exists, and the question itself points the wrong way.
Why a bigger horn is not the answer
A horn is an acoustic component: its length is tied to half a wavelength and its width is limited by amplitude uniformity. The wider the horn, the harder it is to keep every point of the working face moving by the same amount.
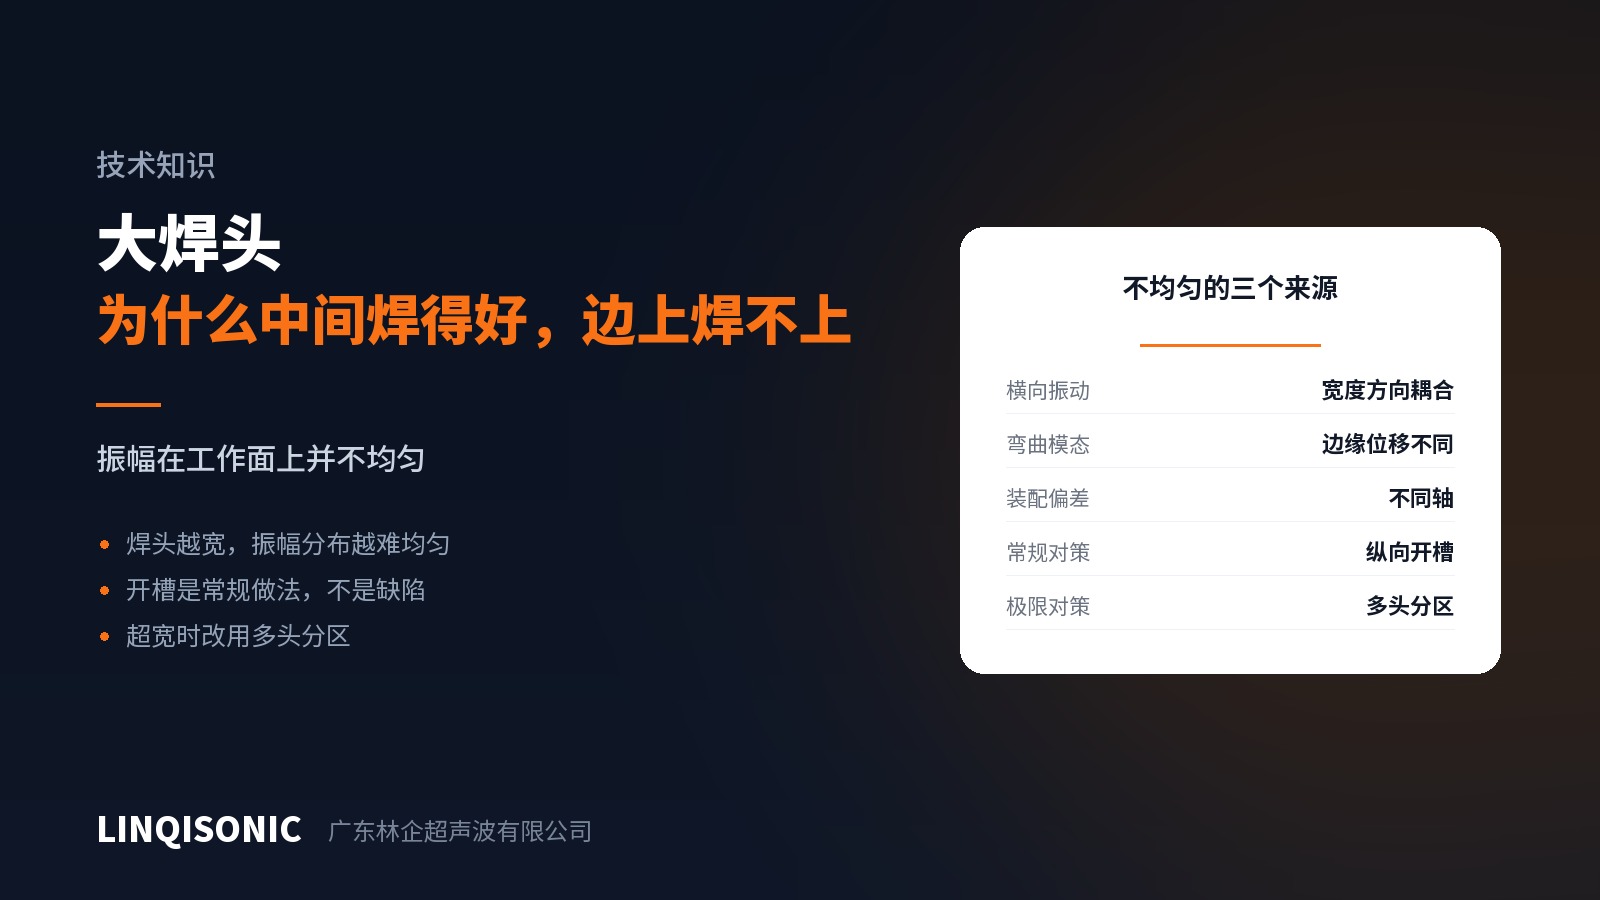
Two reasons. The Poisson effect produces lateral motion that grows with width and couples with the axial motion, disturbing the amplitude distribution. And wide, thin horns readily develop flexural modes, so the face flexes like a drumhead with quite different displacement at centre and edge.
The classic symptom follows: the middle welds well and the ends do not, or the ends flash badly. Parameters do not help, because parameters are not the problem.
Three routes
One: slots. Axial slots divide a wide horn acoustically into several narrow ones, suppressing lateral coupling and flexural modes. This is standard practice rather than a machining defect. It has limits, and beyond a certain width it no longer holds.
Two: zoned drive. Where the weld width exceeds what one horn can keep uniform, the correct answer is several horns each covering a section, each with its own converter. Every horn works inside its comfortable range and uniformity is assured, at the cost of machine complexity.
Three: sequential sections. Weld in several passes with one horn, or use a travelling rotary head. This costs cycle time but keeps the equipment investment low. Watch the overlaps, which are where weak points appear, and design the overlap length deliberately.
Move down in frequency
Large parts move down: lower frequency allows a larger horn, more available power and longer energy transmission. 15 kHz exists for exactly this work, with 20 kHz for moderate weld areas.
Decide this during selection, because frequency is a property of the whole acoustic system rather than a setting. Changing it means a different generator, converter, booster and horn.
Two more things
A contoured nest is mandatory. Large parts deflect under weld force, side walls splay and bases sink, so seating at the joint differs entirely from the unloaded condition. The nest must follow the part, take the force and hold the shape through the cycle. That cost cannot be saved.
The joint has to absorb tolerance. The larger the part, the greater the absolute shrinkage, warp and ejection distortion, and the gap cannot be identical all round. A shear joint relies on side-wall interference and is insensitive to height variation, far more forgiving than a butt joint.
Deciding whether zoning is needed
A simple shop-floor test: put thermal paper or thin weldable film under the working face, run a weld into air, and read the depth distribution of the mark. Deeper means higher amplitude, lighter means lower, and the distribution is visible at a glance.
If the mark fades noticeably from centre to edge, and that difference already leaves the edges unfused, it is time to consider zoning rather than searching further in the parameters.
Large horn design, slotting and maximum usable area are in the horn selection and design guide on the downloads page. Maximum weld area by frequency and multi-head configurations are on the ultrasonic welding machine pages.
Send the part envelope, joint perimeter and cycle requirement to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.