Stay updated with Linqi Ultrasonic news, industry trends and technical insights
100 articles
On parts with several joints made at several stations, vibration from the later weld reaches the joints already made. Sequence, support and frequency decide whether the earlier work survives.
Material compatibility, joint feasibility, energy access, then cosmetic and validation requirements — a conclusion needs all four. The order matters: if an earlier step fails, no parameter downstream means anything.
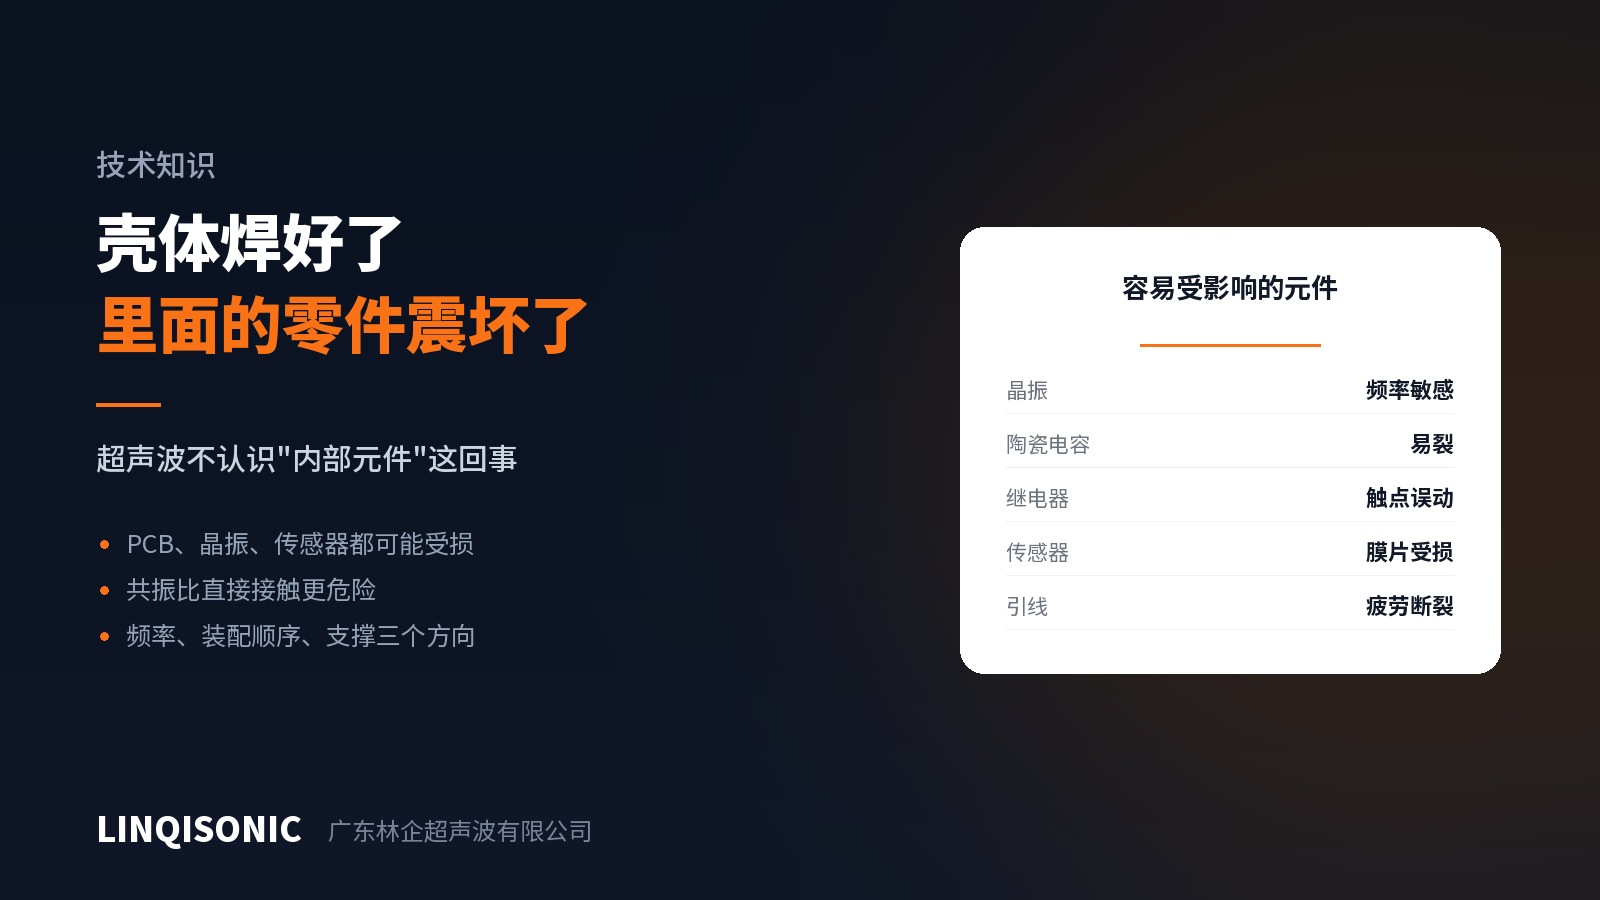
There is another kind of welding failure: the outside welds fine and the component inside is destroyed. The transmission path, resonance and how the component is held decide whether it survives.
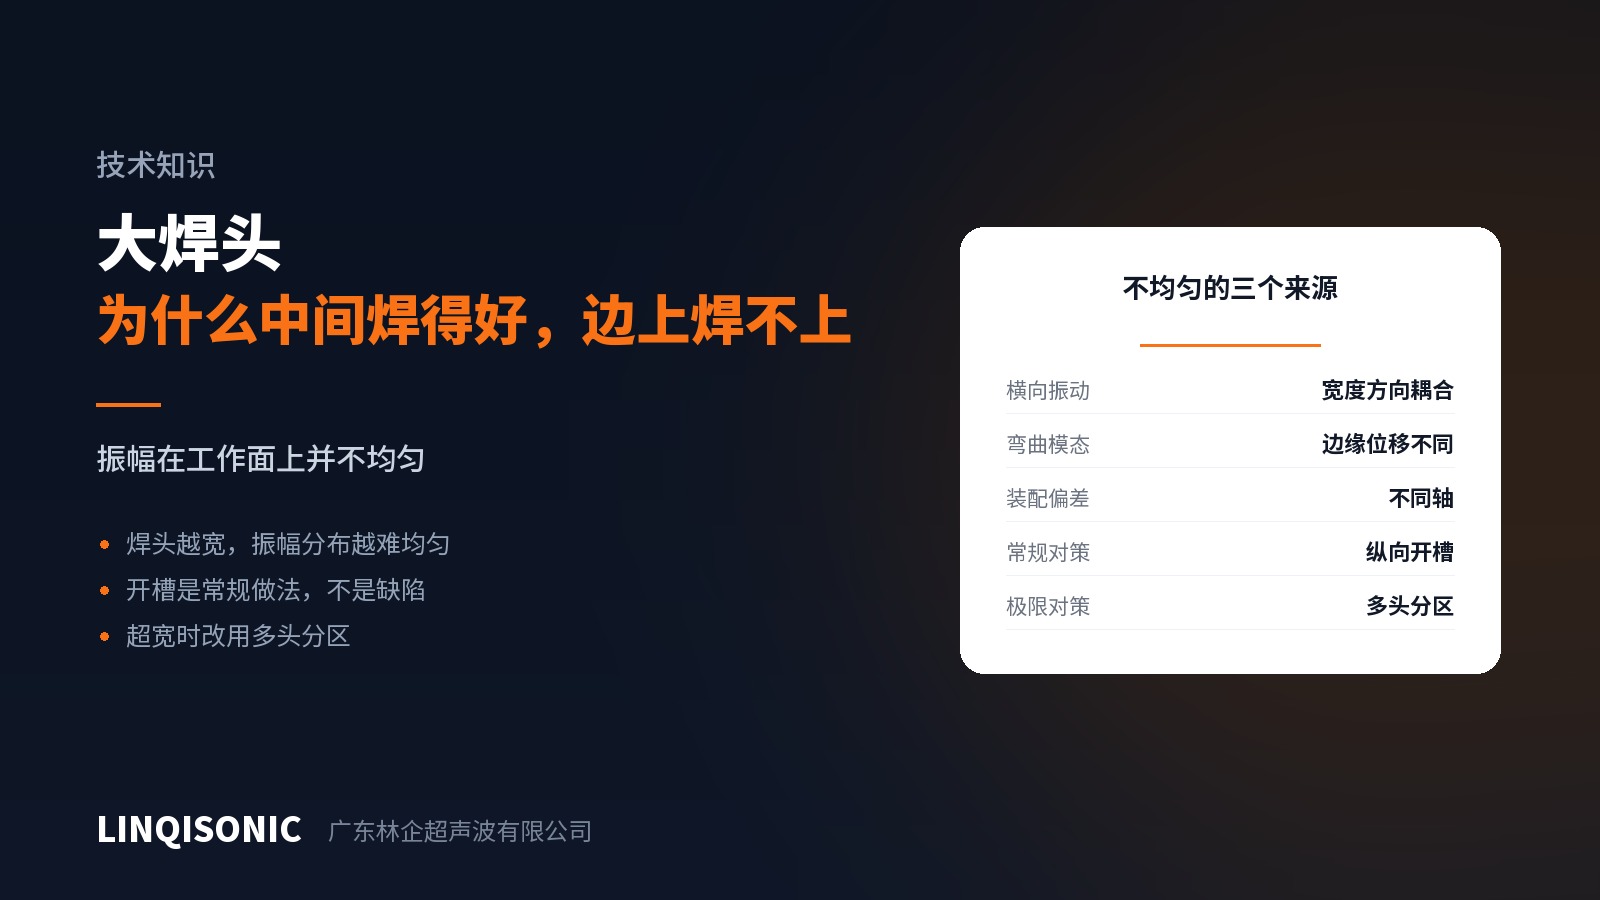
Parts that weld at the edge and open in the middle rarely have a parameter problem. Amplitude across a large horn is uneven and the part is least stiff at its centre, and the two effects add.
Contouring the horn face changes the distance from each point to the nodal plane, and the amplitude distribution changes with it. The difficulty on curved parts is getting every point to fuse at once.
On the same batch, different gripping and different loading rates give noticeably different numbers. The informative part is not the peak force but where the part broke.
Fatigue is a crack growing from a stress concentration, a different matter from carrying a load once. Fillets, flash and residual stress at the joint are where fatigue life starts.
Under impact the strain rate is high, materials behave in a more brittle way and plastic deformation has no time to occur. Notch sensitivity at the joint is amplified, and most drop failures show brittle fracture.
A transparent part magnifies every process defect into a cosmetic one. Whitening is light scattered by crazes, haze is a record of melt flow and witness marks come from the horn face. Each needs a different answer.