
PC Parts That Weld Fine and Crack Days Later
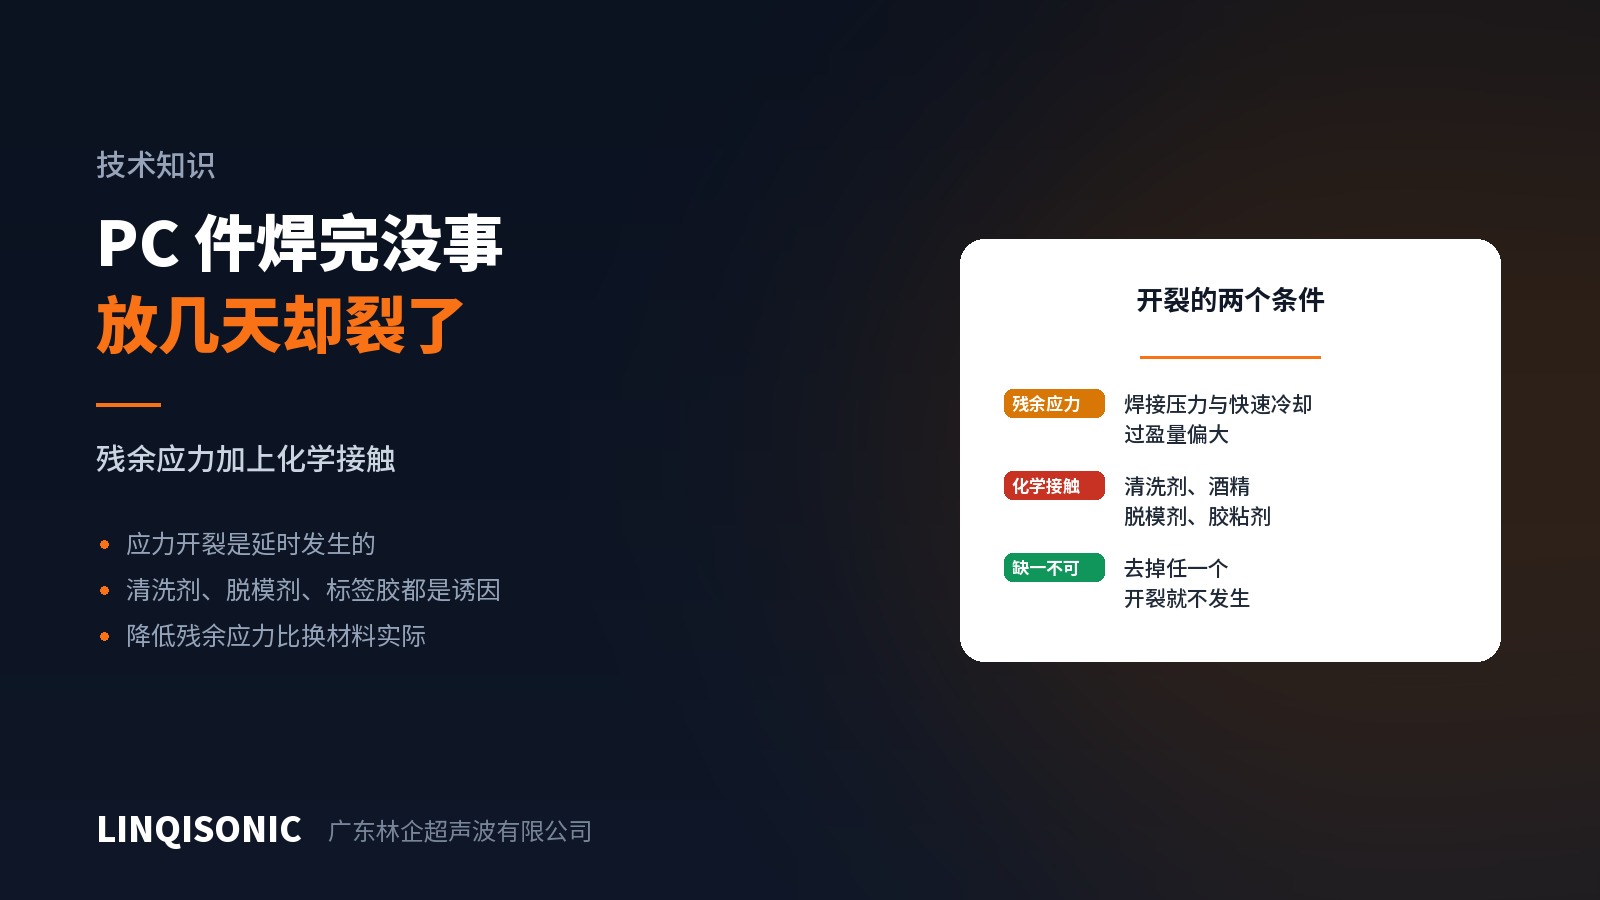
The classic complaint about PC parts: everything passes at the line — strength, sealing, all fine — and a batch starts cracking days later.
This is not a weld strength problem
The cracks usually appear beside the joint rather than in it. The weld is sound and the parent material has failed.
This is environmental stress cracking: residual tensile stress in the material plus contact with certain chemicals, and PC cracks at stresses far below its strength.
The key point is that both conditions are required. Stress without chemical contact does not crack; chemical contact without stress does not crack. That gives you two routes to a fix.
Where the stress comes from
Excessive weld force. More force locks more stress into the part.
Fast cooling and short hold. Melt that solidifies after force is released shrinks unevenly, leaving stress behind. Extending hold helps markedly.
Excessive joint interference. Too much interference on a shear joint keeps the side walls splayed, a permanent tensile stress.
Over-tight fixturing. A part forced flat or square in the fixture keeps that stress after release.
Moulded-in stress. Gate areas and abrupt wall transitions are already high-stress regions; welding only adds to them.
Where the chemicals come from
This half is often overlooked, because nobody thinks of these as chemicals:
Cleaners and alcohol — routine in wiping operations, and PC is sensitive to them.
Release agent residue — carried over from moulding and left on the surface if not cleaned.
Label and tape adhesive — cracking exactly where a label sits is a very common finding.
Lubricants and cutting fluid — splash in the workshop, and oil from hands.
Certain inks and coatings — solvents from printing and spraying.
How to attack it
Start with a test: remove the suspected chemical contact and see whether the cracking stops. Change the wiping agent, move the label, or shift cleaning to a different operation. This confirms stress cracking quickly.
Once confirmed, work both routes:
Reduce residual stress — lower weld force, extend hold, reduce joint interference, check for over-constraint in the fixture, and relax the joint design.
Break the chemical contact — use a PC-compatible cleaner, clean before welding rather than after, change the label adhesive, and check for release agent residue.
PC blends and modified grades
PC/ABS is less prone to stress cracking than unfilled PC, though not immune. Glass-filled PC behaves differently again, as the fibres introduce their own local stress concentrations.
Where the service environment guarantees chemical contact, that belongs in the material selection rather than being left for the welding operation to solve.
Force control and hold settings by machine are on the ultrasonic welding machine pages. Stress-cracking sensitivity by resin and joint design values are in the handbooks on the downloads page. Send photographs, resin grade and downstream process details to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.