
Why Battery Tab Welding Carries Such Tight Process Requirements
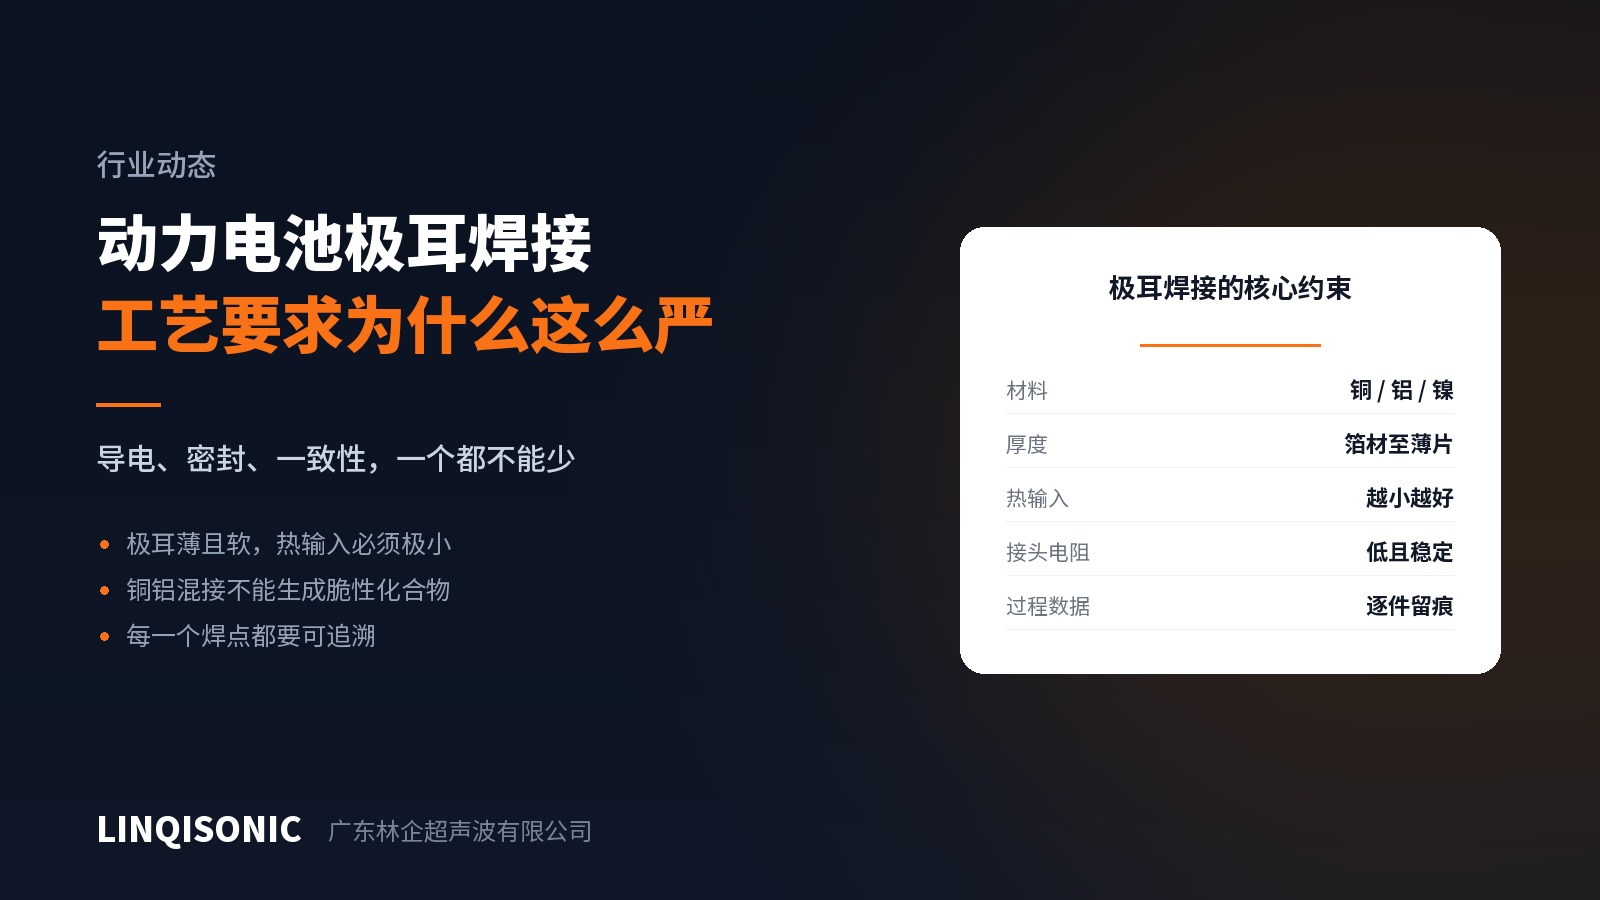
Tab welding is among the most closely watched joining operations between cell and module. The requirements are tight because three constraints bear on one very small weld at the same time.
Constraint one: almost no added heat
Tabs are thin copper, aluminium or nickel, connected directly to the inside of the cell. Any surplus heat can travel down the tab into the cell and affect separator and electrolyte — a safety matter, not a quality one.
That alone rules out most processes that melt the base metal. Ultrasonic metal welding is solid state: the base metal does not melt, heat input is concentrated at the interface and small in total, which fits the constraint naturally.
Constraint two: low resistance, stable for life
The tab carries the cell's entire working current. High joint resistance means continuous local heating, which accelerates ageing of both material and interface. Any single degraded weld becomes the weak point of the whole pack.
What is needed is not low initial resistance but resistance that stays stable across the service life. A solid-state weld is a continuous piece of metal, with no mechanically maintained contact interface and therefore no mechanism for gradual degradation.
Constraint three: copper-to-aluminium intermetallics
Tab-to-interconnect and in-module connections frequently require a copper-aluminium transition. Melt the two together and cooling inevitably produces hard, brittle intermetallic compounds, and the joint cracks under vibration and thermal cycling.
Without a melt pool, the problem does not arise. That is why ultrasonic welding is close to irreplaceable at this step.
And traceability on top
Traction batteries carry mandatory traceability. Process data for every weld — energy, power, force, pre- and post-weld height — may need to be retrieved years later.
The equipment therefore has to set monitoring limits per weld, alarm on deviation, and store and export the data. This is not a bonus feature; it is an entry condition.
Our ultrasonic metal welding equipment monitors and alarms on weld time, energy, force, amplitude, power, and pre- and post-weld height, and stores and exports weld parameters. See the ultrasonic welding machine pages.
One caution
Tab welding parameters do not transfer. Tab material, layer count, thickness, interconnect specification and fixture rigidity all change the result, and any change calls for re-validation. The sound approach is to trial, run pull and resistance testing, then lock the parameters in with process monitoring.
Send material, layer count, thickness and joint configuration to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.