
Welding Stacks of Foil: Getting Through Dozens of Layers at Once
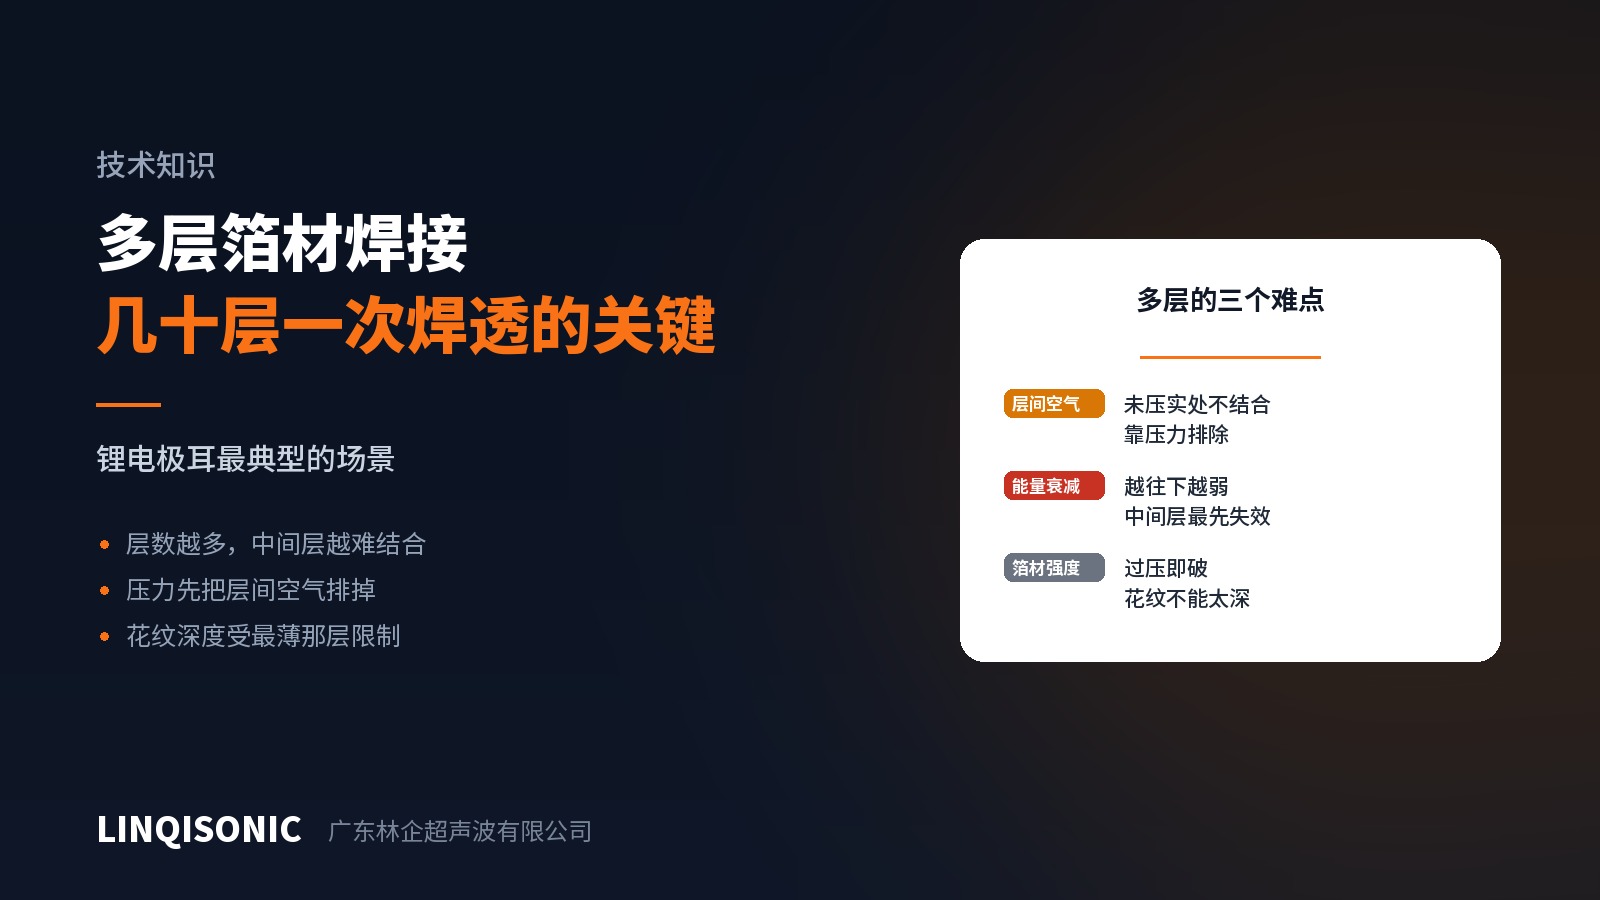
Battery tabs, supercapacitor leads, transformer foil windings — all require dozens of thin foil layers joined in a single operation, with every layer bonded, resistance low and pull strength adequate.
This is the most demanding class of work in metal ultrasonic welding.
Difficulty 1: energy attenuates downward
Shear enters the top layer from the horn and passes down layer by layer, losing energy at every interface. So layers nearest the horn bond best and the bond weakens with depth.
The actual failure is rarely the bottom layer but several layers below the middle — neither driven directly by the horn nor restrained directly by the anvil.
Section a failed joint and the picture is typical: the top layers solidly bonded, the bottom layers acceptable because the anvil held them, and the middle loose. That signature says the layer count has exceeded what the current parameters can reach.
Difficulty 2: air between layers
Dozens of foils stacked together cannot seat perfectly. Wherever they do not, shear cannot pass and no bond forms.
Force therefore matters more in multi-layer work than in single-layer — its first job is not to press the interface but to expel air and gaps and turn the stack into one body.
In practice this means multi-layer force is generally higher than for the same material in one layer, and the trigger method is critical: ultrasound should start only after force has genuinely built and the stack has consolidated, which makes force trigger more dependable than position trigger.
Difficulty 3: foil is weak
Thin foil has limited strength and tears if the knurl bites too deep, yet multi-layer welding needs firm grip. The two requirements conflict.
The result is that knurl depth is limited by the thinnest layer, not chosen from total thickness. This is why multi-layer tooling has to be designed for the job rather than borrowed from single-layer work.
Direction
Force first. Set force high enough to consolidate the stack reliably before touching anything else. With insufficient force, nothing else helps.
Trigger on force. Ensure the stack is consolidated before energy goes in.
Amplitude on the high side. Compensating for layer-by-layer attenuation so lower layers still receive enough shear.
Weld in stages. Where the count is genuinely high, bond a portion into a sub-group first and then join the groups, keeping each operation within a manageable count.
Pre-compact the stack. A pressing operation before welding consolidates layers and reduces trapped air.
Control incoming material. Foil flatness, freedom from wrinkles and edge alignment decide layer seating directly. Untidy material cannot be recovered in process.
Verification
Section and inspect every layer. The only way to confirm the middle; neither appearance nor pull strength reveals it.
Pull in the right direction. Peel and shear load the joint differently; choose by actual service condition.
Measure resistance. Poor interlayer bonding shows first in contact resistance, a more sensitive indicator than pull strength and one that can be applied to every part.
Frequency
Multi-layer foil work commonly runs at 20 kHz, which has the advantage where greater energy transmission and larger weld area are needed. Small areas with fewer layers can use 30 or 40 kHz.
Power, force control and trigger options by machine are on the ultrasonic welding machine pages. Send material, single-layer thickness, layer count and weld area to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.