
Precision Components Inside the Cavity: Keeping the Vibration Away from Them
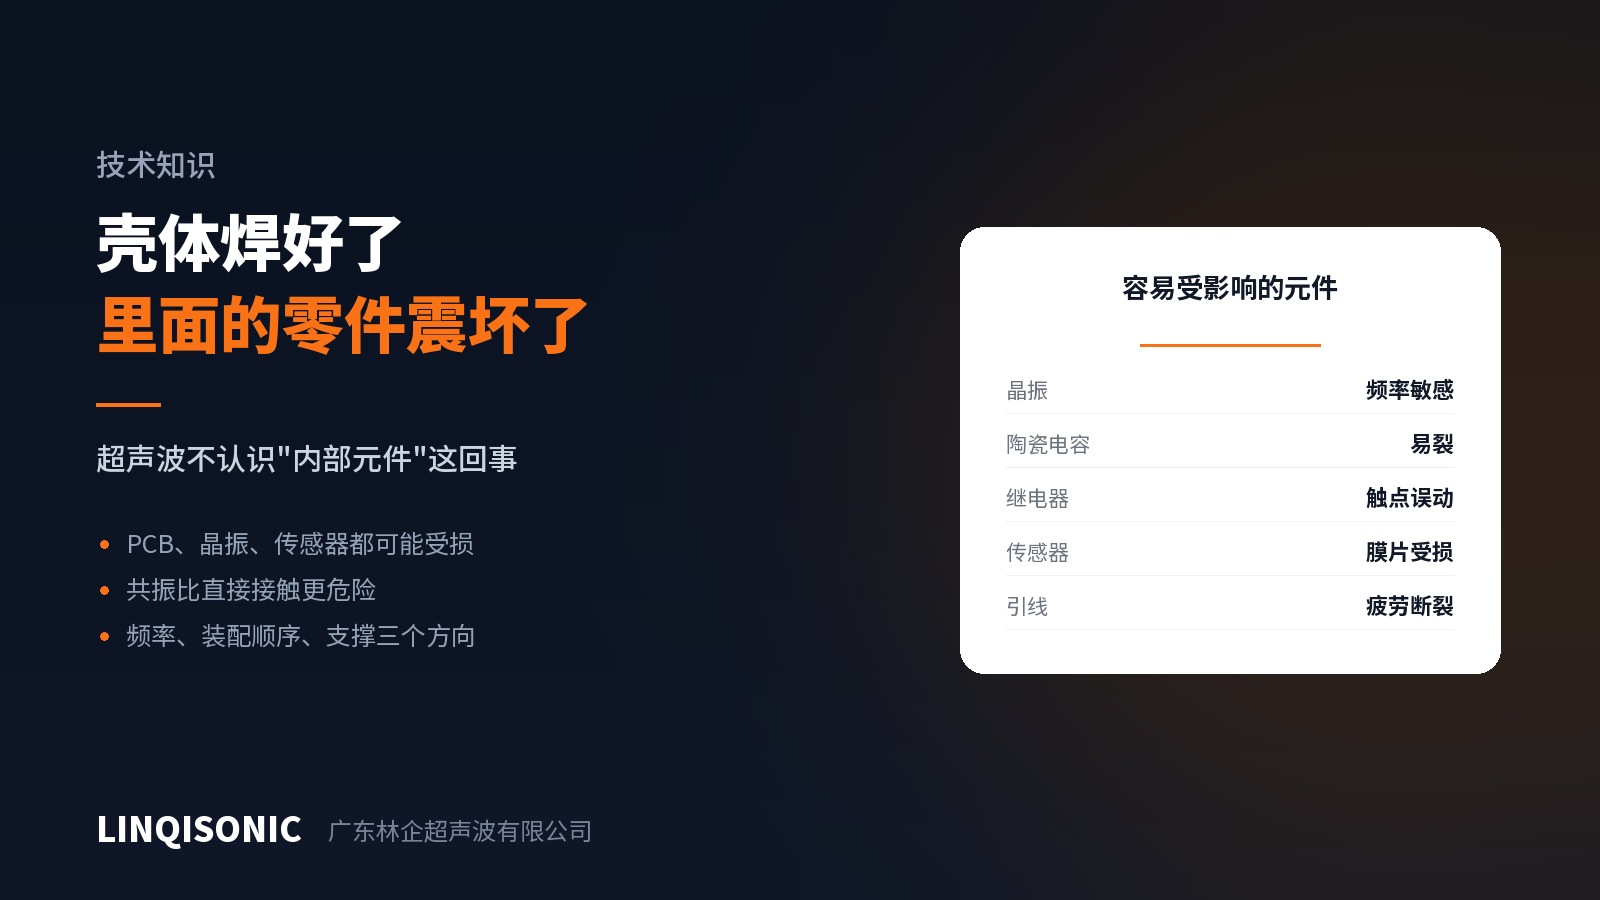
On sensor housings, electronic modules and assemblies containing a diaphragm or a crystal, the difficulty is not the joint but keeping the ultrasound on the path it should take. A perfect-looking weld on an assembly that no longer works is the hardest failure to diagnose.
How the damage happens
Three paths.
One: direct transmission. A component in rigid contact with the housing receives the vibration directly. Rigid contact includes a component pressed against the housing, held in a hard bracket, or potted in a rigid compound.
Two: resonance. If the component, or its leads, cantilevers or diaphragm, has a natural frequency near the welding frequency or one of its harmonics, even a small amount of transmitted energy is amplified into large motion. Slender leads, thin diaphragms and cantilevers are the most at risk.
Three: heat. Heat from the joint conducts along the housing and reaches components nearby. This matters most for heat-sensitive parts and for gaskets already fitted.
Six things that help
Break the rigid path. Put a compliant medium between component and housing — foam, a silicone pad, a sprung bracket. Soft material both isolates and damps, and this is the most effective single measure.
Increase the distance. Amplitude decays along the path, so the further the component sits from the joint the safer it is. Place sensitive parts at the far end during design.
Change the frequency. Where resonant damage appears at 20kHz, moving to 15kHz or 35kHz often avoids it. This is one of the most direct remedies available, provided the equipment offers the choice. Our machines cover 15kHz to 40kHz, so the selection can follow the sensitive band of the internal component.
Lower amplitude and shorten time. Less total energy means less reaching the interior. Joint design has to support it: an efficient joint needs less energy.
Change the joint form. A shear joint concentrates energy at the mating faces and spreads a smaller share into the housing than an energy director does.
Control the heat. Shortening weld time works better than reducing power, because conduction takes time. A high-amplitude, short-time combination gives a smaller heat-affected region.
Verifying the component survived
Neither appearance nor pull testing reveals internal damage, so functional testing is required.
Before and after comparison. Measure the key functional parameters on the same unit before and after welding and look for drift. This is far more sensitive than a pass/fail check afterwards and catches units that pass while already degraded.
Test at aggravated settings. Weld a batch at amplitude or time above production values and find where function begins to degrade. That boundary is the top of the process window, and production settings should sit well below it.
Retest after ageing. A component damaged by vibration but not yet failed may fail months later. Retest after thermal cycling or vibration ageing.
Trial first, then fix the structure
Feasibility here cannot be calculated, only tried. The sensible sequence is welding trials on prototypes or similar existing parts before the tool is cut, establishing the parameters at which the internal component is safe, and setting the joint position, component position and mounting method from that.
Reversed, the damage is discovered after the tool exists, and the change becomes expensive.
Frequency selection, joint forms and energy control are on the downloads page. Machines from 15kHz to 40kHz with amplitude and energy modes are on the ultrasonic welding machine pages.
Send the type, location and sensitivity of the internal components to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.