
The Housing Welded Fine — but the Electronics Inside Did Not Survive
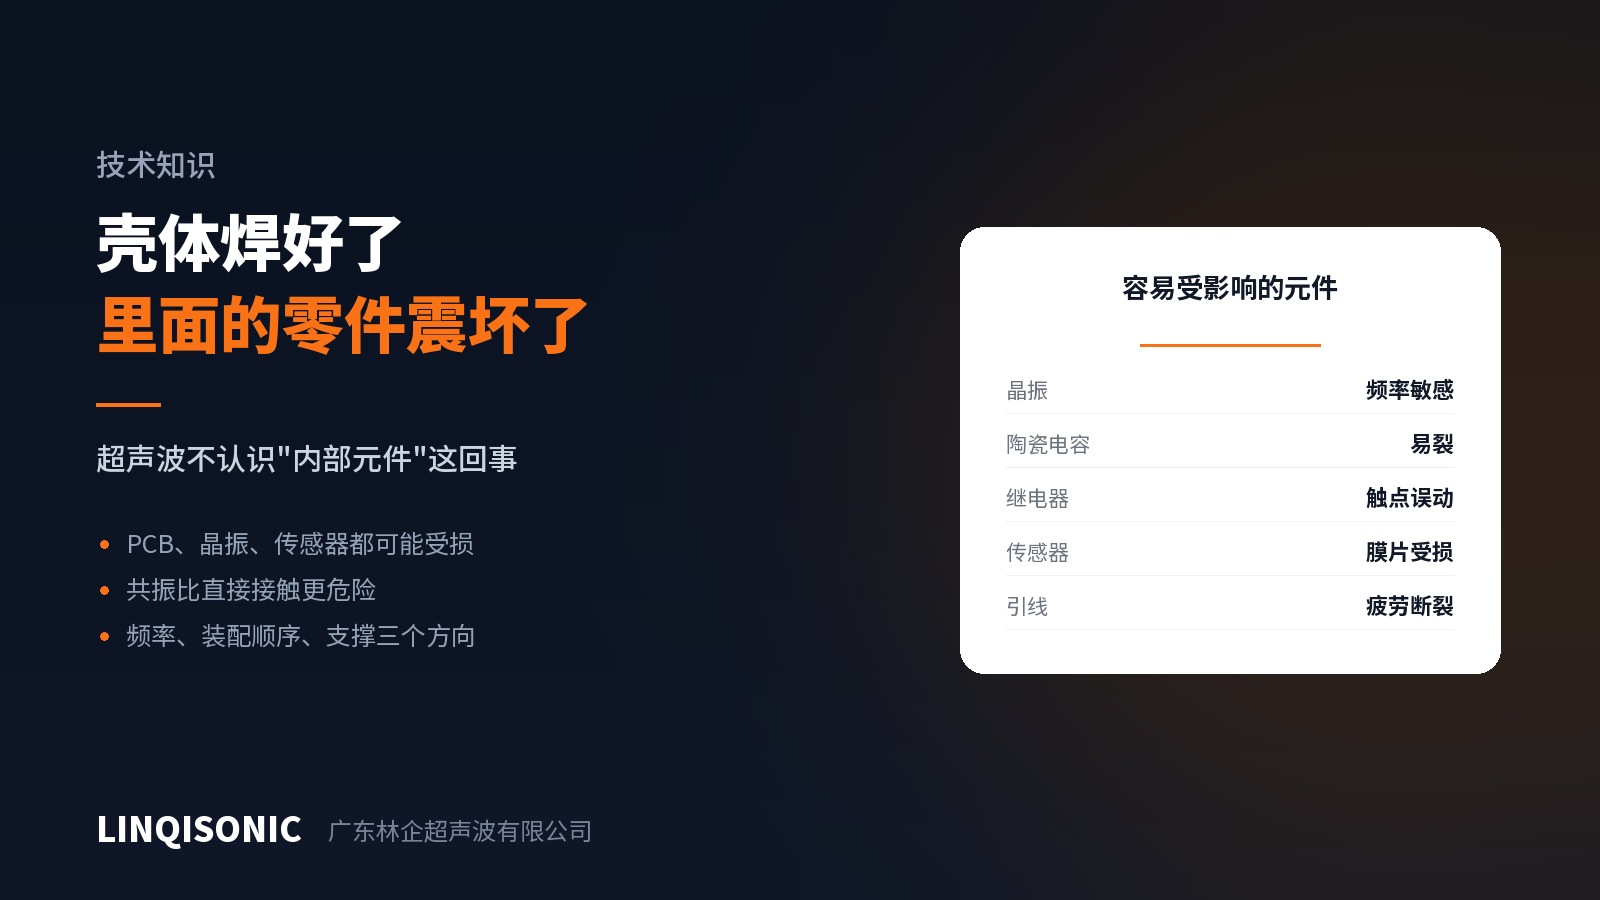
Welding electronic housings brings one particularly elusive problem: the joint is sound, appearance is fine, the seal passes — and the product fails electrically, with damaged components found inside.
Vibration travels inward
Ultrasonic vibration propagates through the housing and does not stop because there are electronics inside. It reaches the PCB, the component leads, and anything in contact with or coupled to the housing.
Vulnerable items include crystals (frequency-sensitive by nature), ceramic capacitors (brittle, prone to cracking at the lead root), relays and micro-switches (contacts can chatter or shift), sensor diaphragms (thin structures sensitive to vibration), and fine leads and solder joints (fatigue).
Resonance is worse than contact
Vibration transmitted by direct contact attenuates with distance and is usually manageable. The real difficulty is resonance — a PCB, a cantilevered bracket or a long lead whose natural frequency falls near the ultrasonic frequency will see markedly amplified motion, and damage appears somewhere unexpected.
Resonance damage has a signature: the same location every time, unrelated to distance from the joint, and appearing across a batch. If every failure is the same component in the same place, resonance is almost certain.
Three directions
1. Change frequency. The most direct measure. Moving from 20 kHz to 30 or 40 kHz changes the resonance condition; higher frequencies also mean lower amplitude and shorter energy transmission distance, which is gentler on internal components. The trade-off is available power — rarely a constraint on small, thin electronic housings.
2. Change the assembly sequence. Can the housing be welded before the electronics go in? For many products the sequence is negotiable, and this is the most complete solution. Where sealing forces the opposite order, consider fitting sensitive components last through a sealable access.
3. Support and damp internally. Hold the PCB firmly within the housing rather than leaving it suspended on a few bosses; an unsupported board resonates readily. Add damping between board and housing where necessary.
Further measures
Shorten weld time. Less exposure means less cumulative damage. Energy mode with higher amplitude and a shorter cycle is usually kinder to internal components than a long, low-amplitude weld.
Move the horn contact point. Introduce vibration as far as possible from sensitive components, preferably with structure in between.
Change the joint form. A shear joint concentrates energy at the mating faces and spreads less of it into the part body than an energy director.
Verification
Do not rely on appearance and leak testing alone. Functional electrical testing after welding is essential, ideally with thermal cycling or vibration ageing — some damage is undetectable at despatch and only fails in the customer's hands.
Available frequencies by machine are on the ultrasonic welding machine pages. Send assembly drawings, internal layout and the location of sensitive components to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.