
Millimetre-Scale Parts: Small Enough Becomes Hard Again
Sensor housings, miniature valves, connectors and microfluidic medical parts measure only a few millimetres. Intuition says small parts should be easy; past a certain size the difficulties simply change.
Where the difficulty is
A small energy window. A small part needs little total energy, while the machine's smallest controllable increment does not shrink with it. It is like weighing a gram on a large scale: the resolution is short and a little too much overshoots.
No room for joint geometry. A director needs height, a shear joint needs engagement depth, and flash needs a trap. On a part of a few millimetres these features compete for space and often will not fit.
Location tolerance is magnified. On a small part, a given deviation is proportionally larger. A tenth of a millimetre is nothing on a 100mm part and one part in thirty on a 3mm part.
Handling is hard. Loading small parts by hand is slow and inconsistent; automatic feeding needs bowls and grippers that cost more than the machine. Many small-part projects are limited by handling rather than welding.
Move up in frequency
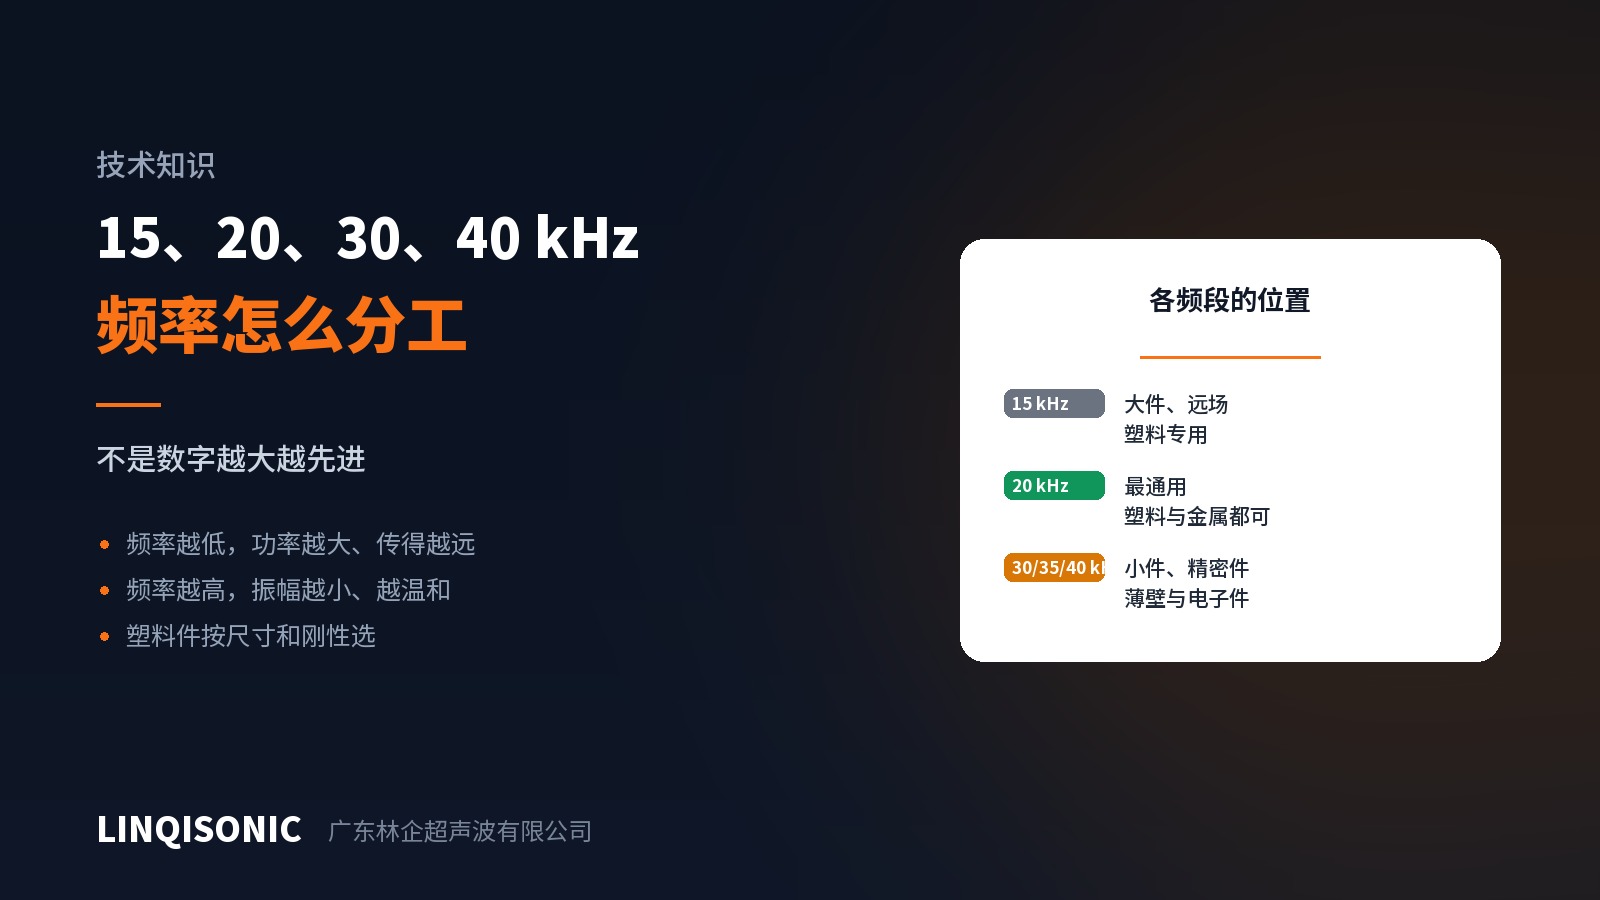
Small parts move up: 40 kHz gives low amplitude and a gentle mechanical action, and the horn is compact enough to reach into confined positions. The trade-off is less power and a smaller area, which small parts do not need anyway.
30 or 35 kHz is the middle choice for small and medium precision parts.
The fixture is most of the engineering
On small-part projects the fixture is often more complex than the machine, and it has to solve several things.
Accurate, repeatable location. Few, accurate features with a nest that follows the contour. Pin wear affects small parts far more than large ones, so set the check interval by piece count.
Easy loading and unloading. Too close a fit and the part will not go in or come out; too loose and location is gone. Lead-in chamfers and ejectors are usually needed, or vacuum to hold and positive air to release.
Venting. Small deep nests trap air most readily, the part floats on a cushion, and weld height varies part to part. Cut vent grooves or drill through the base.
Possibly several at once. For cycle time, small parts are often welded several per stroke, and then uniformity of amplitude and pressure across the nests becomes the new difficulty — the same problem as amplitude uniformity on a wide horn.
Mode and monitoring
A small window means energy or depth mode; time mode lacks the resolution. Use multi-dimensional monitoring as well, with limits on energy, power and post-weld height. Defective small parts are almost impossible to spot by eye, so the data has to do it.
Destructive sampling on small parts is cheap, so set a higher sampling rate and use it to calibrate the monitoring limits.
Do the arithmetic first
Before starting a small-part project, work out the split: seconds to weld, seconds to load and unload, minutes to change over. If handling dominates the cycle, the investment belongs in automation rather than in the welder.
This is regularly overlooked, and the result is the right machine with the output still short.
Frequency options, maximum weld area and multi-dimensional monitoring are on the ultrasonic welding machine pages. Joint forms and the dimensional system are on the downloads page.
Send the part size, daily output and handling method to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.