
Large Flat Parts That Will Not Weld in the Middle
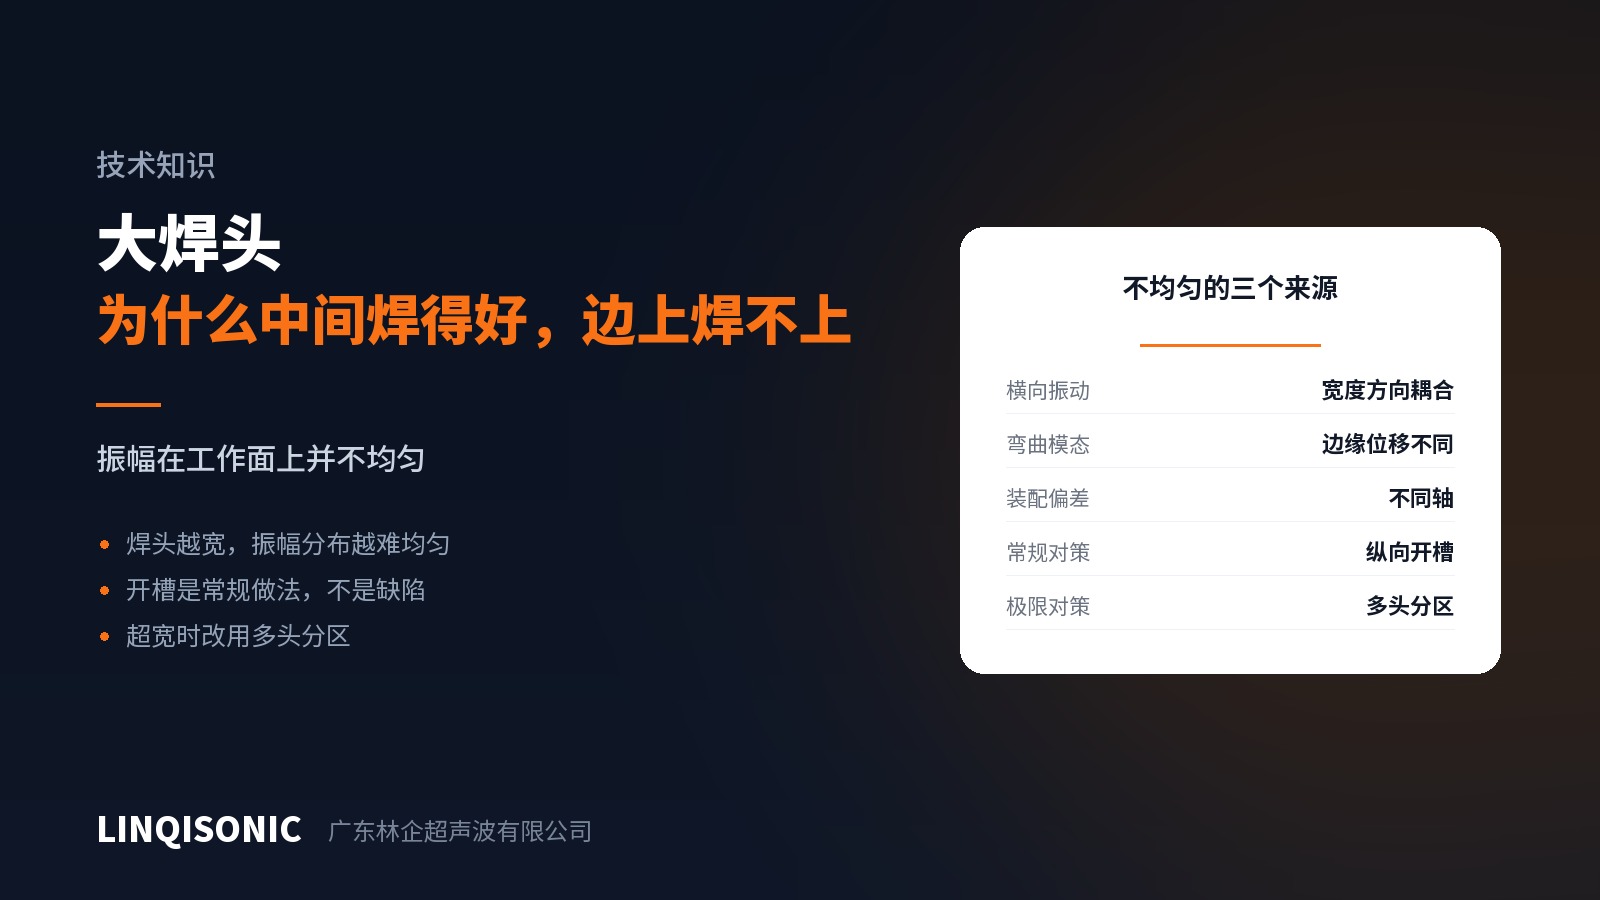
On panels, covers and trays the classic symptom is a good weld all round the edge and a middle section that opens under a light pull. Raise the energy and the edges start marking while the centre still will not fuse.
Three causes stacked together
One: uneven amplitude across the horn. A horn is a metal body designed to resonate, and the larger it is, the harder it becomes to hold amplitude uniform across its face. Large horns need uniformity optimised at the design stage and measured at points across the face after manufacture to confirm the distribution is within tolerance. A large horn that has never been checked for uniformity is normally weak in the middle.
Two: the part is least stiff at its centre. Bending stiffness at the middle of a large flat part is far below that near the side walls. Under weld force the middle deflects, contact pressure between horn and part actually falls there, and energy does not transfer.
Three: accumulated flatness error. Moulding warpage scales with size. A few tenths of a millimetre is irrelevant on a small part and is enough to leave the middle unseated across a span of several hundred millimetres.
The corresponding answers
The fixture must support the whole face. First priority. A fixture for a large flat part cannot support only the edges; it has to follow the contour across the whole area and hold deflection under weld force to a minimum. Fixture machining accuracy directly determines weld quality here.
Design the joint in segments rather than welding everything at once. Where sealing is not required, converting a continuous joint into segments concentrates the energy into a few sections and works far better than one long shallow weld.
Add ribs or locating posts in the middle. Raise local stiffness at the centre so it can carry the weld force. This has to be raised at the drawing stage.
Adjust the energy director by zone. Making the director slightly taller in the middle compensates for the seating difference. It is a tool adjustment, directly effective, and needs trial verification.
Weld in several passes with several horns. Rather than one large horn in a single shot, use several smaller horns over zones. Amplitude uniformity is easier to control on each, and force is easier to apply evenly.
The equipment layer
Large parts place two specific demands on the machine.
Parallelism on descent. A frame that lacks rigidity, or slop in the guides, tilts the horn as it descends, and on a large part that becomes visibly deeper on one side. Frame rigidity and guide accuracy matter far more here than on small parts.
Power margin. A large weld area needs high power, and insufficient power shows up as failing to fuse no matter how long the time. Estimate from the actual weld area and material at selection, rather than extrapolating from experience with small parts.
Frequency choice. Large horns are harder to make uniform at higher frequencies, so large flat parts usually run at 15kHz: the longer wavelength makes uniform amplitude easier to achieve at a given size, and permits a larger horn face.
Validate before fixing the dimensions
Feasibility for large parts belongs in the design stage: how large the weld area is, which material, whether it must seal, whether segmentation is permitted. Those four decide between a single large horn, several horns, or a different process altogether. Discovering after tooling that it will not fuse leaves very little room to change.
Large horn design and segmented joints are on the downloads page. High-power 15kHz machines and maximum weld sizes are on the ultrasonic welding machine pages.
Send the part size, material and joint layout to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.