
Medical & Hygiene超声波焊接
No adhesive, no solvent, no particles - welds that can be validated and traced
Medical and hygiene parts ask something different of a joint: no adhesives or solvents, no particles shedding, welds that survive sterilisation, and traceable process data for every single part. Ultrasonic welding adds no third material, keeps heat at the joint interface for milliseconds, forms a molecular bond in seconds, and logs energy, time and collapse part by part. On the plastics side it covers infusion and dialysis consumables, syringes and catheter fittings, diagnostic cassettes and microfluidic chips, and filter or vent membranes inside housings. On the nonwoven side, ultrasonic cut-and-seal does the cutting and edge sealing in one operation, leaving a clean edge with no fraying. Equipment can be configured to cleanroom requirements.
Typical Welded Parts
Common ultrasonic welding and cutting stations in this industry
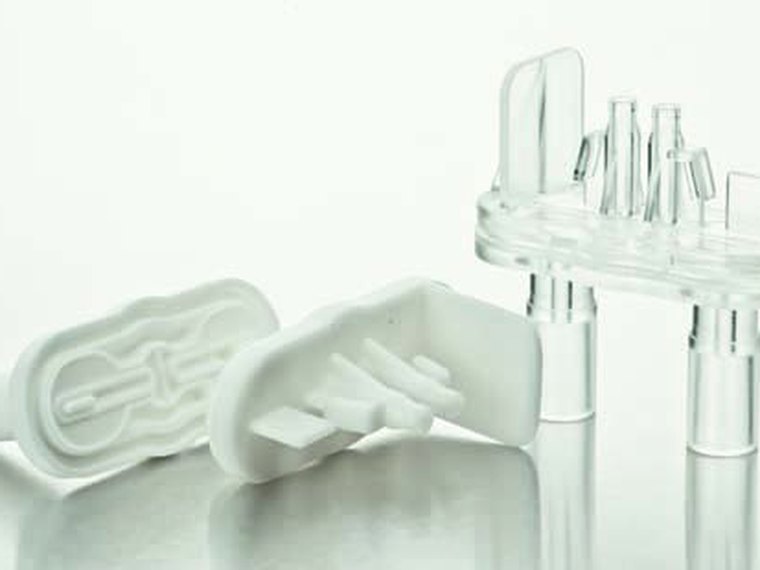
IV drip chambers and spikes
A hermetic weld all round with no flash breaking loose inside the fluid path - a shear joint formed over the full perimeter
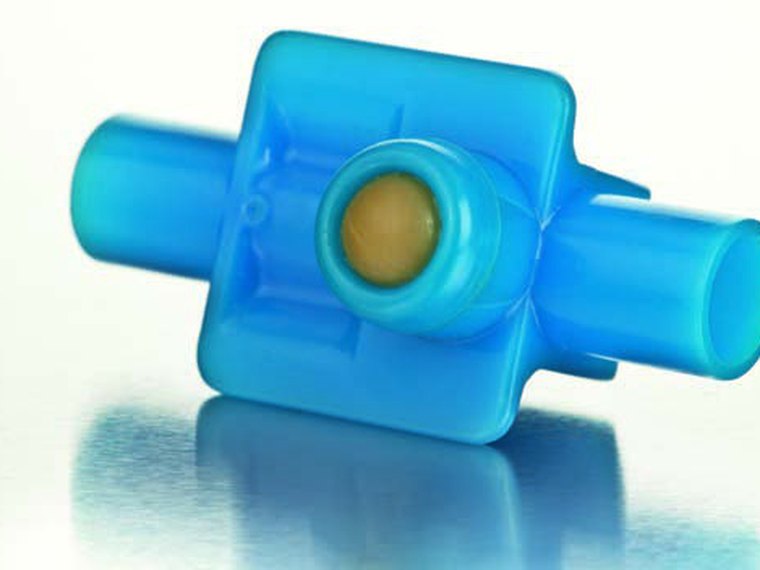
Injection sites and Y-connectors
Several ports sealed at once, resisting repeated needle penetration and flushing, with a contoured fixture holding the part
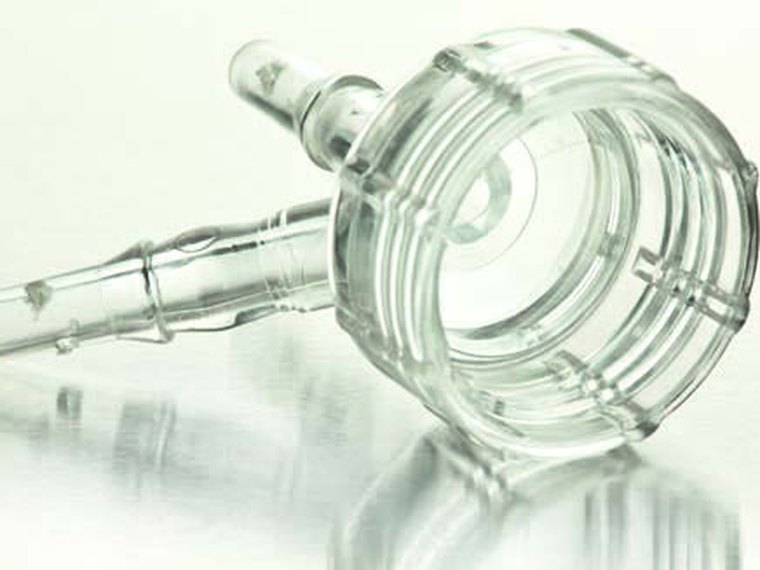
Luer fittings and catheter connectors
Dimensional tolerance sets connection reliability and seal grade; the servo holds total height by absolute distance
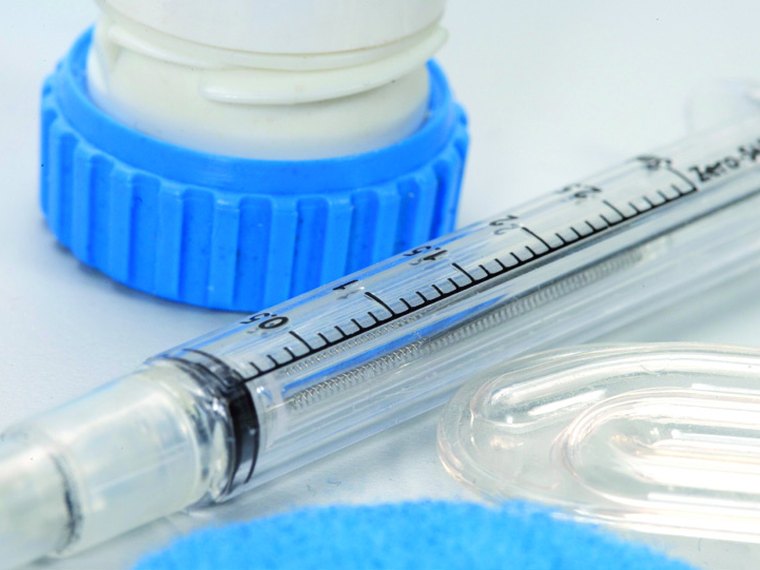
Syringe assemblies
The plunger must travel smoothly and the weld must not shed particles into the drug path - low amplitude, short time
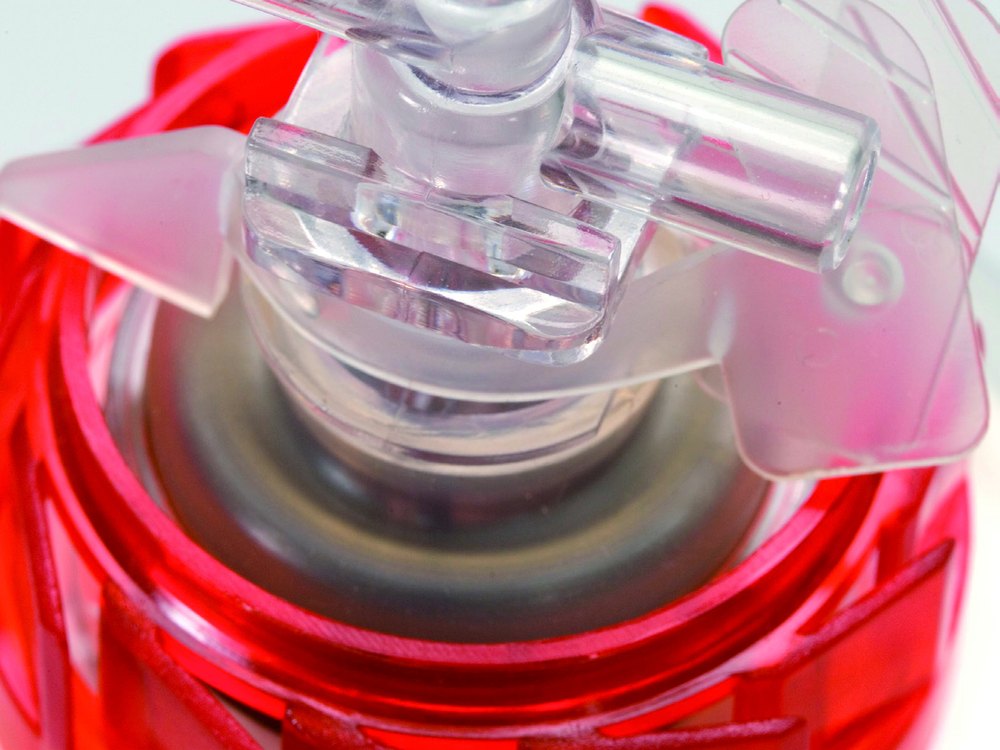
Blood-line components and valve bodies
Blood-contacting containers and stopcock bodies - the weld must stay continuous, pore-free and survive sterilisation, controlled in energy mode
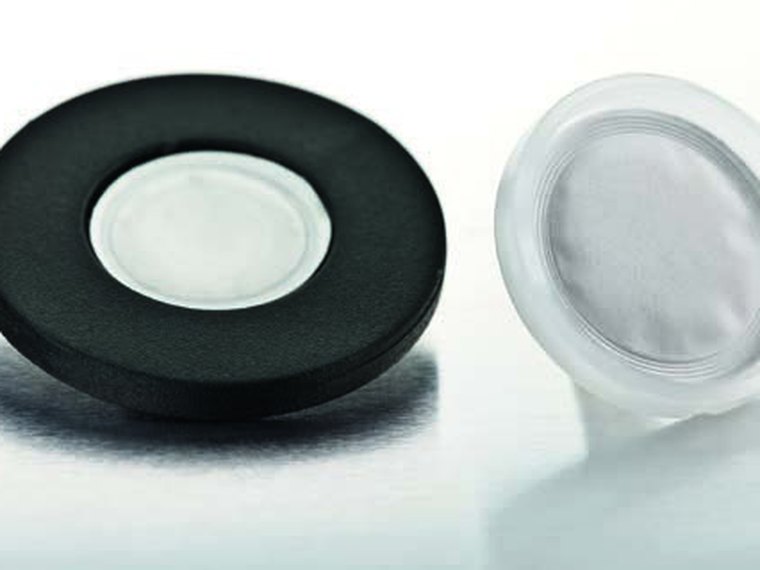
Filter and vent membranes in housings
The membrane is thin and tears under longitudinal vibration - torsional welding leaves it intact, and a vacuum horn can pick it up
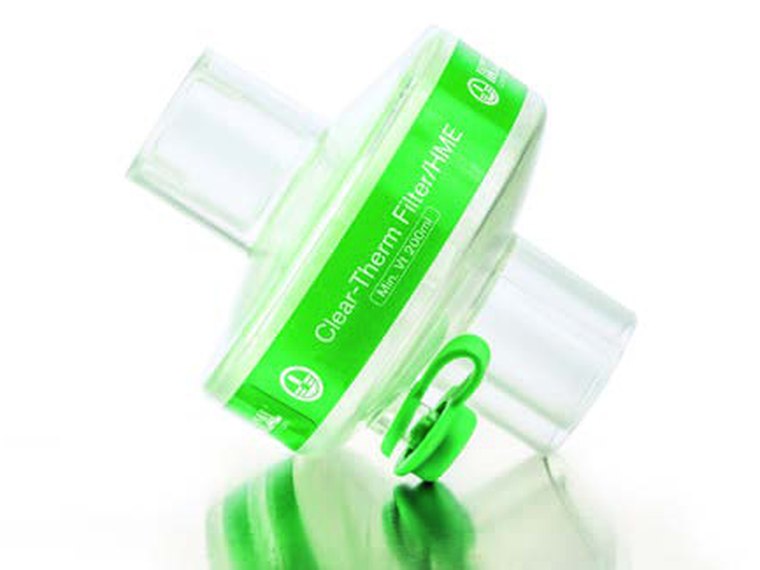
Breathing air filters
A continuous ring weld with no leaks, and airflow resistance that must not change after welding
Filter screens and cartridges
Media bonded to the frame over the full perimeter so it holds under backflush - a shear joint carries the strength
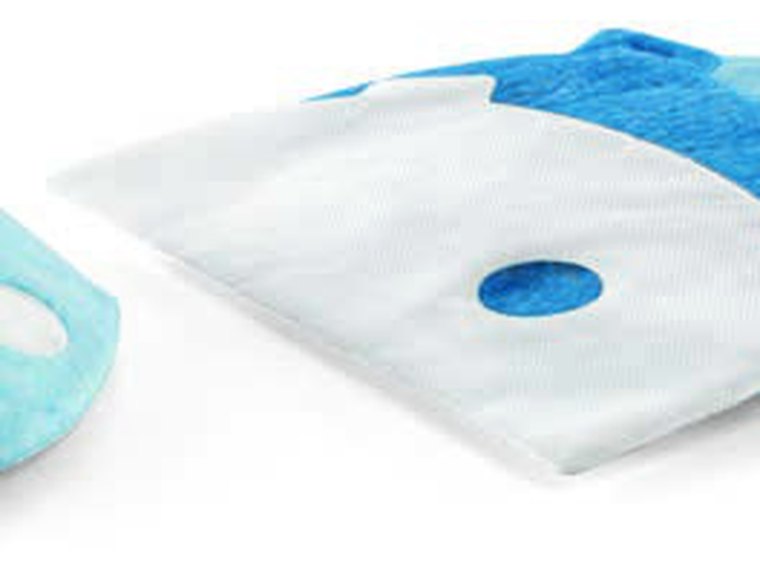
Mask ear loops and nose clips
Spot welds that hold without stiff burrs pressing on the face - low amplitude spot welding with a rigid fixture
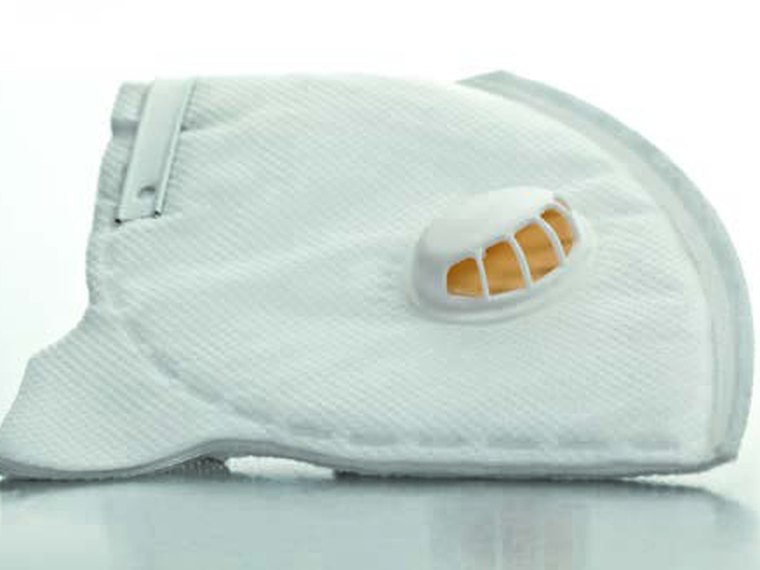
Mask body cutting and sealing
Multi-layer filter media cut and edge-sealed in one operation, leaving a clean, fray-free edge; hard tools can be reground
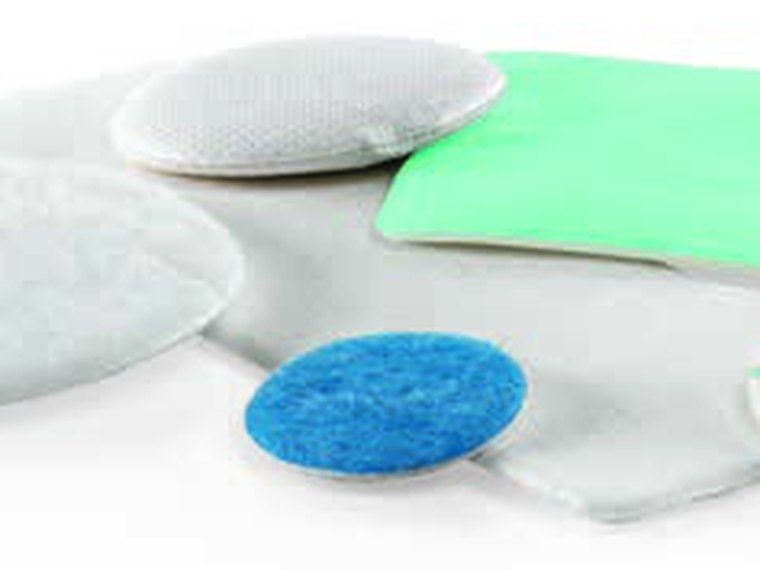
Wound dressings and bandage edges
The edge must be perfectly sealed so no fibres enter the wound - cutting and edge welding happen together
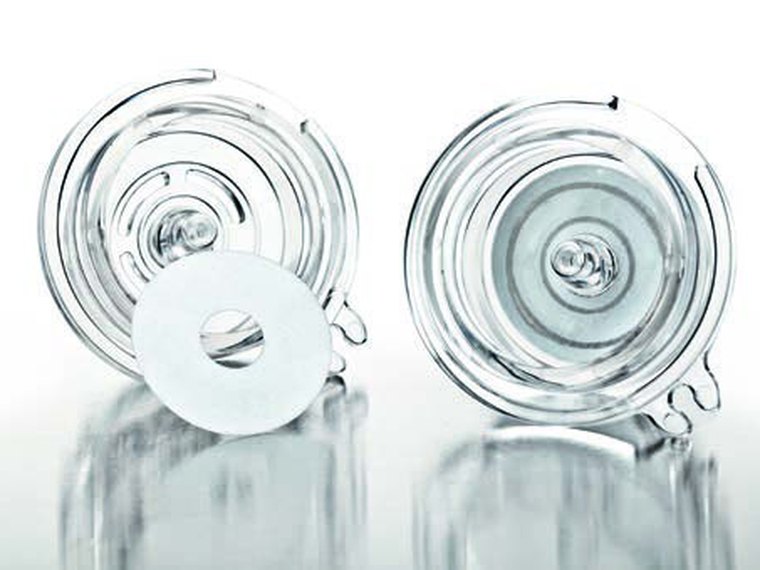
Diagnostic cassettes and microfluidic chips
Channel dimensions must not distort and the weld must be clean with no internal flash; COC/COP and PMMA need trials first
Why LINQISONIC
From joint design to line integration, we solve one thing: welds that hold and stay consistent
No third material introduced
No adhesive, solvent or solder. No curing wait, no biocompatibility risk from solvent residue, no fasteners taking up space. The material stays single-composition, which keeps sterilisation and recycling simple.
No particle generation
Melt bonding produces no chips or spatter, and ultrasonic cutting seals the nonwoven edge as it cuts so fibres cannot shed. For infusion, dialysis and dressings that touch the patient, this is the hardest requirement of all.
Process data for every part
Energy, time and collapse are logged for each part and can feed MES for CpK and 100% process monitoring, giving process validation real data instead of inference from sampling.
Configurable for cleanrooms
Material selection, surface treatment and lubrication can be specified to cleanroom requirements to limit dust generation and accumulation. The exact class must be confirmed against your line environment.
Cut and seal in one operation
Nonwovens and thermoplastic-containing technical textiles are cut and edge-sealed in a single pass by an ultrasonic wheel or die, giving a cleaner edge than hot cutting; hard tools can be reground repeatedly.
Weld trials before commitment
Send us the part or the drawing. We weld samples first and run pull and leak tests, then fix the joint design, horn, fixture and machine configuration.
医疗与卫材超声波焊接与切割技术
输液透析耗材、导管接头、口罩敷料与过滤透气件的焊接与切割工艺。含三种接头形式的推荐尺寸、材料可焊性矩阵,以及 12 类典型零件的要求与做法。
- 7 页完整版,含接头设计尺寸图解
- 医用常用料与灭菌方式的选材提示
- 切割封边:一道工序完成裁切与锁边
PDF · 0.6 MB · 7P
Send us your part
Tell us the material, dimensions and cycle time. We reply with joint design, machine and fixture suggestions.
Direct contact