
Snap Fits Plus Welding: Which One Carries the Load
"Snap it together first, then weld a joint round it — belt and braces." The idea sounds safe and in practice often leaves neither doing its job.
The two fight each other
Snaps that close first hold the weld faces apart. A snap fit locks the halves at a fixed relative position. If that position sits a fraction above what welding needs, a gap remains between the weld faces, and no amount of energy will close it.
Welding needs travel, and the snaps prevent it. Ultrasonic welding involves real displacement: the director melts, the halves approach, and melt fills the gap. That travel is typically a few tenths of a millimetre. With the snaps already locked, the travel cannot happen — energy goes in, nothing moves, and the interface overheats without fusing.
The reverse holds too. If welding does complete and the halves close by a few tenths, the snaps are pulled past their design position and the hooks are loaded, distorted or broken.
What to do
Option one: stop the snaps setting the height. Design them with clearance so that after engagement there is still play: they prevent separation without deciding the distance between the halves. Height location belongs to the weld faces.
Option two: snaps as pre-fixing only. They hold the halves loosely for handling onto the fixture, and welding provides the real seating and location. That requires a genuinely loose engagement.
Option three: choose one. Snaps where the joint must come apart, welding where it must seal or carry load. Asking for both usually gets neither.
When the combination does make sense
One case is legitimate: a long joint on a large part, with snaps used to pull the halves together before welding and take out warp. There the snaps are an assembly aid rather than the final connection, and should be designed as such — moderate engagement force, clearance in position, and all load carried by the weld afterwards.
Another is dividing duties: snaps on one side taking the operating force of opening and closing, the weld on another side providing the seal. They act in different places and directions and do not interfere.
How to tell
If a part already combines both, run a simple trial: cut the snaps off, weld the joint alone, and see whether quality improves noticeably. If it does, the snaps are interfering and the design needs changing rather than the parameters.
Check the other direction too: after welding, look at the hooks for whitening or distortion, which shows the weld collapse pulled them past position.
One more route
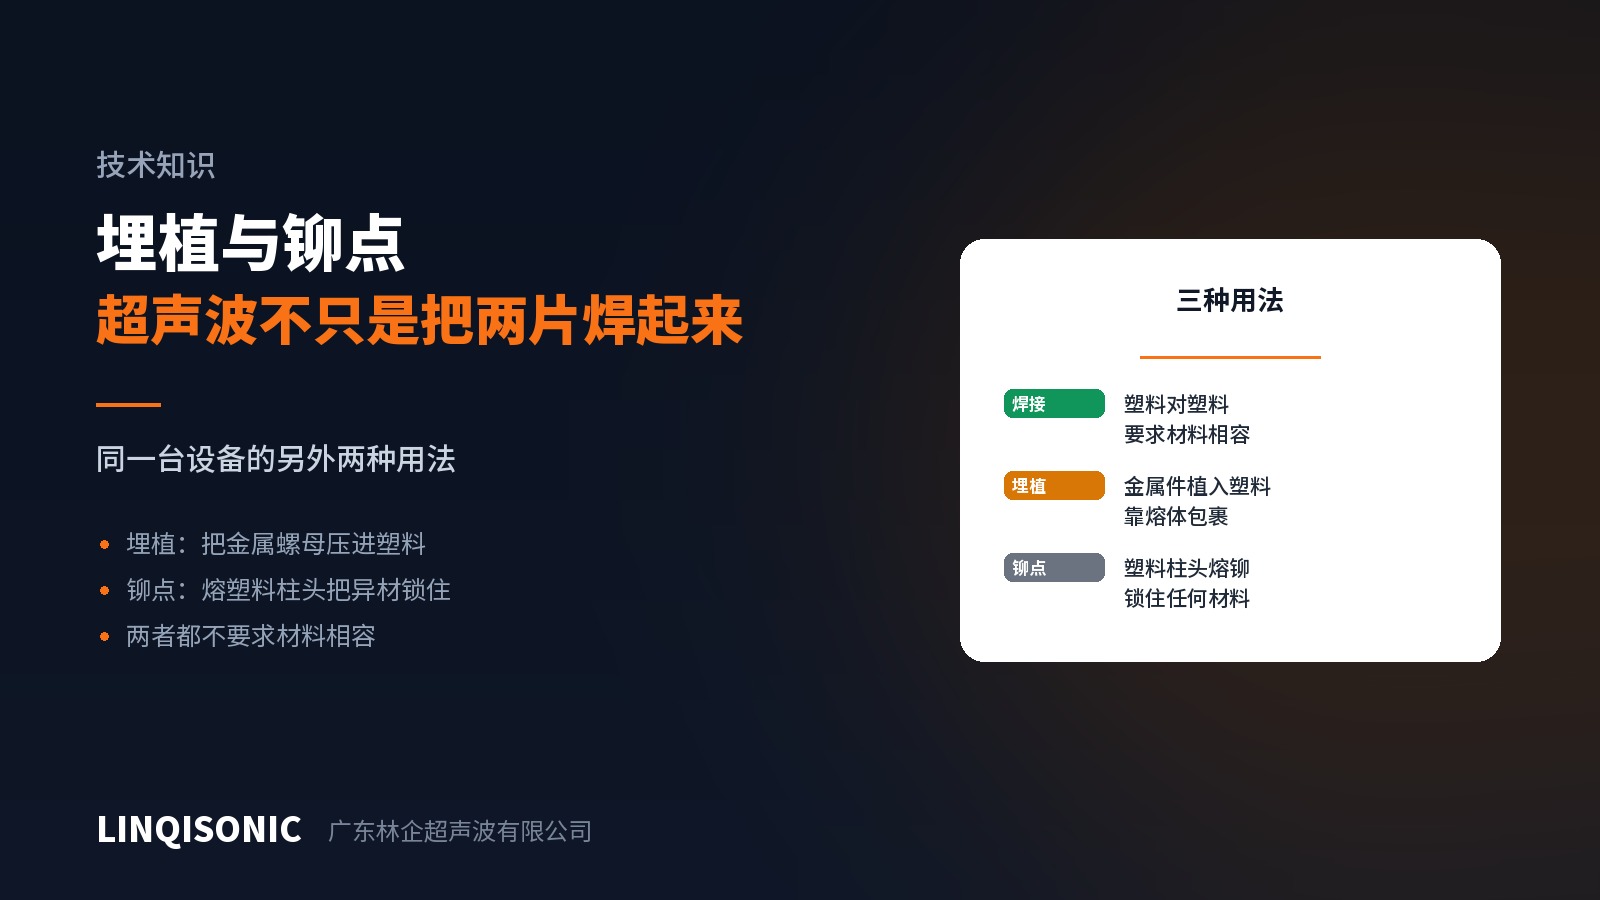
Where the materials are incompatible and cannot be welded but the joint must hold, use ultrasonic staking: a boss on one part passes through a hole in the other and the head is melted into a rivet that captures it. The captured part takes no part in fusion, so compatibility is not required. That is far cleaner than combining snaps with welding.
Joint design and staking head forms are in the handbooks on the downloads page. Depth modes and staking tooling are on the ultrasonic welding machine pages.
Send the assembly drawing to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.