
Shrinkage and Warp: Half the Result Is Decided Before Welding
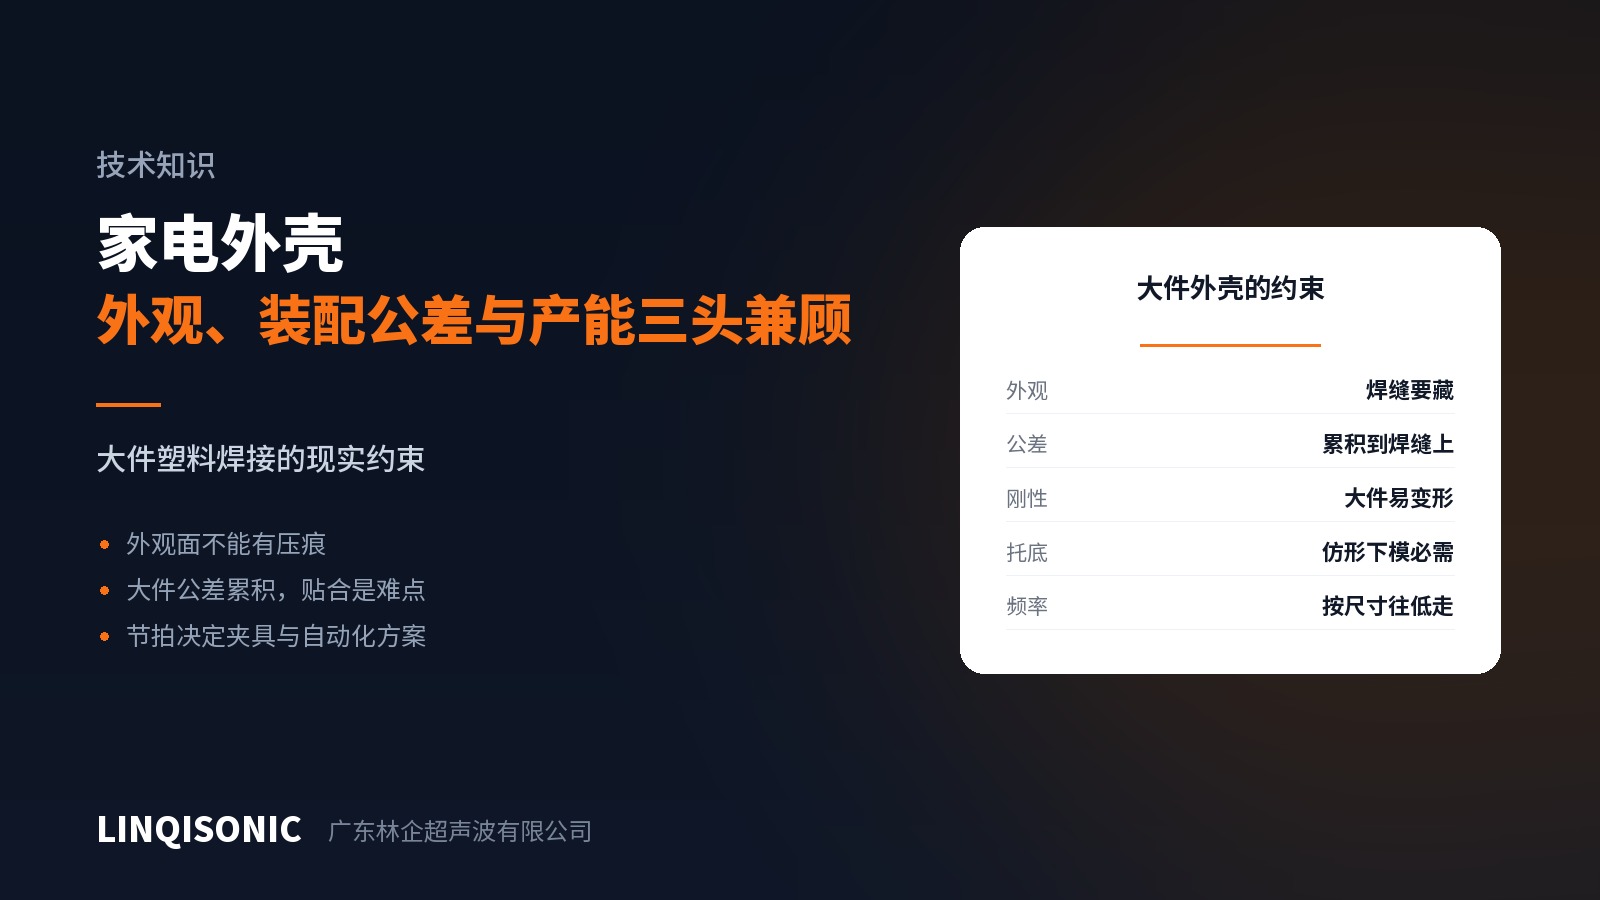
The larger the part, the greater the absolute magnitude of moulding shrinkage, warp and ejection distortion. When the halves come together, the gap cannot be identical all round the joint: some regions seat firmly and others still show a gap.
The result is one part with sections fused and sections cold. That is not a tuning failure; the geometry was already wrong before welding began.
Three responses, in order
One: a joint that absorbs tolerance. A shear joint relies on side-wall interference and is insensitive to height variation, far more forgiving than a butt joint. Prefer it on large parts.
Two: a mode that compensates. Time mode offers no compensation for a varying gap; relative depth starts from each part's actual contact point and energy mode watches the total input, and both are steadier.
Three: a fixture that brings the part to shape. Correcting a large part in the fixture before welding is far more effective than adjusting parameters afterwards.
But do not over-constrain
The third has a reverse side: a fixture clamped too hard locks residual stress into the part. The part is forced into shape, welded, released, and the stress remains, ready to crack under thermal cycling or chemical contact. PC is especially sensitive.
The distinction is that the fixture should support and guide, not straighten. The nest follows the part's natural shape, takes the weld force and holds the shape through the cycle, rather than pressing warped regions flat with a few clamps.
When to go back to moulding
There is a line: where moulded warp exceeds what welding can absorb, it is a moulding problem and welding will not recover it.
The test: rest the two halves together with no external force and measure the gap all round. If the largest gap approaches or exceeds the joint interference or the director height, no parameter will make that section good.
What to examine then is tool cooling, gate position, ejection and moulding parameters, not further trials at the welding station.
Two more points on large parts
A contoured nest is not cheap and cannot be skipped. Large parts deflect under weld force, side walls splay and bases sink, so seating at the joint differs entirely from the unloaded condition. The nest is a necessity, not an option.
Beyond a certain joint length, zone it. One horn cannot hold amplitude uniform along a long joint and the middle welds while the ends do not. Consider several horns driving separate zones.
Tolerance absorption by joint form and the dimensional system for eight joint types are on the downloads page. Relative depth mode, energy mode and large-part fixturing are on the ultrasonic welding machine pages.
Send drawings, materials and measured gap data to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.