
The Parting Line Decides Which Way the Flash Goes
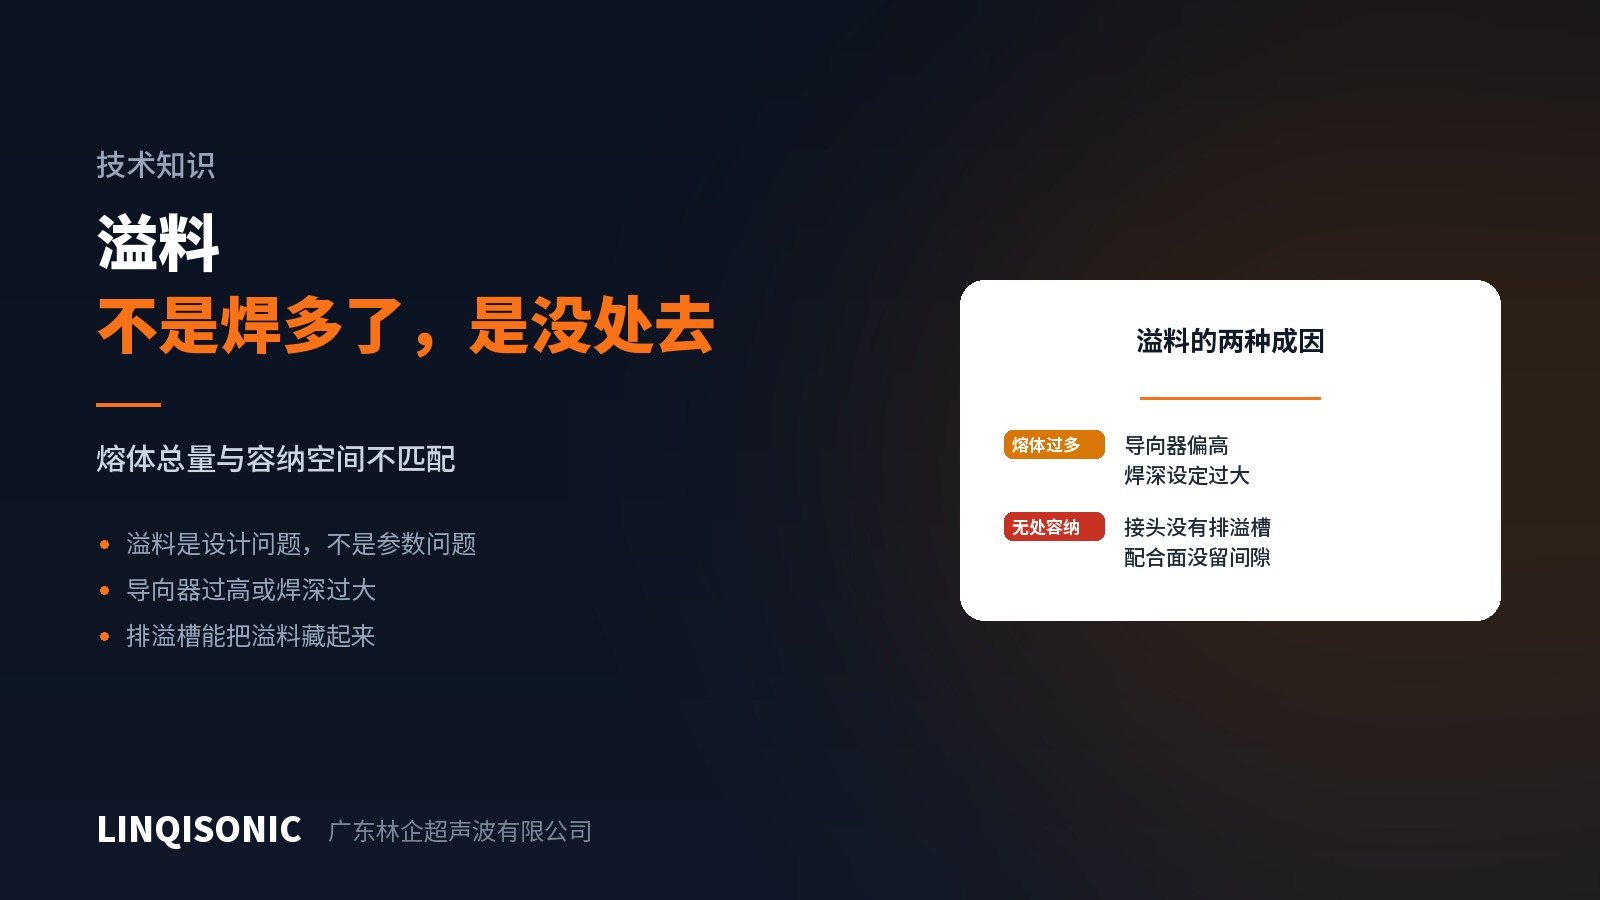
Flash has two questions: how much, and which way. The first is controlled by director height and energy; the second is decided entirely by geometry and parameters cannot move it.
Direction is designed in
Melt flows under pressure along the path of least resistance. If one side of the joint is a closed step and the other an open gap, it will take the open side.
So the question is not how to make flash disappear — melt is conserved and it does not disappear — but how to send it somewhere it cannot be seen.
Three common approaches
A flash trap. A groove inside the joint to receive the surplus melt, sized from the director volume rather than drawn by eye. The most direct and effective measure.
A step joint. A step outside the joint line keeps the flash behind it, and the step also helps location: the halves align before they close.
A shear joint. Melt stays contained between the mating faces, so visible flash is naturally less than with an energy director. Worth preferring on cosmetic parts, provided the side walls can take the lateral force from the interference.
Where to put the parting line
The parting line sets the visible division between the halves and which side the flash appears on. Place it at a change in the form — an edge, a styling break, a decorative groove — where flash is least conspicuous.
Put it across the middle of a large face and flash lands in the most visible place, and no amount of parameter work will make it acceptable.
Two things easily missed
Flash at corners looks worse. Melt flows poorly there and accumulates into a local ridge. Traps at corners can be deeper and wider.
Direction affects function, not only appearance. Flash entering a sealing face forces the fit open; flash falling into a fluid path on medical or fluidic parts is a particle risk; flash in the light path of an optical part affects transmission. In those cases flash direction is a functional question.
If the tool is already cut
Direction cannot change, so reduce the quantity: lower the weld force, which is what drives melt out, taking the low end of the range that still ensures seating; switch to energy or depth mode to cap the total input; and check that horn and part are parallel, since misalignment concentrates flash on one side.
A quick diagnostic: even flash all round is a melt volume question, so check director height and energy; flash on one side is parallelism or fixture; intermittent flash is incoming variation.
Flash trap dimensions, step joints and the full dimensional system for eight joint types are in the joint design guide on the downloads page. Force control and mode selection are on the ultrasonic welding machine pages.
Send drawings and appearance requirements to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.