
Why a Horn Has to Be Designed for the Job
"Can we modify an existing horn to suit?" The answer is usually no, and the reasons are worth setting out.
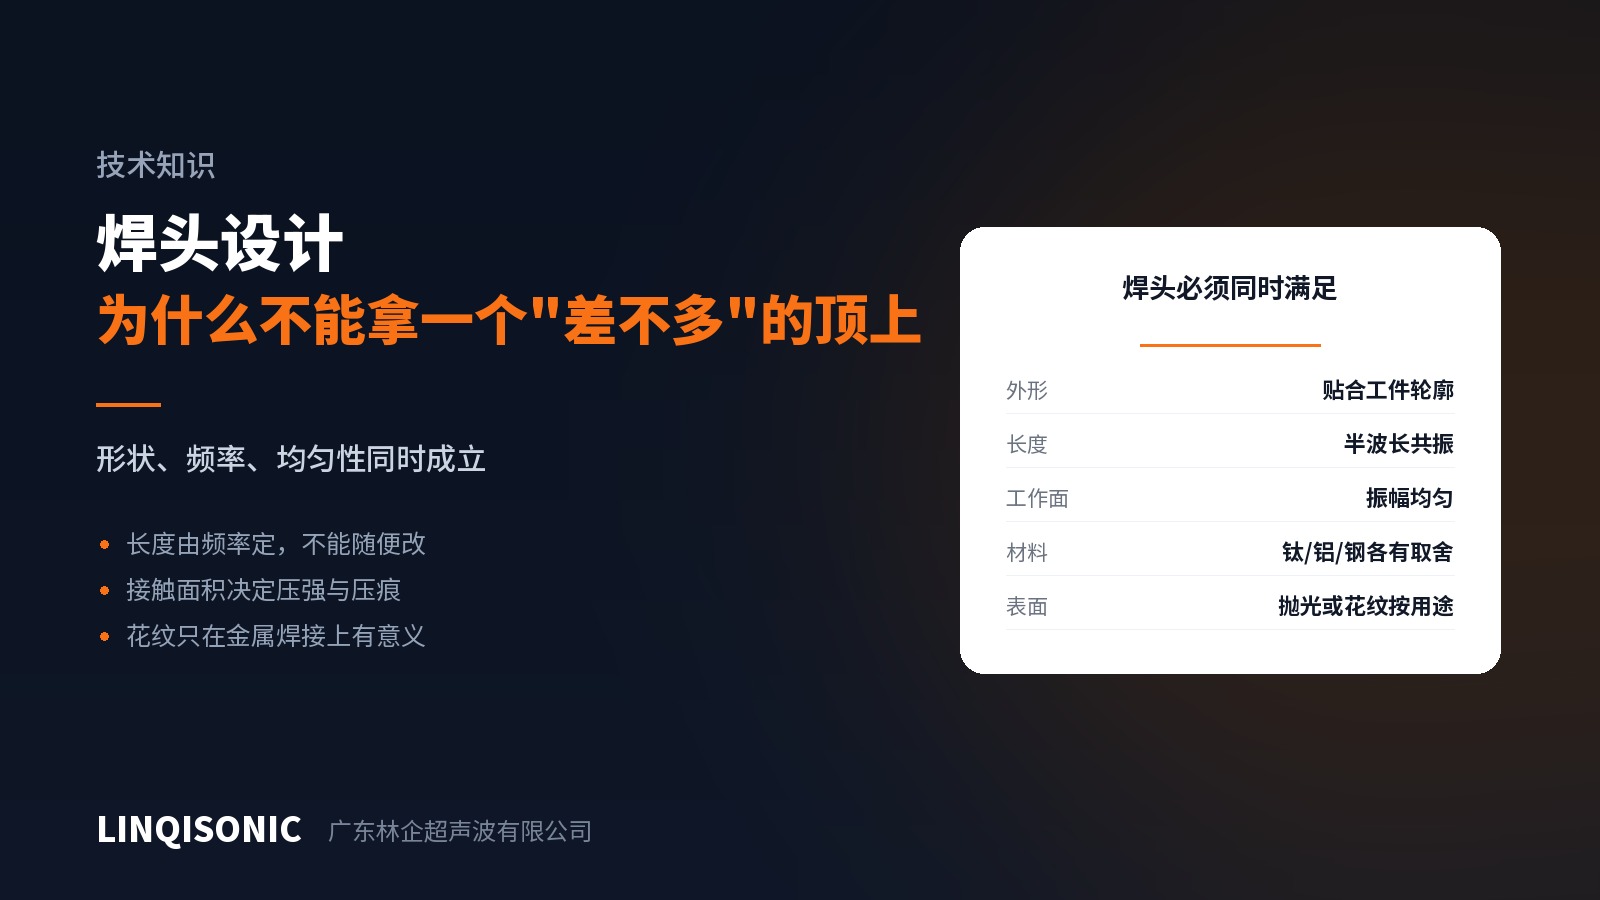
Three conditions at once
The shape must match the part. The working face has to conform to the contact surface, or pressure distributes unevenly and one side crushes while another fails to fuse.
Length is set by frequency. A horn stands in a half-wavelength relationship; change the length and the resonant frequency moves with it. Trimming a few millimetres to suit part height is not an option.
Amplitude must be uniform across the face. The more complex the shape and the larger the size, the harder this becomes — and it is often the real limit on how large a horn can be.
These constrain one another. Changing the shape affects frequency, changing length affects resonance, increasing size affects uniformity. A horn is calculated, not traced from the part.
Material trade-offs
Titanium — the best acoustic performance, low loss and high strength, suiting high amplitude and continuous duty, and the usual choice for large horns. Machining difficulty and cost are the drawbacks.
Aluminium — good acoustics, easy machining and low cost make it the most common horn material. Wear resistance is poor, the face wears readily, and life is short against abrasive filled materials. Surface hardening improves this.
Steel — wear resistant, but acoustically lossy and noticeably hot in service, so normally reserved for wear-critical areas or particular applications.
Surface treatment
Polishing. For plastic welding, and especially clear or cosmetic parts, the face must be polished; any texture transfers one-to-one onto the part.
Knurling. Metal welding horns carry knurled or toothed faces to grip the workpiece and transmit shear motion. Plastic welding needs no pattern, and adding one only leaves marks.
Hardening. Aluminium horns wear quickly against glass-filled materials, and surface hardening extends life considerably.
Common modification mistakes
Shortening to suit the part — frequency drifts and the stack cannot resonate.
Drilling clearance holes in the face — the amplitude distribution is disturbed and the hole surroundings become stress concentrations.
Using one flat horn across several scattered weld points — the central contacts see quite different pressure from those at the edge.
Grinding the face smaller to raise amplitude — gain changes, but so do frequency and uniformity. Change gain by changing the booster.
What a design needs
To produce a horn, the minimum required is the part drawing showing joint position and contact contour, the resin grade, the frequency, and the required cycle rate. Note any appearance requirements or clearance features as well.
Maximum horn sizes and available frequencies by machine are on the ultrasonic welding machine pages. Send drawings for horn design or modification to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.