
Joining Copper to Aluminium: What Fusion Welding Cannot Do
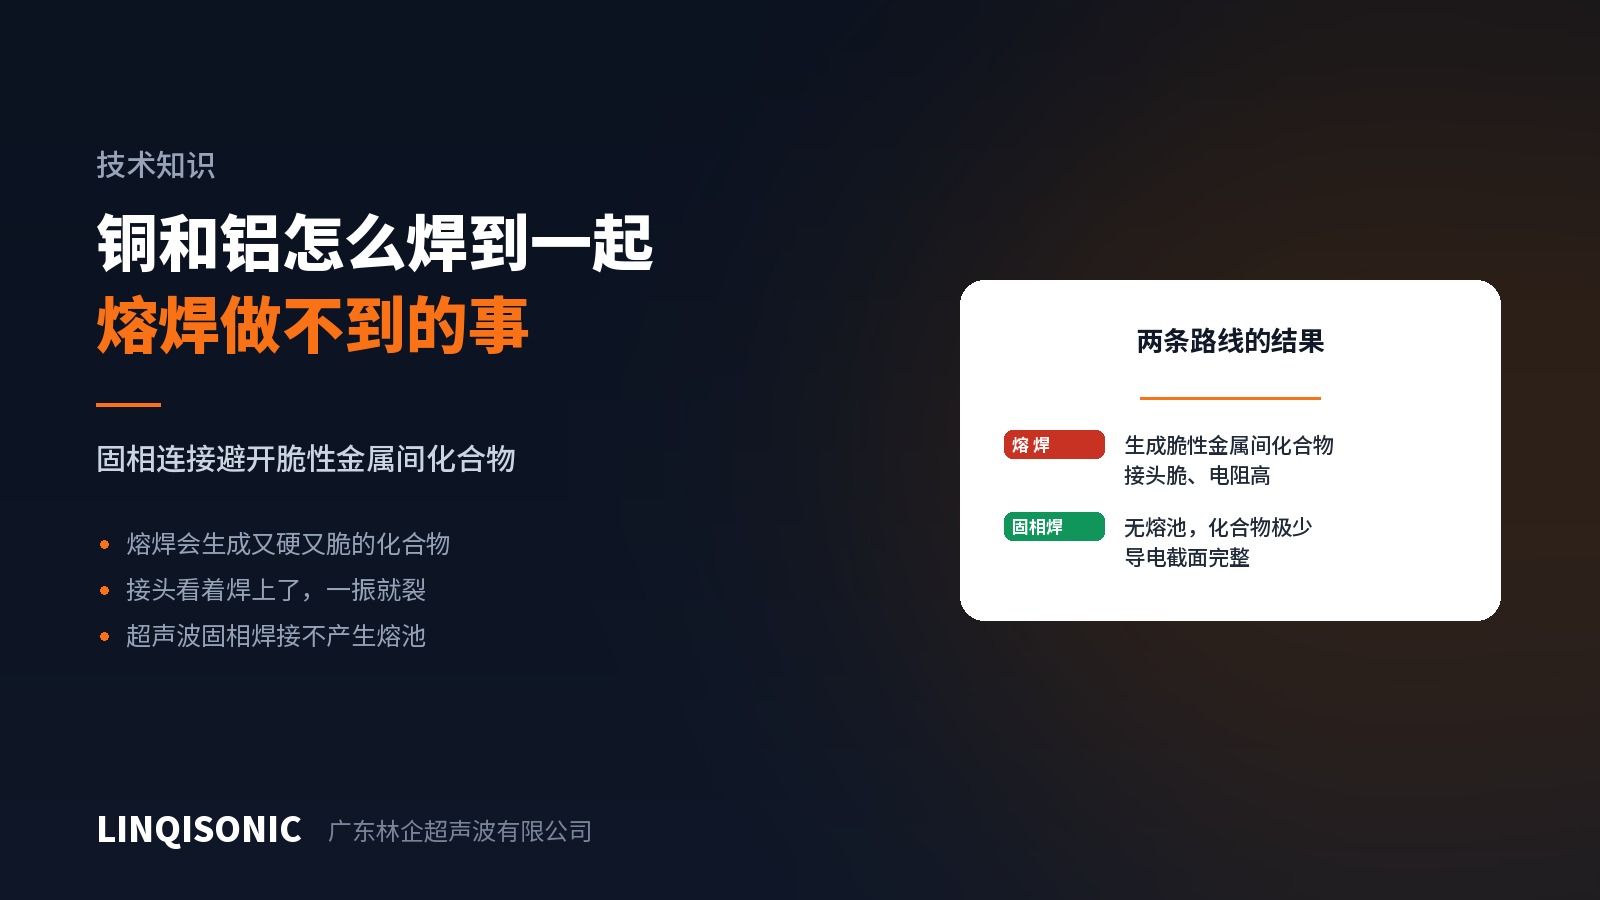
Joining copper to aluminium is unavoidable in battery packs, automotive harnesses and power connections — and doing it by fusion welding is metallurgically disadvantaged from the outset.
Why fusion welding struggles
Copper and aluminium dissolve into one another in the liquid state, and on cooling precipitate a family of intermetallic compounds. They share two characteristics: they are hard and brittle, and they conduct far worse than either parent metal.
The result is a joint that looks sound but is mechanically brittle and electrically poor. In service, vibration and thermal cycling initiate cracks in the intermetallic layer, joint resistance rises, and the resulting heat accelerates ageing — a self-reinforcing loop.
Worse, this layer forms whenever there is a melt pool. Parameter control can make it thinner; it cannot remove it.
Solid-state joining sidesteps the problem
Ultrasonic metal welding produces no melt pool. High-frequency vibration disperses the oxide on both surfaces so clean copper meets clean aluminium under force and forms metallic bonds, with temperature staying well below melting throughout.
No liquid phase means no wholesale interdiffusion, intermetallic formation stays within a very thin range, and both the mechanical and electrical properties of the joint survive.
This is not a win from parameter optimisation. It is a different process route.
Points to watch
1. Surface condition matters more than expected. Aluminium oxidises very quickly and its oxide is denser and harder than copper's. Ultrasonic vibration exists to break that film, but heavy oxide, oil or anodising on incoming material raises the energy needed and degrades consistency. Incoming surface condition belongs in receiving inspection.
2. Which metal goes on top changes the result. Aluminium is softer and deforms more under force and vibration. Knurl pattern, force distribution and stack order all affect how energy divides between the two sides; establish this during trials rather than by assumption.
3. Weld area governs current capacity. For an electrical joint, the current it will carry depends on the area actually bonded, not on how large the weld looks. Insufficient area means local heating at rated current.
4. Tooling is consumable. Breaking the oxide depends on the knurl gripping the workpiece. Once the knurl wears flat, energy no longer transfers and quality falls across the board. The decline is gradual and easily mistaken for machine ageing when replacing the tooling would restore it.
Typical applications
Aluminium tabs to copper interconnects in traction batteries, copper-to-aluminium busbar transitions, and copper wire to aluminium terminals as an alternative to crimping.
Our ultrasonic metal welding equipment covers 20, 30, 35 and 40 kHz; see the ultrasonic welding machine pages for models.
Send material grades, thicknesses and joint configuration to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.