
Welding Thin-Walled Parts: Punch-Through, Distortion and Resonance
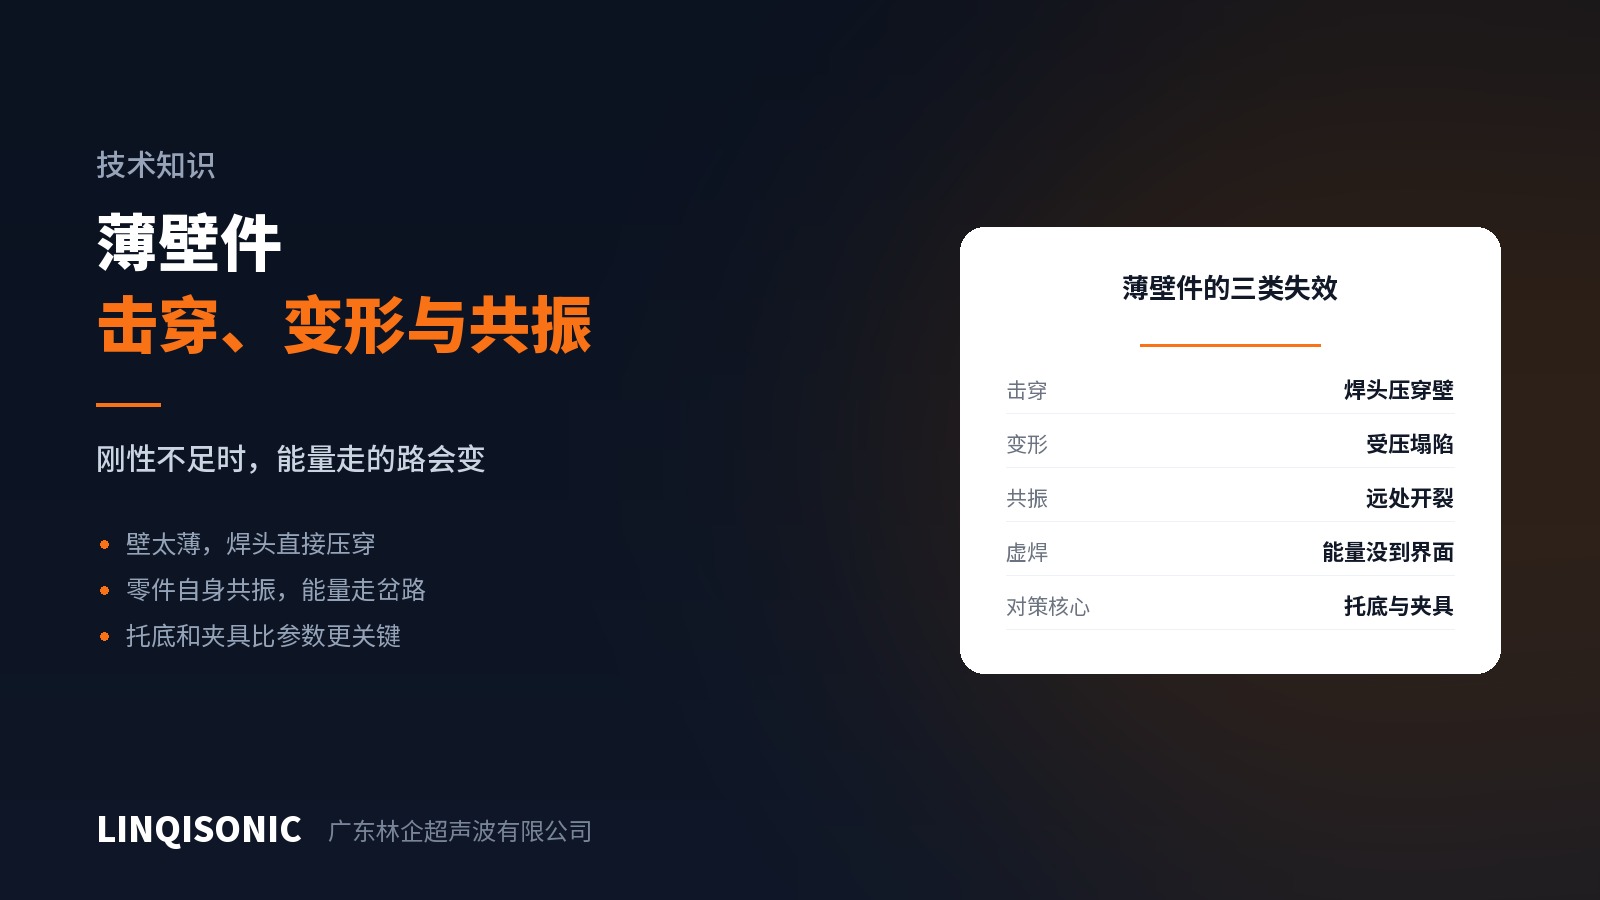
With thin-walled parts, the problem is often not at the joint but somewhere else entirely.
Three typical failures
1. Punch-through. The horn bears on a thin wall that cannot take the force and vibration, and pushes through or dents it. The most direct failure.
2. Collapse and distortion. The part sinks or the side walls splay under weld force, so seating varies around the joint and one side fuses while another does not.
3. Cracking far from the joint. The most puzzling case: the weld is sound, but something cracks well away from it. The cause is a feature of the part resonating near the ultrasonic frequency, amplifying local motion and concentrating stress there.
Why thin walls are difficult
Energy transfer in ultrasonic welding depends on part stiffness. With adequate stiffness, vibration travels the intended path to the joint. Without it, energy goes where it more easily can — into making the thin wall vibrate, or deflecting the part — rather than to the interface.
The consequence is twofold: too little energy at the joint, too much everywhere else.
Order of remedies
1. Support from below. The nest must follow the part contour as closely as possible and take the weld force. Inadequate support is the leading cause of thin-wall problems, and a properly contoured nest usually beats any parameter change.
2. Restrain whatever resonates. Where remote cracking occurs, find the feature and add a support point in the fixture. Resonance needs freedom to move; restrain it and it stops.
3. Increase horn contact area. At the same force, doubling the area halves the pressure, improving both punch-through and marking.
4. Reduce force and approach speed. Impact at contact is a major contributor to punch-through, and decelerating before contact helps noticeably.
5. Consider a higher frequency. Higher frequency means lower amplitude for the same energy and a gentler mechanical impact on thin walls. The trade-off is less available power and a smaller weld area — which small thin parts do not need anyway.
Only then, energy and time.
What design can do
Many thin-wall problems can be avoided on the drawing:
place a supporting structure or rib beneath the horn contact area rather than on unsupported wall;
thicken the wall locally near the joint to give energy a stable path;
shorten or rib any cantilever or flange likely to resonate.
Frequency options and amplitude ranges by machine are on the ultrasonic welding machine pages. Send part drawings and wall thickness distribution to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.