
Controlling Flash in Ultrasonic Welding
A ring of plastic squeezed out around the joint: it spoils appearance, interferes with assembly, and sometimes has to be trimmed by hand. One of the most common complaints in ultrasonic welding.
The answer usually does not lie in the parameters.
Where flash comes from
The logic is plain: more melt is produced than the joint can contain, and the surplus has to go somewhere.
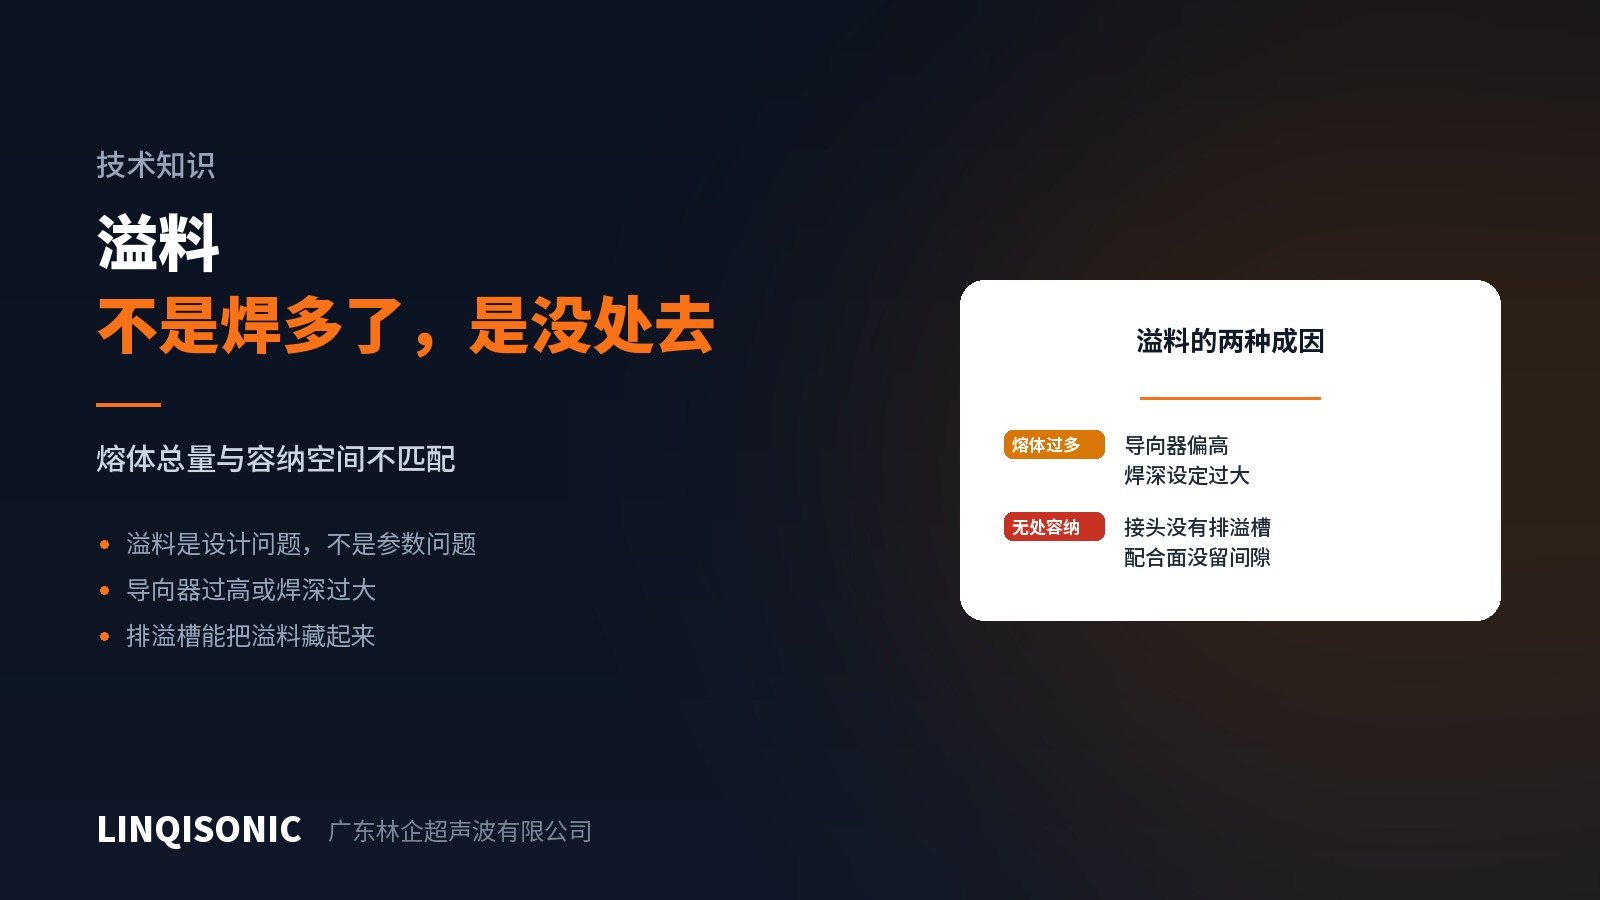
So there are only two directions: too much melt, or nowhere to put it.
Direction one: too much melt
The energy director is too tall. Director height sets the volume available to melt, and should be matched to wall thickness. A wall thickness change without a corresponding director change is the most common cause.
Weld depth set too deep. In depth mode, if the commanded travel exceeds what the director can supply, the machine keeps pressing and melts base material on both sides, so melt volume inevitably exceeds the gap.
Energy or time set too high. The only genuinely parametric cause — and often itself a compensation for one of the two above.
Direction two: nowhere to put it
A design issue, and the easiest to resolve.
Add a flash trap. A groove alongside the joint lets surplus melt flow inward rather than outward. The flash still exists but is hidden where it cannot be seen after assembly. The most direct and effective fix.
Use a shear joint. Melt is contained between the mating faces, so a shear joint naturally produces less visible flash than an energy director — worth weighing when appearance matters.
Add a step. A step outside the joint line both conceals flash and helps location.
What parameters can still do
Where the design is fixed, some margin remains:
Reduce force. Force is what drives melt out of the joint; take the lower end of the range that still ensures seating.
Switch to energy or depth mode. Time mode compensates for nothing, so slightly more material means more flash. Energy mode caps the total input.
Check horn-to-part contact. If the working face is not parallel to the part, force concentrates on one side and flash gathers there. One-sided flash is a clear signal.
A diagnostic
Look at whether flash is even all round or concentrated on one side.
Even all round → a melt volume issue; check director height and energy setting.
One side → parallelism or fixture; check horn contact and part location.
Intermittent → incoming variation; check wall thickness and height tolerance.
Mode selection and force control differ by machine; whether energy and distance modes are available is listed on the ultrasonic welding machine pages.
Flash trap dimensions, director height against wall thickness and the full dimensional system for eight joint types are in the Energy Director & Joint Design Guide on the downloads page.
Send part drawings and photographs to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.