
Why Ultrasonic Horns Wear, and When to Replace Them
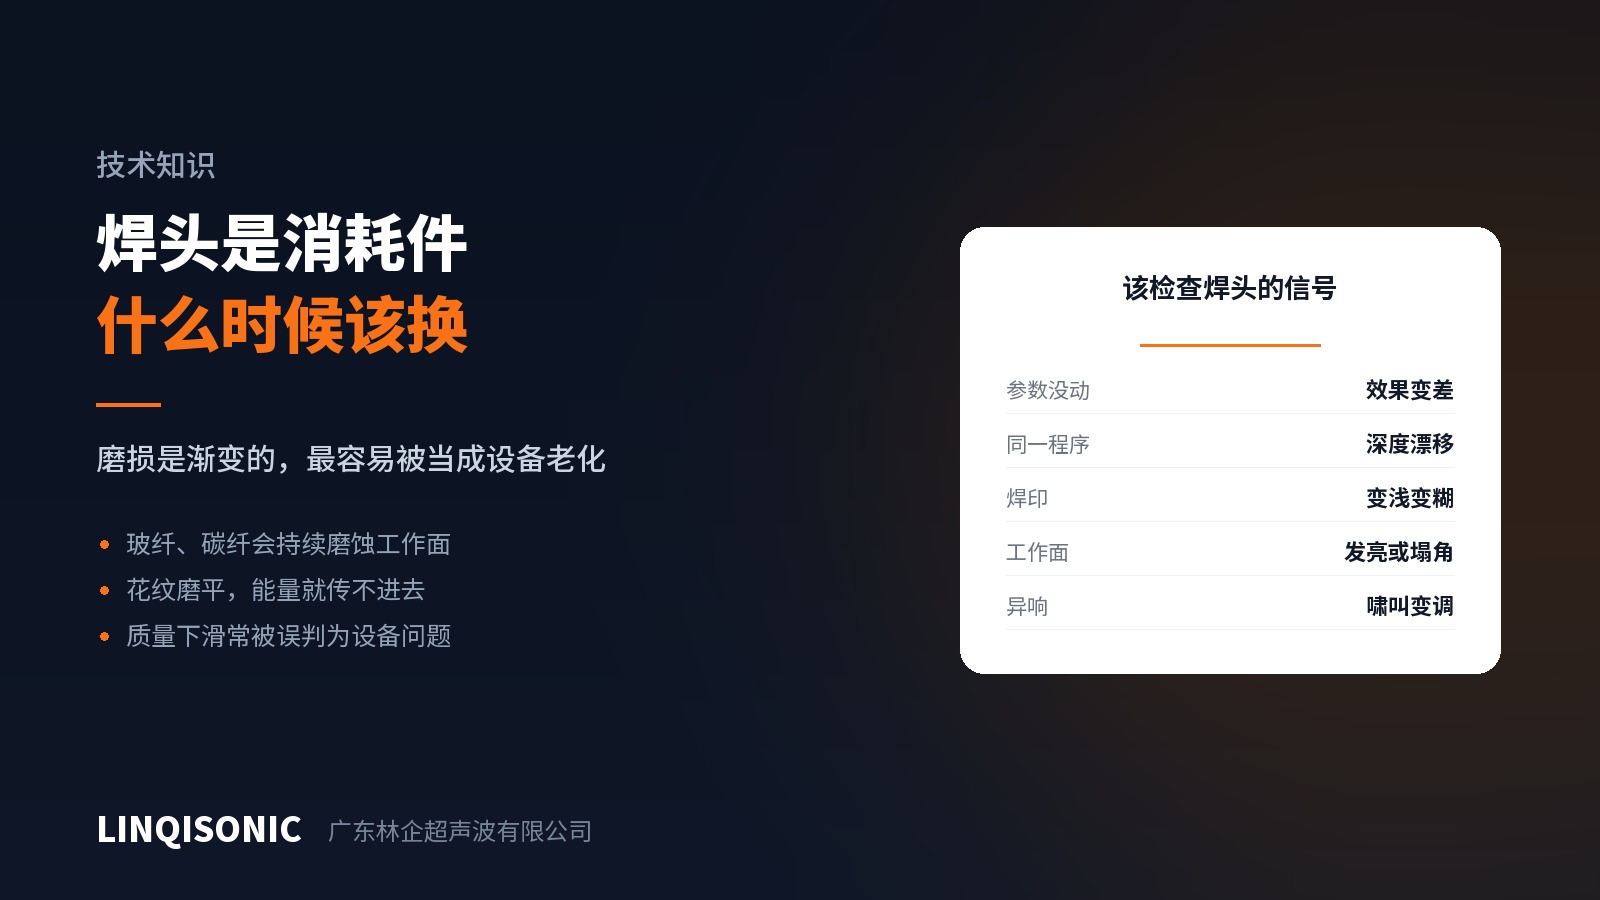
"The machine is two years old and does not seem as good as it was." That is among the most common service descriptions we receive — and a large share of the time the real answer is that the horn needs replacing.
Horns are consumables
The horn contacts the workpiece directly and takes high-frequency vibration and force on every cycle. Wear on the working face is inevitable; only the rate differs.
Glass- and carbon-filled resins — fibre is far harder than resin and abrades the face like fine abrasive paper. The higher the loading, the faster the wear, and carbon is more aggressive than glass.
Metal welding tooling — depends on a knurl gripping the workpiece to transmit vibration, and the knurl is the first thing to flatten.
Unfilled plastics — much slower, but not zero, particularly with fillers or coated surfaces.
Why it gets misdiagnosed
Wear is gradual. Nothing fails on a particular day; yield drifts down a little at a time, parameters creep up a little at a time, and occasional rejects slowly become normal.
Through that process operators suspect material batches first, then tooling, then machine ageing. The horn — which still "looks fine" — tends to be considered last.
Signals worth watching
Same parameters, worse results. Same program, same material, and strength or seal integrity is no longer what it was. The most direct signal there is.
Post-weld depth drifting. Welding in depth mode, the post-weld height gradually departs from where it used to sit. A little material off the face changes the geometry.
Weld impression fading or blurring. In metal welding, watch the knurl impression on the part; when it becomes shallow or its edges smear, the knurl has flattened.
A polished or rounded working face. A sound face keeps its original texture and edges. Local shine indicates concentrated wear; rounded edges change both contact area and pressure distribution.
A change in the sound. A horn is an acoustic component designed to a resonant frequency, and losing material shifts its mass distribution and resonance. Experienced operators hear it.
How to manage it
Put horns in the spares plan. In volume production of filled or metal parts, the horn is a planned consumable with a replacement interval — not something to buy after it fails.
Inspect on a schedule, not only when there is trouble. Check the working face by shift or by output, and photograph it. The trend is far more informative than a single judgement.
Do not dress the face yourself. Horn length is set by resonant frequency; unplanned grinding shifts the resonance, costing efficiency at best and causing generator alarms or horn cracking at worst. Repairs belong with someone who can re-verify the frequency.
Look after spares too. A horn stored badly — knocked, or corroded by damp — will misbehave as soon as it is fitted.
Material selection, the relation between gain and profile, and amplitude uniformity across large horns are covered in the Horn Selection & Design Guide on the downloads page. Equipment is on the ultrasonic welding machine pages.
If you are unsure about a horn, photograph the working face and send it to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.