
Welding Appliance Housings: Three Requirements at Once
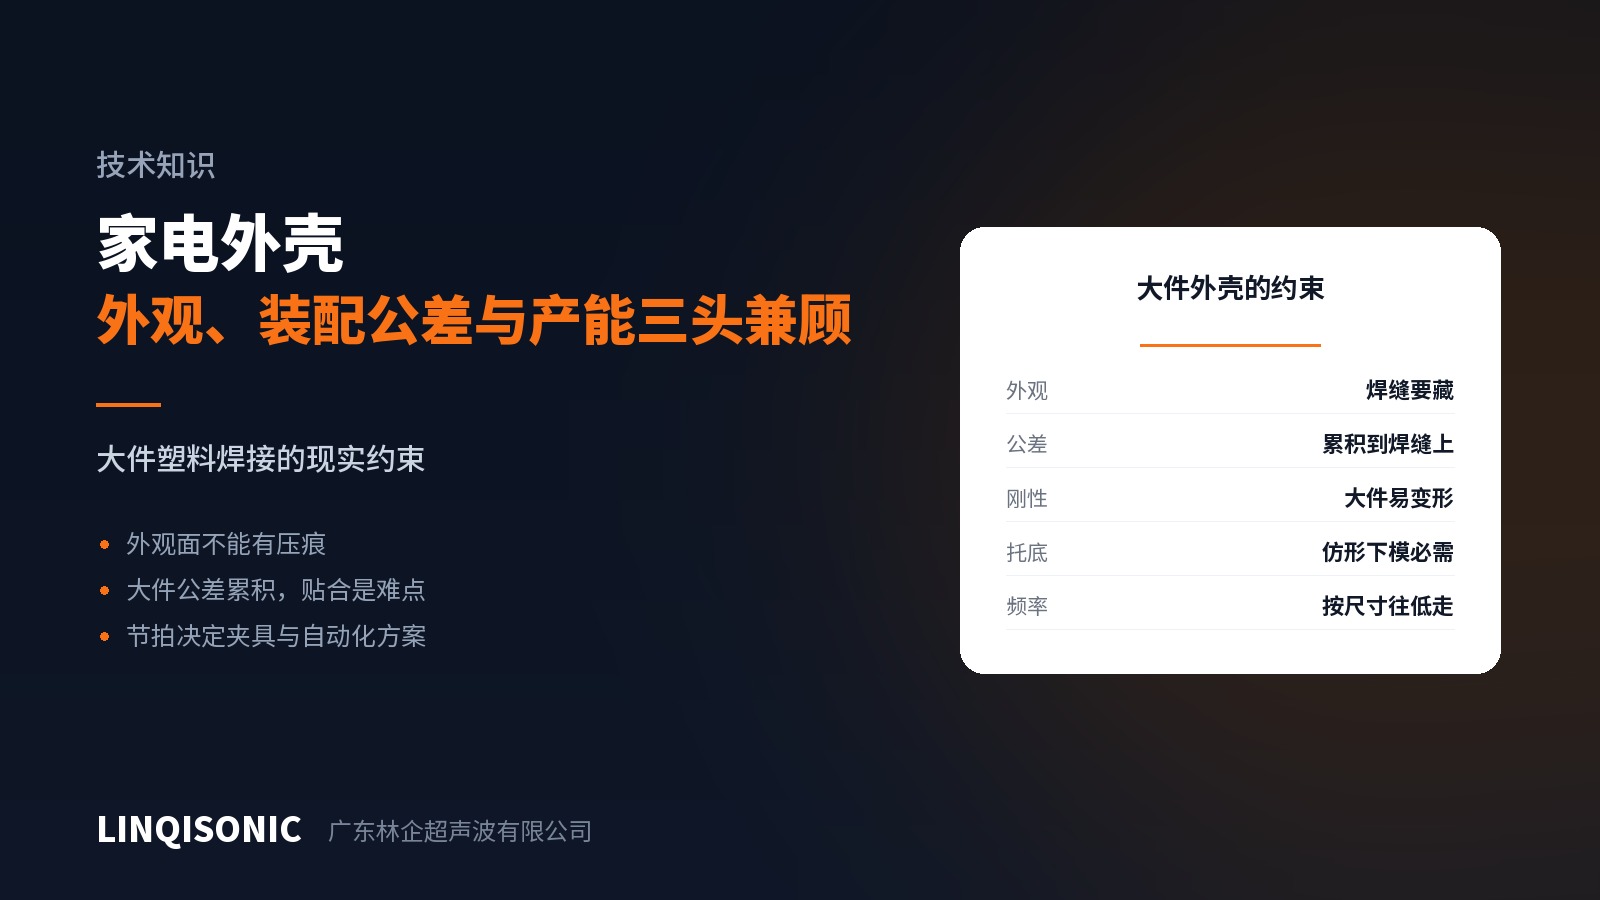
Vacuum cleaner bodies, air purifier housings, small appliance panels, fan covers — all share a profile: large, appearance-critical and produced in volume. The three requirements pull against each other.
Constraint 1: no marks on visible faces
The outer surface of an appliance housing is what the customer sees, and a horn impression there shows in raked light however light it is.
In order of preference:
Put the horn contact on a non-visible face. Most housings can take force from inside or underneath, the cleanest answer provided it is planned on the drawing.
Where the visible face is unavoidable — enlarge the contact area to spread pressure, polish the horn face, and reduce force and approach speed.
Consider far-field welding. The horn contacts somewhere inconspicuous and energy travels through the part to the joint. Large housings are usually amorphous ABS or PC/ABS, which transmit better than semi-crystalline resins, so this is workable.
Constraint 2: tolerance accumulates at the joint
The larger the part, the greater the absolute magnitude of moulding shrinkage, warp and ejection distortion. When the halves come together, the gap cannot be identical all around the joint — some regions seat firmly and others still show a gap.
The result is one part with sections fused and sections cold.
Remedies:
Design a joint that absorbs tolerance. A shear joint relies on side wall interference and is insensitive to height variation, far more forgiving than a butt joint.
Use distance or energy mode. Time mode offers no compensation for varying gaps.
Let the fixture bring the part to shape. Correcting a large part in the fixture before welding beats adjusting parameters afterwards — but avoid over-constraint, since a fixture clamped too hard locks in residual stress, a particular risk with PC.
Control incoming parts. Where moulded warp exceeds what welding can absorb, that is a moulding problem and welding will not recover it.
Constraint 3: large parts need support and stiffness
Large parts deflect under weld force, with side walls splaying and bases sinking, so seating at the joint differs entirely from the unloaded condition.
A contoured nest is mandatory, not optional. It must follow the part closely, take the force, and hold the shape through the cycle.
Nests for large housings are rarely cheap, but saving that cost usually buys a long-running yield problem.
Frequency and equipment
Large plastic parts move down in frequency: larger horns, more available power, longer energy transmission. 15 kHz exists for exactly this work, while moderate weld areas suit 20 kHz.
Where the joint perimeter is long, one horn cannot hold amplitude uniform and multiple horns in zones should be considered.
Output and automation
As volume rises, cycle time becomes the binding constraint — and not only weld time, but loading, locating and inspection as well.
Parameter memory — where one machine runs several models, recalling settings on changeover is more reliable than a transcribed parameter sheet.
Process monitoring — hidden cold welds in large parts are hard to catch by manual sampling, and per-part monitoring is the practical answer.
Quick-change fixturing — changeover time often exceeds weld time by a wide margin.
Materials
Appliance housings commonly use ABS, PC/ABS, PP and HIPS. ABS and PMMA are fully compatible, making a clear panel on an ABS body a common pairing. PP and ABS are incompatible, and where a design pairs them, staking or mechanical fastening is the only route.
The compatibility reference is in the handbooks on the downloads page. Frequencies, maximum horn sizes and monitoring for large-part machines are on the ultrasonic welding machine pages. Send drawings, materials and cycle requirements to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.