
Why a Wide Horn Welds in the Middle but Not at the Edges
A common complaint on large parts: the middle welds beautifully while both ends either fail to fuse or flash badly. Changing parameters does not help, because this is not a parameter problem.
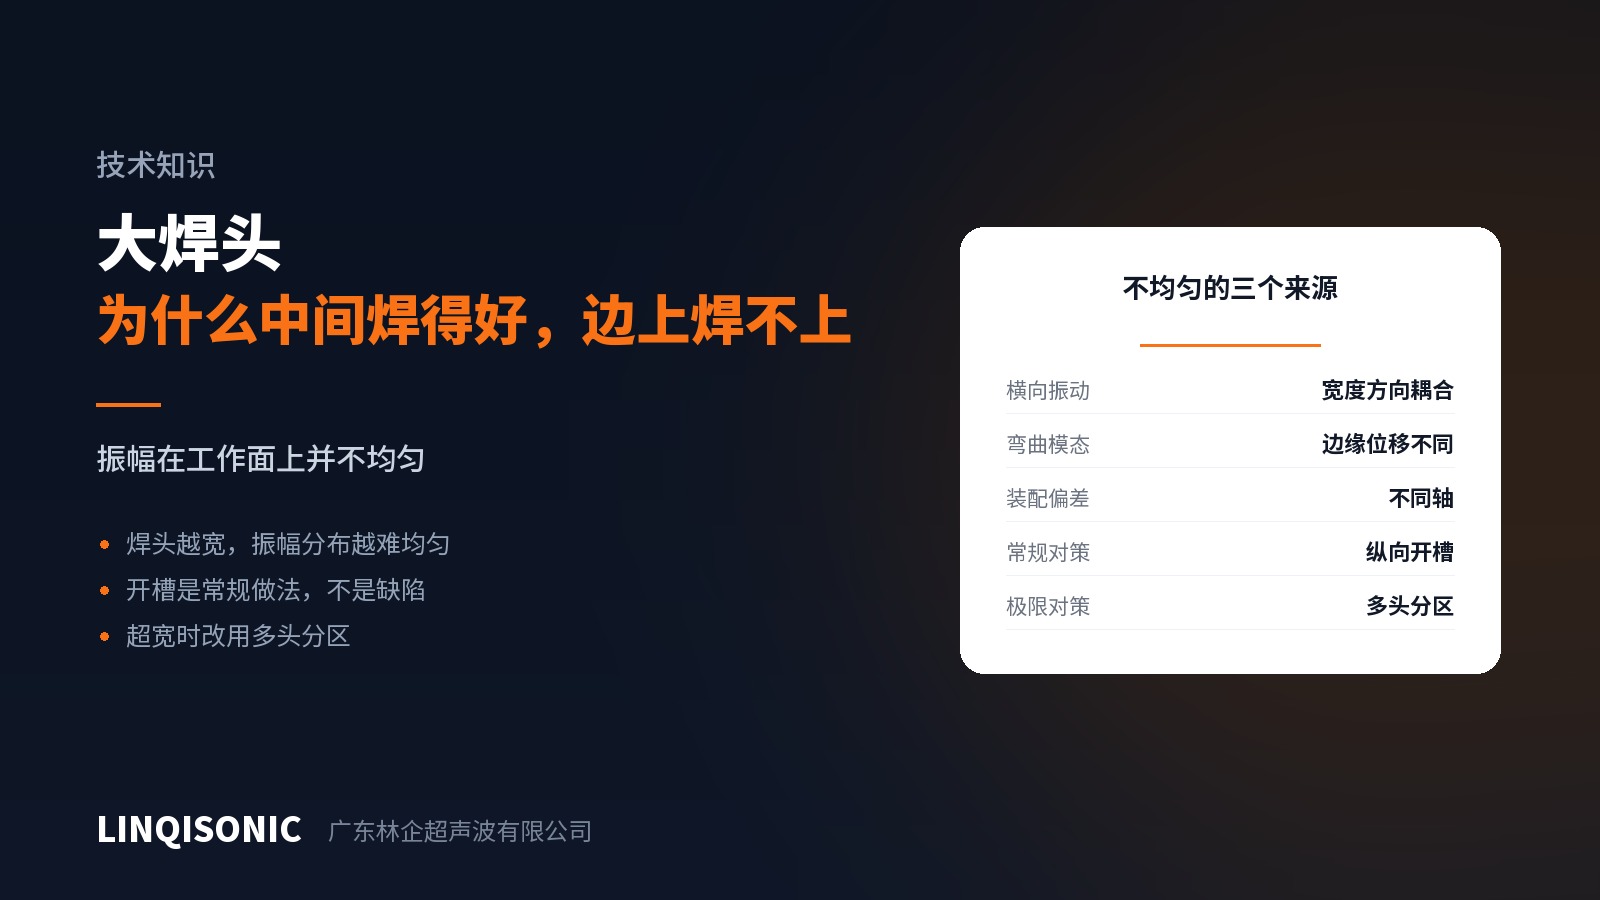
Amplitude is not uniform across the face
Ideally every point on the working face moves by the same amount. In practice, the wider the horn, the harder that becomes.
Lateral motion. As the horn extends and contracts axially, the Poisson effect makes it contract and expand laterally too. The wider the horn, the more significant this component, and it couples with the axial motion and disturbs the amplitude distribution.
Flexural modes. Wide, thin horns readily develop bending vibration, and the face flexes like a drumhead with quite different displacement at centre and edge.
Assembly error. A misaligned stack, unclean mating faces or incorrect tightening torque all leave one side with lower amplitude.
Slots are standard practice
Large horns often carry several axial slots. They are not cooling holes or weight reduction — their purpose is to acoustically divide a wide horn into several narrow ones, suppressing lateral coupling and flexural modes so each segment vibrates axially on its own.
Slots on a large horn indicate sound design, not a machining defect.
Beyond a certain width, split into zones
Slotting has its limits. Where the weld width exceeds what one horn can keep uniform, the correct answer is multiple horns driving separate zones, each with its own converter and its own section of the joint.
Every horn then works within its comfortable range and uniformity is assured, at the cost of machine complexity.
Rule out the simple causes first
Before suspecting the horn, confirm the following:
Is support from below uniform? A part supported on one side and unsupported on the other behaves very much like uneven amplitude, from an entirely different and more common cause.
Is the horn parallel to the part? Press impression paper or a soft material after assembly and check that the mark is even.
Are mating faces clean and torque correct? The converter-to-booster and booster-to-horn faces must be clean and flat, tightened to the specified torque; insufficient torque loses energy in transmission.
Is part height consistent? With loose incoming tolerances, tall parts contact first and short ones not at all, which also looks like edges failing to weld.
How to measure it
The most direct method: place thermal paper or a thin weldable film under the working face and run a weld into air, then read the depth distribution of the mark. Deeper means higher amplitude, lighter means lower, and the distribution is visible at a glance. Simple and reliable, and worth doing when changing horns and during routine maintenance.
Large horn design and maximum usable area are covered on the ultrasonic welding machine pages. Send drawings and joint layout to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.