
Can a Wall of a Few Tenths Still Be Welded
Director height is one-eighth of the wall thickness. At 0.6mm that is 0.075mm — a dimension the tool cannot hold, producing either a short shot or a rounded tip, so the drawing value does not exist in production.
Three problems at once
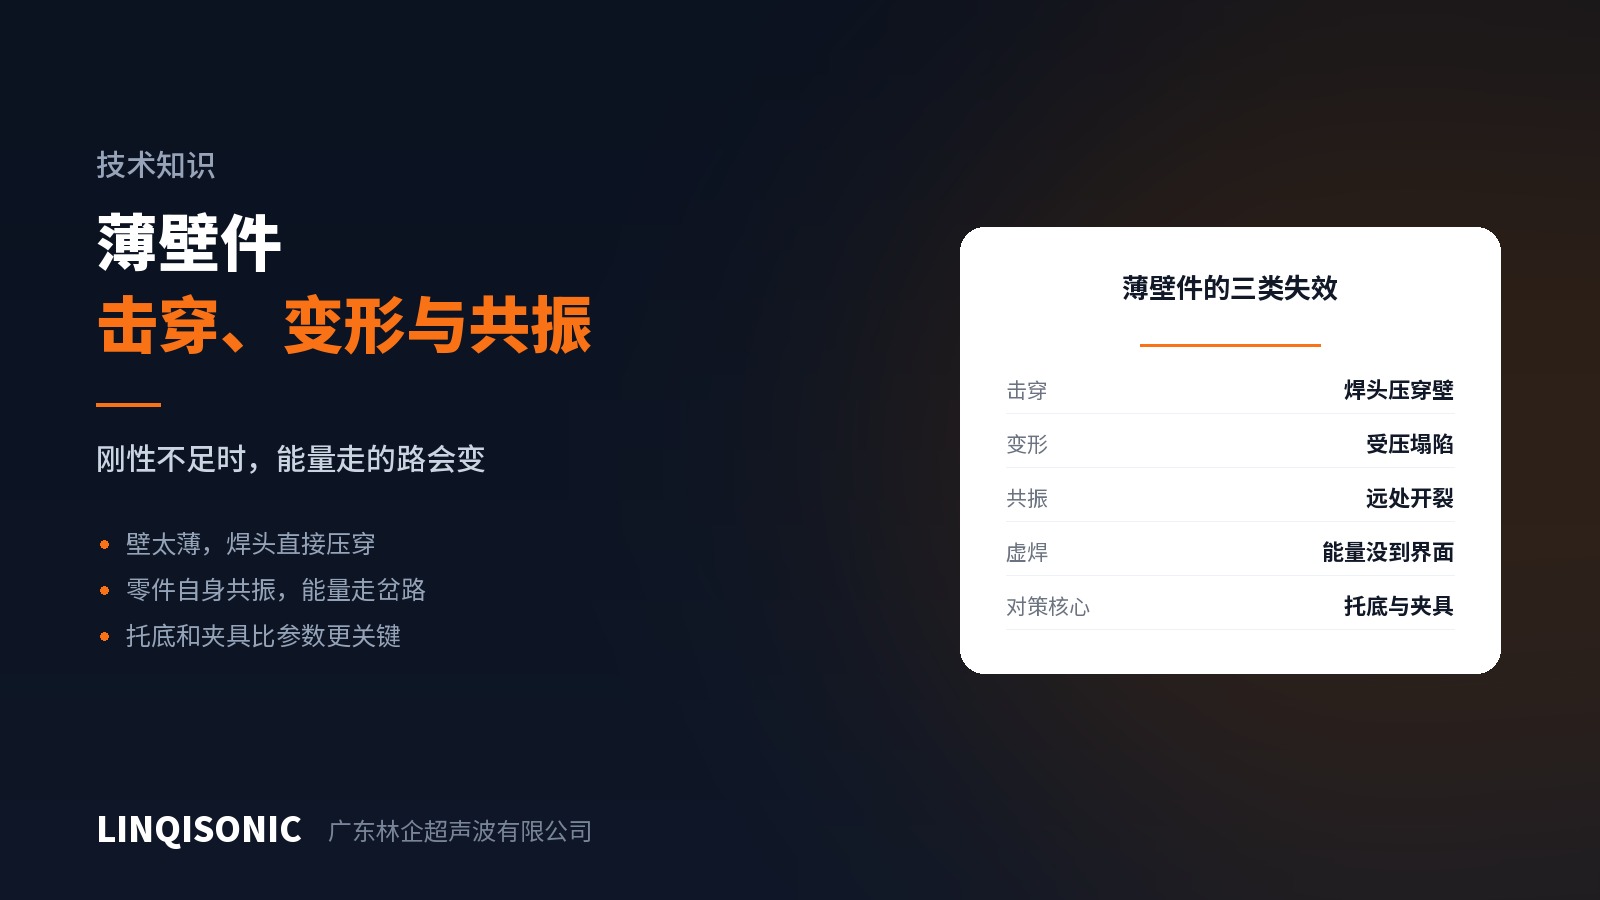
The joint cannot be made. As above. Once the director is incomplete, both the initial contact area and the melt volume run free, and parts from one batch behave very differently.
The part cannot take the force. Thin walls collapse or punch through. The part deforms first, the travel is absorbed by that deformation, and the real pressure at the interface falls far below the setting.
Resonance. Thin walls, cantilevers and large flat faces vibrate as a whole near the ultrasonic frequency, and cracks appear well away from the joint. Such cracks recur in the same place across a batch, unrelated to distance from the weld — the signature of resonance.
Change the approach rather than forcing it
Shear joint. No tiny director; heat comes from sustained friction along an interference fit of a few tenths of a millimetre, far more manufacturable than a 0.075mm director. The side walls must take the lateral force, so thin-walled parts usually need external restraint from the fixture.
Spot welding. No continuous joint, only fusion at discrete points. A small horn, concentrated force and controllable energy per point suit thin walls. Fine where the joint only fixes and does not seal.
Rotary welding. Films, nonwovens and sheet run between a fixed horn and a patterned wheel, and the raised points on the wheel do exactly what an energy director does. This is the mature route for very thin material.
Staking. Where one of the two parts is not thin, stake the thin one in place: no compatibility required and no fusion asked of the thin part.
When a joint is unavoidable
Move up in frequency. Higher frequency means lower amplitude and a gentler mechanical action on thin walls; the trade-off is less power and a smaller area, which small thin parts do not need anyway.
Enlarge the contact area and reduce force and approach speed. Impact at contact is the main source of punch-through.
The nest must follow the contour. Support for a thin part cannot be a few points. This matters more than any parameter.
Restrain whatever resonates. Where remote cracking appears, find the feature that vibrates and add a support point. Resonance needs freedom to move, and restraining it stops it.
Ask one question first
Given a very thin-walled part, ask: does this joint have to seal, or only to hold?
If it only holds, spot welding and staking are both easier than a continuous joint and the tooling is simpler. If it must seal, evaluate carefully — reliable sealing on thin walls is demanding, and a more stable plan is often to let welding or staking fix the parts and give sealing to a gasket, solving the two separately.
Joint forms and the dimensional system are on the downloads page. Frequency options, force and approach speed control are on the ultrasonic welding machine pages.
Send the wall thickness distribution, joint position and sealing requirement to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.