
Energy Director or Shear Joint: When to Switch
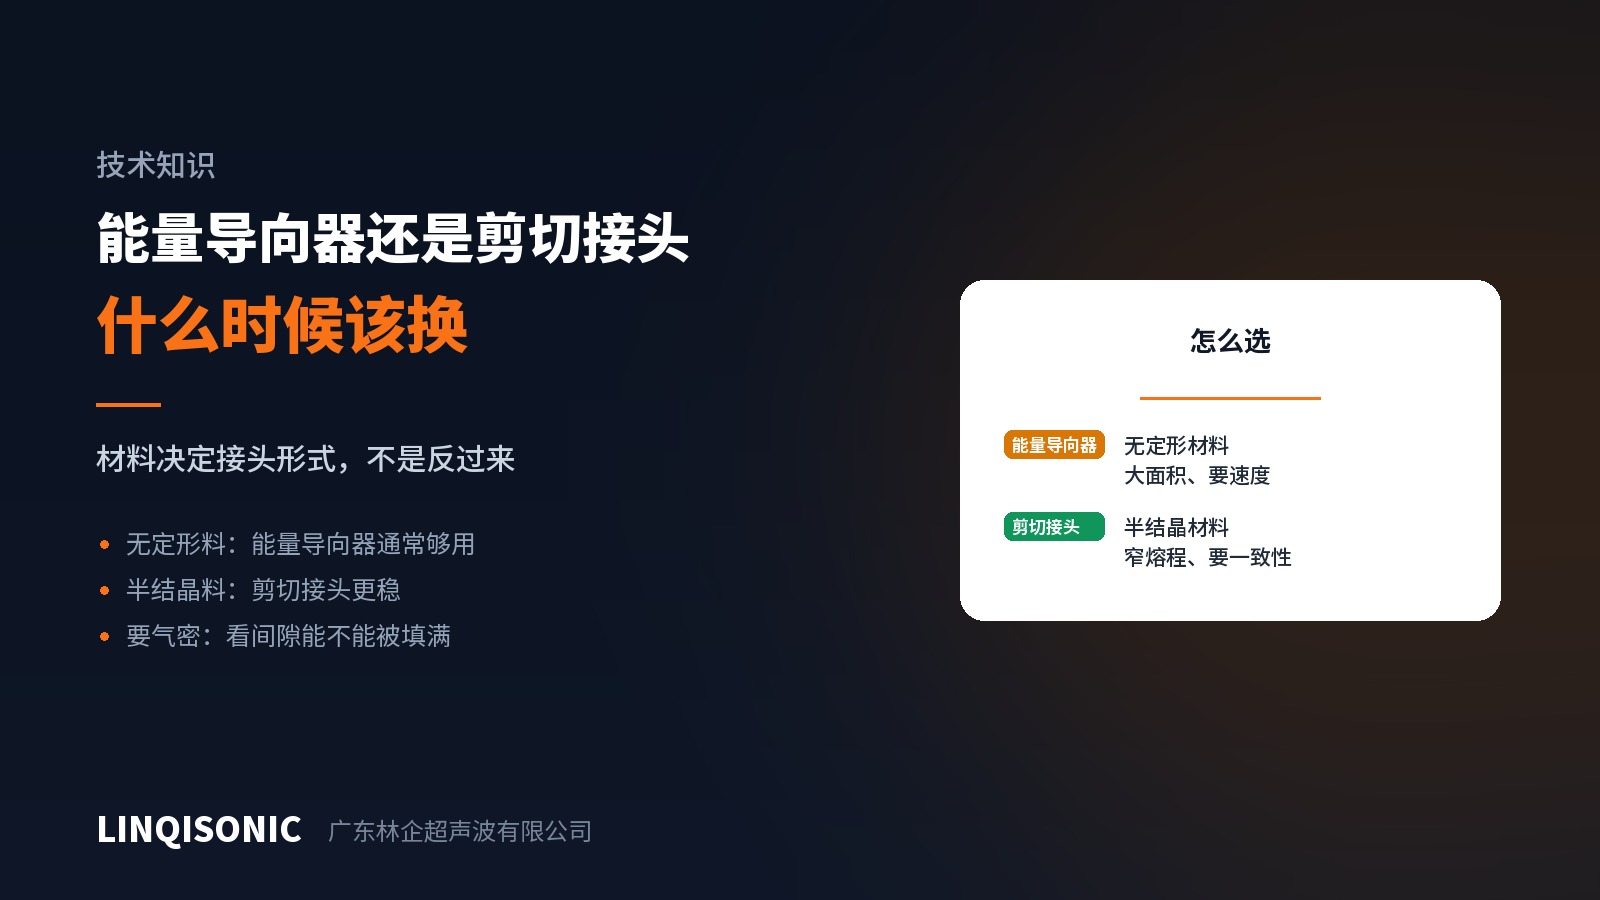
There are many ultrasonic joint forms, but two dominate practice: the energy director and the shear joint. Choose wrongly and no amount of parameter work will fully compensate.
They work in quite different ways
An energy director is a triangular ridge along the joint. Energy concentrates at the tip, melts it instantly, and the melt flows out to fill the gap. Its characteristic is speed — small contact area, rapid onset, well suited to large weld areas.
A shear joint is an interference fit between the two parts. Side walls rub against each other, melting advances progressively down the mating face, and melt stays contained within the fit. Its characteristic is stability — melting is gradual and does not depend on any single instant.
The material decides
Amorphous resins (ABS, PC, acrylic, PS) have a broad softening range with a gradual transition from soft to flowing. The instantaneous melt-and-flow an energy director relies on reproduces easily in these materials, so a director is usually sufficient and faster.
Semi-crystalline resins (nylon, PP, PE, POM, PBT, PEEK) have a defined melting point and a narrow range. They stay solid until temperature is reached, then flow rapidly, with almost no transition. That makes the instant of tip melting hard to reproduce consistently — within one batch some parts fuse fully and others fall short.
A shear joint replaces the instant with a process: friction continues along the mating face and melting advances steadily, insensitive to small variations in time and energy. For semi-crystalline materials, consider a shear joint first — a reliable rule.
Other factors
Hermeticity. A director's seal depends on melt filling the entire joint line; any starved region is a leak path. A shear joint seals through a continuous fused band on the mating face, which is generally more dependable.
Part stiffness. A shear joint requires side walls able to take the lateral force from the interference fit; thin walls or long spans may splay outward. The fixture then has to restrain the part externally, or the design has to revert to a director.
Weld area. Shear joint area grows with engagement depth, and so does weld time. On very large joints the cycle time may not justify it.
Moulding capability. Shear joint interference is typically a few tenths of a millimetre, demanding tool precision and stable moulding. Where the tool cannot hold it, a sound drawing value will not be achieved in production.
A practical order of work
Faced with weak or inconsistent welds, the first instinct is usually to adjust parameters. A faster route is to answer two questions first:
Is this a semi-crystalline resin? If so, the joint form may have been wrong from the outset.
Is it glass-filled? If so, director performance falls with fibre content, and a shear joint again deserves consideration.
Changing the joint form means changing the tool, which is not cheap. But it changes the ceiling; parameter work only finds the best point beneath that ceiling — and when the ceiling is too low, no amount of searching is enough.
The full dimensional system for eight joint types and the selection basis are in the Energy Director & Joint Design Guide, available from the downloads page. Equipment is on the ultrasonic welding machine pages.
Send part drawings to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.