
Turning an IP Rating Into a Welding Process
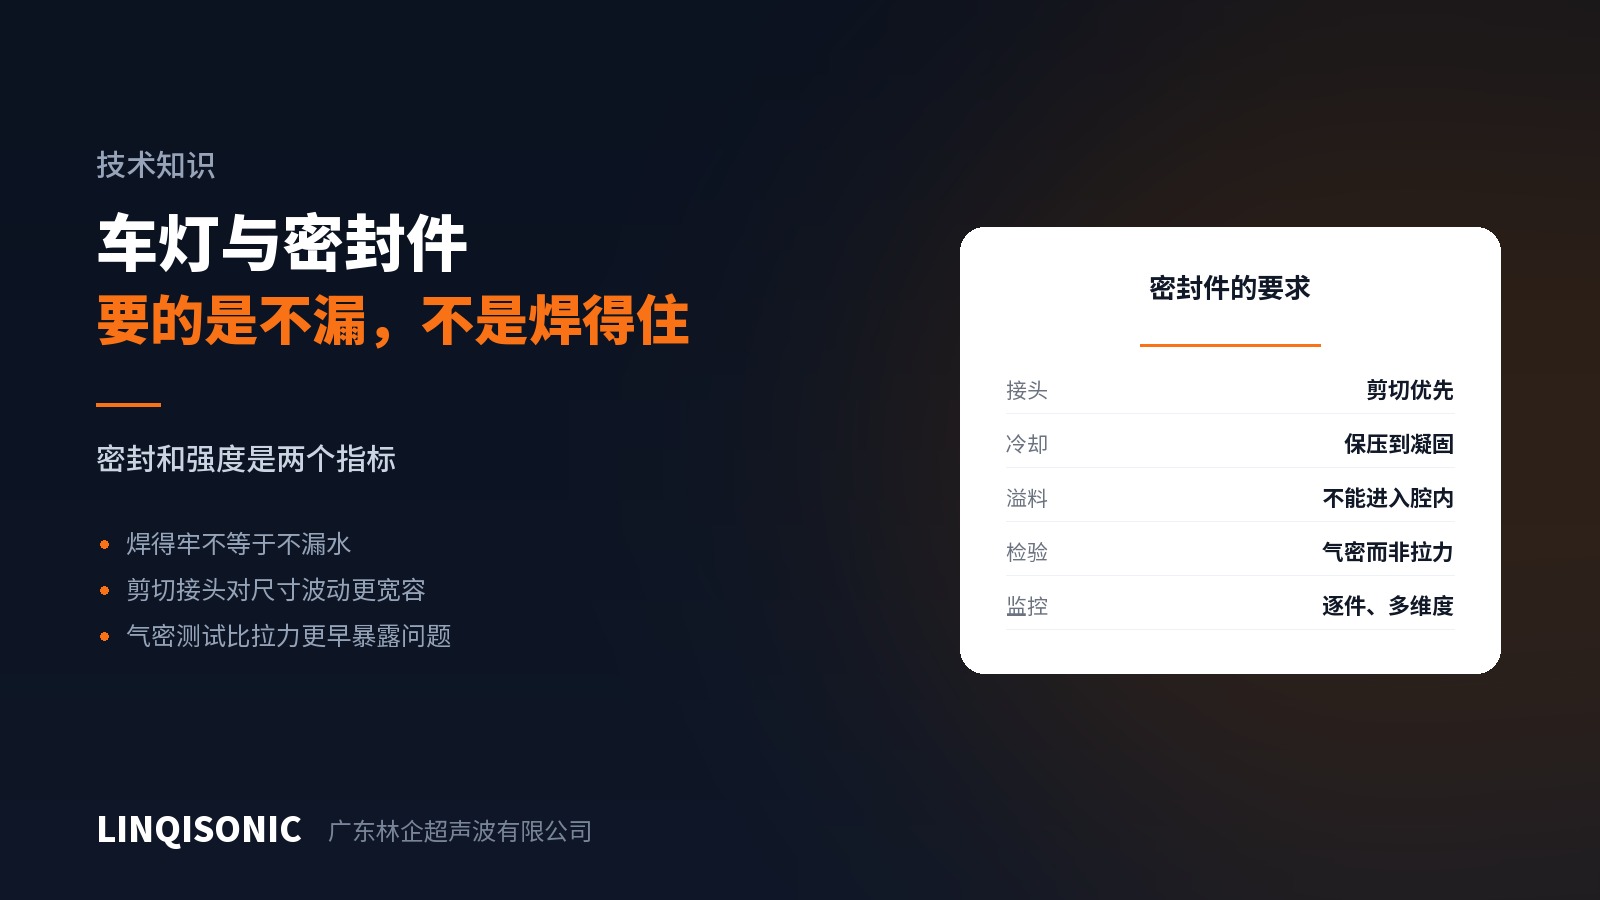
A customer says "this housing needs IP67", and the first job in process engineering is not adjusting parameters but translating that sentence into requirements on the joint.
What an IP code states
The two digits cover protection against solid objects including dust, and protection against water, with the test methods and conditions defined in IEC 60529.
Two common ones: in IP67 the 7 corresponds to temporary immersion, tested at a specified depth for a specified time; in IP68 the 8 corresponds to continuous immersion, with depth and duration agreed between manufacturer and user rather than fixed. That last point is often misunderstood — two IP68 claims are not directly comparable.
Note that an IP test is a type test on the assembly, not an inspection method for a weld. No production line immerses every part, so a line criterion is needed that can be applied to every part and correlated with the type test.
Translating it into a line criterion
The usual approach has three steps.
One: run the type test and establish the correlation. Take a batch, record the production leak rate for each part, usually by pressure decay, then run the immersion test to IEC 60529 conditions and see below which leak rate parts pass consistently.
Two: set the line criterion with margin. Do not sit at the value that just passes; leave room for ageing, thermal cycling and batch variation.
Three: leak test every part and back it with process data. Run pressure decay on every part while recording energy, power and post-weld height, compare against the leak results, and tighten the monitoring limit on whichever dimension proves most sensitive.
What the joint has to deliver
Water protection comes down to a continuous fused band. One discontinuity is a path, however short. So:
Choose a shear joint, forming a continuous fused band on the mating face with the interference providing mechanical sealing besides.
Radius the corners generously. Melt flows poorly into sharp corners and leaves discontinuities; the four corners of a rectangular housing are the most common leak sites.
Do not run the joint across abrupt wall transitions. Shrinkage conditions differ there and leaks follow.
Hold long enough. Shrinkage during solidification, uncompensated, leaves microscopic channels inside the joint.
Give the flange enough stiffness. A soft flange deflects during welding and seating varies along the joint.
Do not forget the first digit
The first digit covers solid objects. What the welding process contributes there is not generating particles itself: control the flash direction so debris does not enter the cavity, keep fixture and station clean, and extract particles from horn wear.
This matters most on electronic assemblies, where debris inside a cavity migrates under vibration and eventually lands where it should not.
And a material layer
Sealing is not only about the joint. The housing material itself has a water vapour transmission rate, so a permanently closed cavity changes humidity slowly even with a perfect weld. Demanding products add a desiccant or select a material with lower transmission — a material and structural design question rather than a welding one.
Joint design, corner treatment and sealing structures are on the downloads page. Hold control and per-part monitoring are on the ultrasonic welding machine pages.
Send the IP requirement, cavity volume and drawings to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.