
Designing the Joint on a Part With Uneven Walls
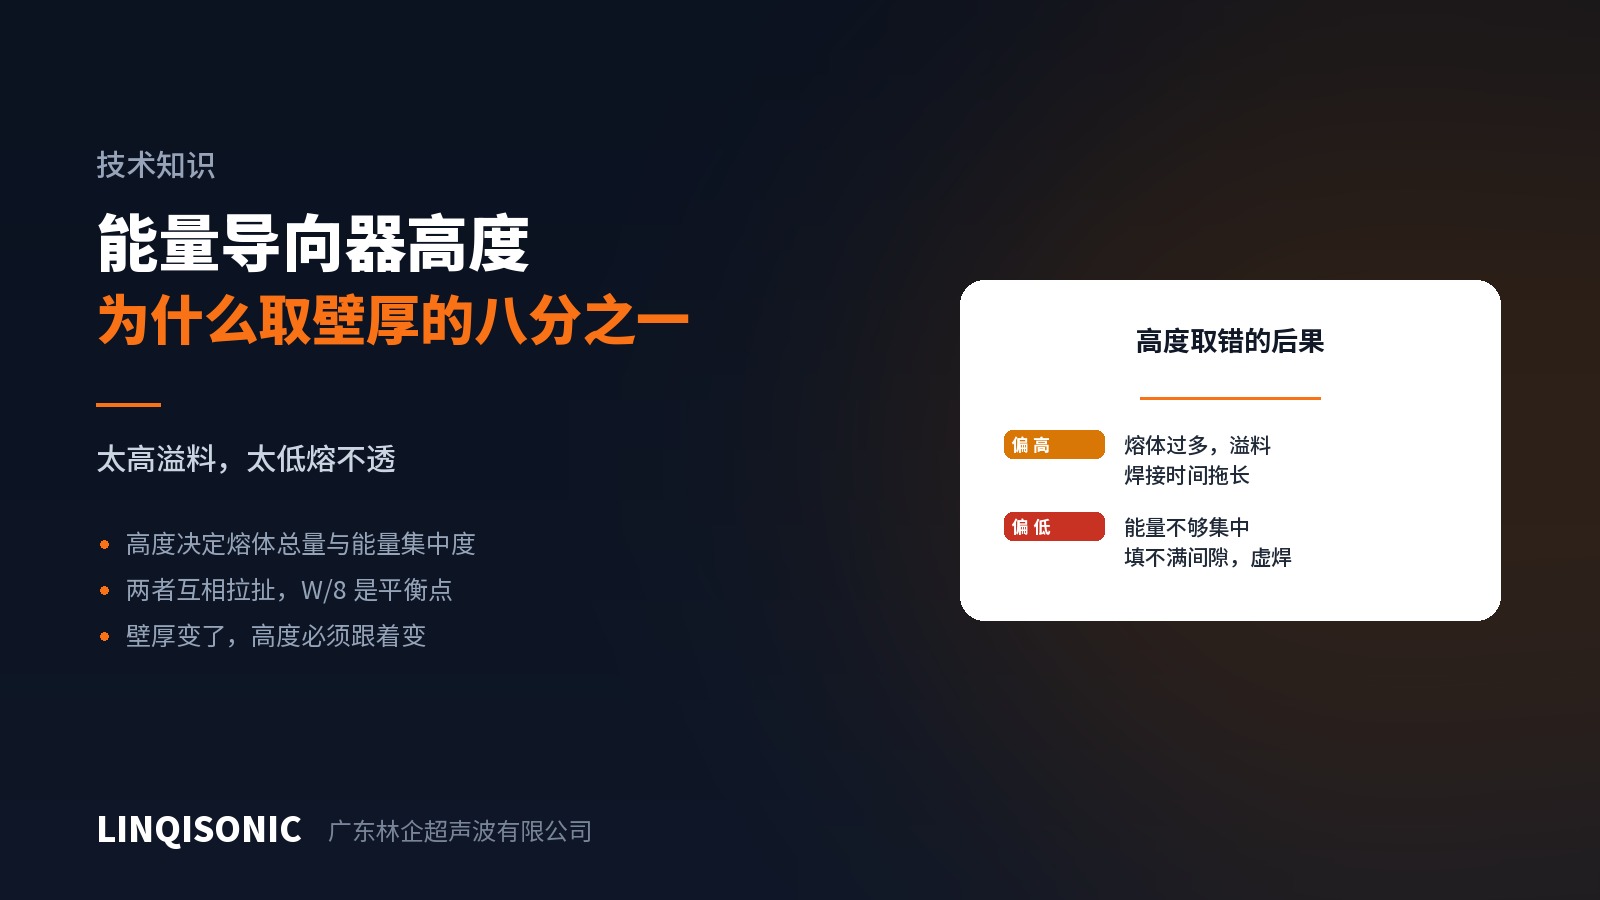
Director height is one-eighth of the wall thickness — everyone knows the rule. The difficulty is that many parts vary in wall thickness along the joint, while the director is still drawn at a single height all the way round.
Why one value will not do
Director height sets two things at once: the volume of resin available to melt and the initial contact area. Take the height from a 3mm wall and the 1.5mm section carries twice the melt it needs.
The thick section may be right while the thin section produces a mass of flash, and a thin wall cannot absorb that heat without distorting or punching through. Set it from the thin wall instead and the thick section has too little melt to fill the gap, leaving discontinuities.
Option one: let the director follow the wall
The most direct answer: take director height from the local wall thickness and vary it in sections along the joint, with smooth transitions rather than steps.
It costs a little more in the tool and far less than fighting uneven flash at the welding station afterwards.
Option two: change to a shear joint
A shear joint generates heat through sustained friction along an interference fit, and melting advances progressively down the mating face, far less sensitive to wall variation than a director. On parts with significant variation, consider it first.
The cost is that the side walls must take the lateral force from the interference. Thin sections may not, and then the fixture has to restrain them externally or the wall has to be thickened locally.
Option three: move the joint
Wall variation is often driven by styling and cannot change, but the joint position frequently can. Placing the joint on a band of relatively uniform wall is far easier than working around it in place — a drawing-stage decision.
Extra risks in the thin sections
Two problems belong specifically to the thin sections.
Punch-through and distortion. A thin wall cannot take the same force and vibration and collapses under the horn. The nest needs close-fitting support there and the contact area should be larger.
Resonance. Thin walls, cantilevers and large flat faces readily resonate near the ultrasonic frequency, and cracks appear well away from the joint. Add support points in the fixture; resonance needs freedom to move, and restraining it stops it.
Choosing the mode
Uneven walls mean the joint fuses at different rates along its length, which suits time mode least of all. Use energy or relative depth mode so the machine adapts to the real condition instead of running a fixed time.
Director height against wall thickness, the dimensional system for eight joint types and the design-review checklist are on the downloads page. Energy and depth modes and fixture options are on the ultrasonic welding machine pages.
Send drawings showing the wall thickness distribution to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.