
Knurled Tooling in Metal Welding: Grip Comes First
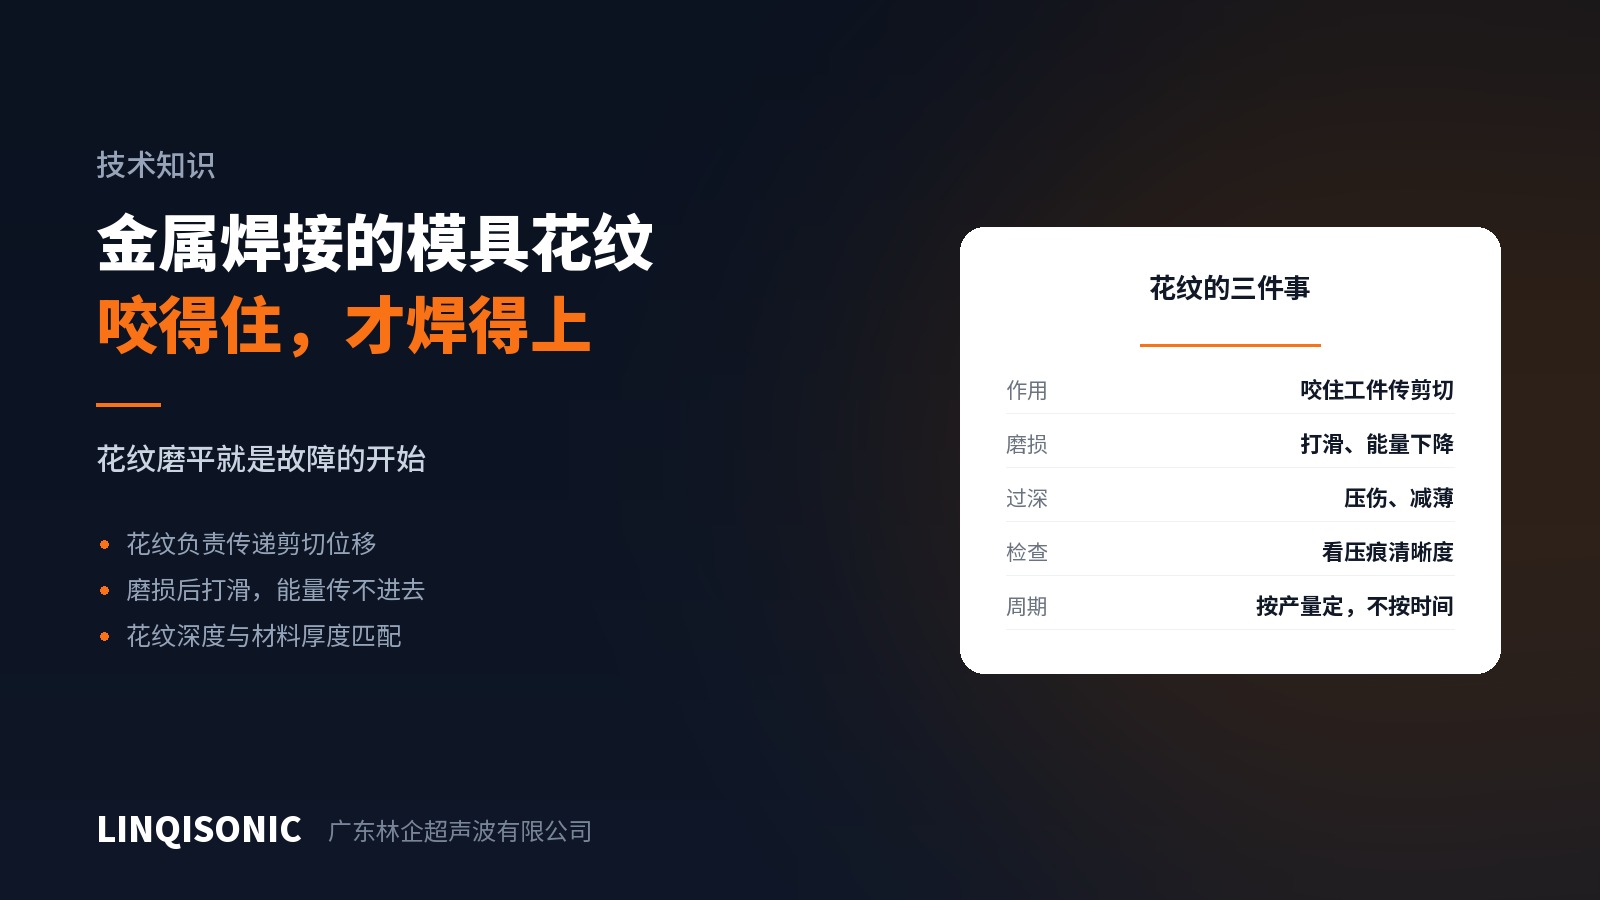
Metal ultrasonic welding works on a completely different principle from plastic. Plastic melts from interfacial friction; metal does not melt. Lateral shear breaks up and displaces the oxide and contamination on the contact faces, bringing fresh metal atoms into direct contact for a solid-state bond.
The whole process depends on one thing: the shear motion actually reaching the work.
What the knurl does
Both the horn face and the anvil carry a knurled or toothed pattern. They grip the workpieces so that the horn's lateral motion carries the upper part with it while the anvil holds the lower part still. Relative sliding occurs between the two layers, and the bond forms at that sliding interface.
If the knurl cannot grip, the horn simply slips on the surface — all the energy is spent between horn and workpiece instead of between the two workpieces. The symptoms are weak welds, bright wear marks on the part, and a hot horn.
Knurl wear is the usual cause of trouble
The pattern carries high-frequency shear under load continuously, so wear is inevitable. Once worn:
Grip falls away — slipping begins and weld strength gradually declines.
The decline is gradual — which is the difficult part. Nothing fails one morning; strength drifts down, and by the time sampling catches it a good many parts may have passed.
Judge by the impression on the part. A crisp, clearly defined pattern means the tooling is sound; a blurred, flattened or locally absent pattern means it needs replacing or reworking. This is the simplest and most reliable daily check.
Set the replacement interval by piece count, not by calendar. The same tooling running two hundred a day and two thousand a day are entirely different lives.
Choosing knurl depth
Deeper is not better.
Too shallow — no grip, slipping.
Too deep — an excessive impression in the part, thin foil pierced, conductor section thinned to the detriment of conductivity and strength.
Depth must match material thickness. Tooling for thin foil and tooling for busbars are not the same tooling, and this is not a place to compromise.
Horn and anvil have different jobs
The horn drives the upper workpiece, and its pattern must transmit shear.
The anvil holds the lower workpiece still. If its grip is inadequate, the lower part moves with the upper, no relative sliding occurs, and nothing bonds.
When troubleshooting weak welds, check both — not only the horn.
Daily practice
Check the impression every shift. One part, pattern clarity, more direct than any instrument.
Clean regularly. Metal debris and oxide accumulate in the grooves, and a packed pattern is a shallow pattern. Use a soft brush and a suitable cleaner; never scrape the faces with anything hard.
Keep a spare set. Wear is gradual, and there is no time to make new tooling once the line has to stop.
Log piece counts. A cumulative weld count per tool set beats recollection.
Frequency
Metal ultrasonic welding commonly runs at 20, 30, 35 and 40 kHz. Large conductors and busbars usually sit at 20 kHz, while fine harnesses and small spot welds move higher — the smaller and thinner the work, the higher the suitable frequency.
Frequencies, tooling sizes and knurl selection by machine are on the ultrasonic welding machine pages. Send material, thickness and conductor section to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.