
Acoustic Stack Maintenance: The List That Belongs on the Machine
Unplanned stoppages on ultrasonic welders are rarely a failed generator. Most accumulate from small, unattended things in the acoustic stack.
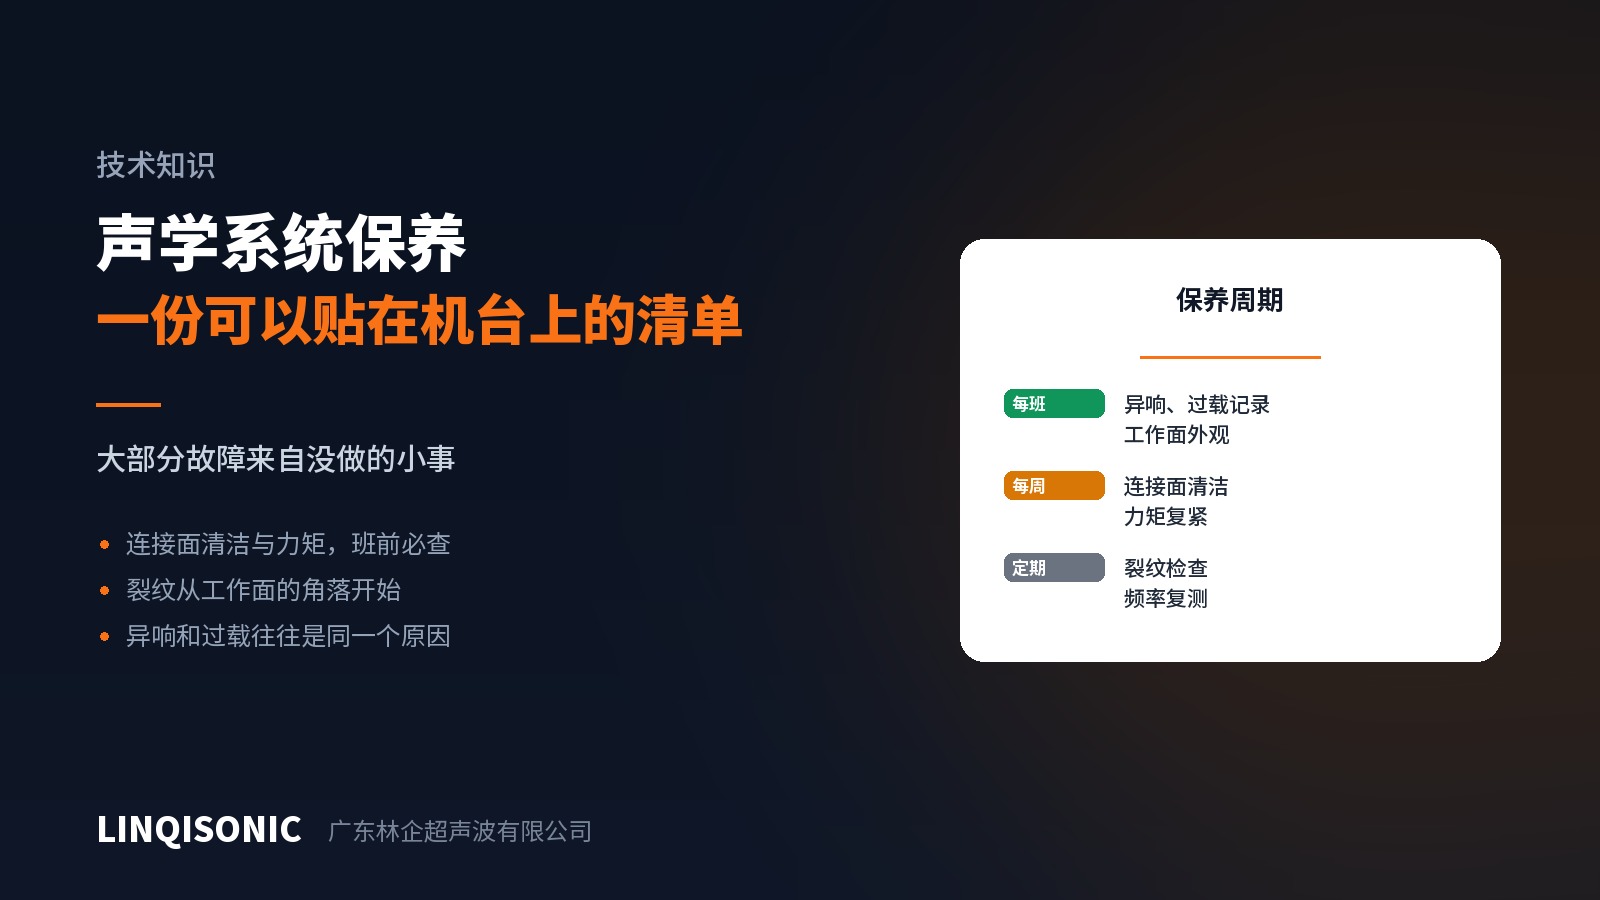
Every shift
Listen. Normal operation gives a steady high-frequency tone. A shrill squeal, a wavering pitch, or noticeably more noise than usual all warrant stopping. Abnormal sound almost always means the resonance condition has changed.
Check overload records. An occasional overload may be one bad part; repeated overloads are a system problem. Do not simply reset and carry on each time.
Inspect the working face. Look for adhered material, wear, or polished bright areas. Adhesion changes the contact condition; wear changes dimensions and therefore frequency.
Every week
Clean the mating faces. Converter-to-booster and booster-to-horn faces must be clean. These are the path for all the energy, and any contamination or bruising causes loss and heating there. Treat the faces as the manufacturer specifies after cleaning.
Re-torque. Use the specified value, not feel. Too little torque allows relative sliding, heating and energy loss; too much damages threads and end faces.
Check the slide and pneumatics. The stroke should be smooth and free of sticking, with stable pressure. A rough stroke shows up directly as poor weld consistency.
Periodically
Crack inspection. Horn cracks typically begin at stress concentrations — face corners, slot ends and thread roots. Inspect with a magnifier or dye penetrant. A cracked horn must be taken out of service; cracks propagate quickly and end in sudden failure.
Frequency check. Wear, re-machining or a drop shifts the resonant frequency. Measure the actual frequency and confirm it remains within tolerance.
Amplitude distribution. Particularly for wide horns: run a weld into thermal paper under the face and read the evenness of the mark.
Reading a few symptoms
Overload on start — usually an abnormal resonance condition: a cracked horn, drifted frequency, a loose joint, or mismatched components. Start once with no load; overloading unloaded confirms the stack itself.
A hot horn — some temperature rise is normal, but a distinctly hot horn means energy is being dissipated inside it, generally from a crack or a poor mating face.
Same parameters, worse results — check horn wear and joint torque first, then fixture and incoming parts, and only then suspect the generator.
On spares
Horns are consumables. Keeping one spare of each common size costs far less than a line stopped waiting for a new horn — especially for long-running tooling whose drawings may no longer be to hand.
Maintenance items, common spares and stack configurations by model are on the ultrasonic welding machine pages. For maintenance or spares, call +86 769 8202 9510 / +86 137 6001 0932, or write to 1427498429@qq.com.