
The Acoustic Stack: Converter, Booster and Horn
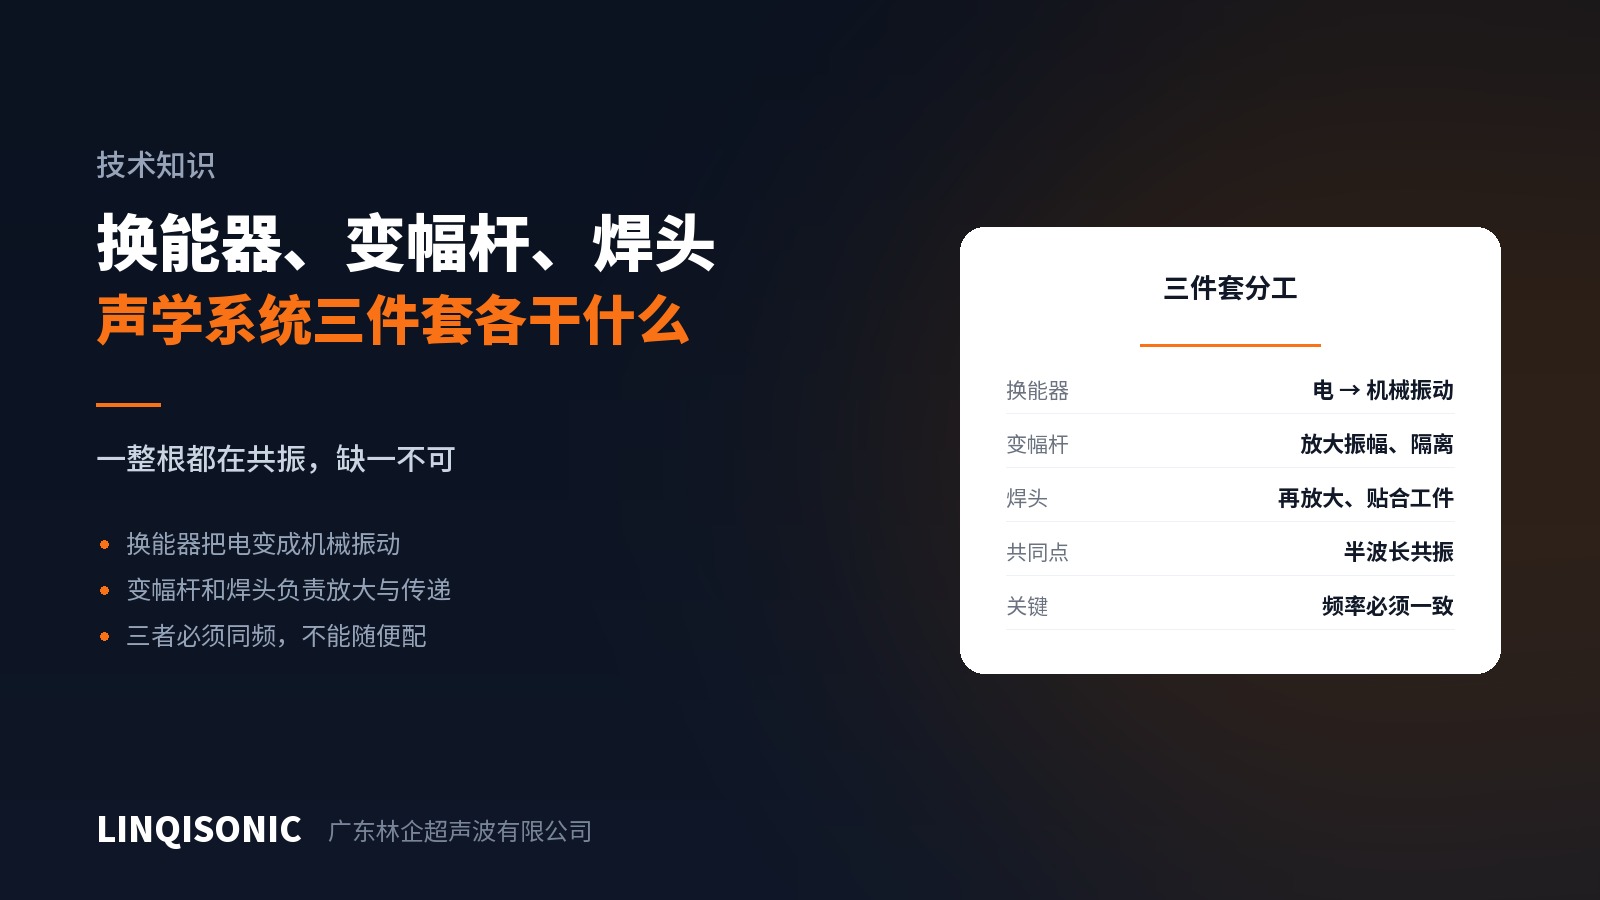
Between the high-frequency electrical energy leaving the generator and the mechanical vibration reaching the part, three components stand in series. Together they are called the acoustic stack.
Converter: electricity into vibration
A converter contains piezoelectric ceramic discs that expand and contract under an applied high-frequency voltage, producing mechanical vibration. This is the energy conversion step.
The amplitude a converter produces is modest and insufficient to weld on its own. Its job is conversion; amplification comes later.
Booster: amplification and mounting
The booster sits between converter and horn and serves two purposes.
Amplitude gain. Its two ends differ in cross-section, and vibration passing from the larger to the smaller section increases in amplitude — a direct consequence of energy conservation. The ratio is its gain.
A place to clamp. The whole stack vibrates, and only a point of zero displacement — a node — can be held. The centre of the booster is exactly such a node, and the mounting ring in the head clamps there. Without a booster, the stack has no suitable mounting point.
Horn: final gain and delivery
The horn contacts the part directly. Its shape follows the part contour while still contributing gain of its own.
A horn design must satisfy three requirements at once: match the part, resonate at the working frequency, and hold amplitude sufficiently uniform across the working face. These constrain each other, which is why horns are designed for the job rather than approximated from stock.
Why frequency must match
All three components are dimensioned to half a wavelength, so that in series the stack resonates at the working frequency and transmits vibration efficiently.
If one component's resonant frequency drifts — a horn machined too long, worn, or a 20 kHz horn fitted to a 40 kHz machine — the stack cannot resonate properly. The symptoms are generator overload, failure to start, or an unusually shrill noise.
The three parts therefore cannot be mixed freely. Replace a horn with one of the same frequency, and change gain by changing the booster rather than machining the horn.
Total gain
Overall amplification is approximately the product of booster gain and horn gain. To raise amplitude, fit a higher-gain booster or redesign the horn — the first is easy, the second means new tooling.
Higher gain is not automatically better. Excessive amplitude raises stress in the horn, shortens its life, and makes marking and thin-wall damage more likely. Appropriate beats maximum.
Frequencies, gain ranges and maximum horn sizes by machine are on the ultrasonic welding machine pages. Send part drawings for horn design to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932.