
Weld Force and Amplitude Work Against Each Other
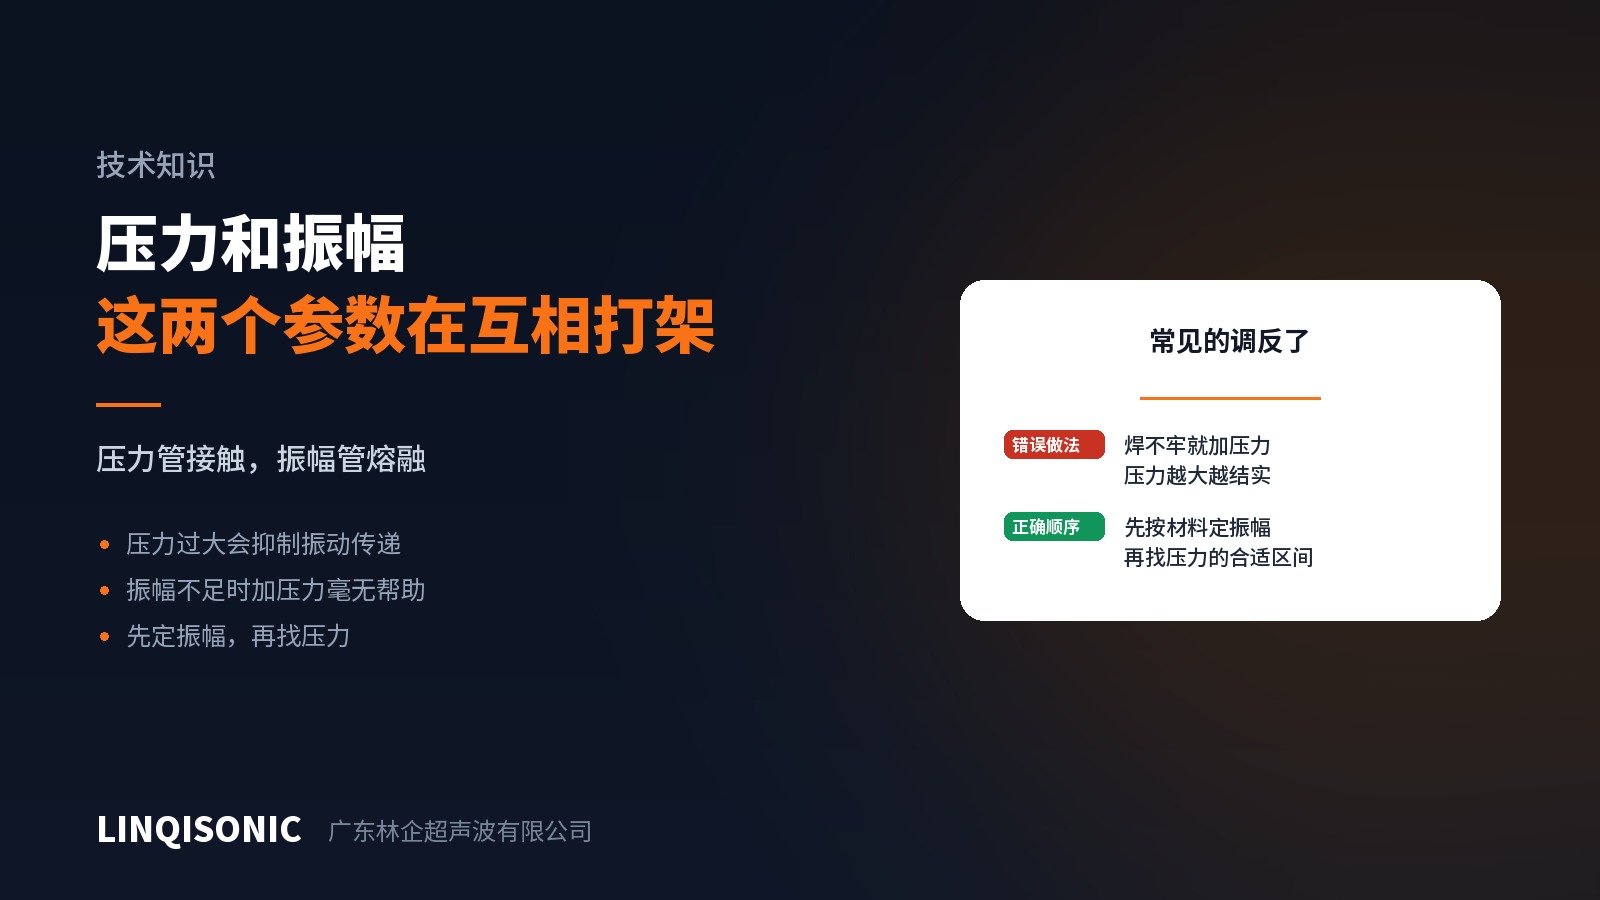
"If it will not weld, add force." This is the most common mistake on the shop floor — and it usually makes matters worse.
The two parameters do different jobs
Force keeps the two faces in contact and, once melt forms, consolidates it and fills the gap. It generates no heat.
Amplitude creates relative motion across the interface and generates heat by friction. Heat comes from amplitude, not from force.
That distinction underpins everything else.
Why too much force is worse
Vibration has to reach the interface and produce relative slip there. Under excessive force the faces are pressed together so hard that relative motion at the interface is suppressed — the vibration arrives, but the interface cannot move, and frictional heating becomes less efficient.
At the same time, excessive force squeezes freshly formed melt out of the joint as flash. With the melt displaced, there is less left to fill the joint.
The typical symptom: after adding force, marking is heavier, flash is greater, and joint strength is unchanged or lower.
Force cannot be too low either
With insufficient force the faces seat poorly and a gap remains. Vibration reaches the interface but cannot cross it — air in between breaks the energy path. Weld time lengthens noticeably, melting is slow to start, or nothing welds at all.
And if melt is not consolidated by adequate force, voids remain inside the joint on cooling; the part looks welded but leaks on test.
The right order
First, set amplitude by material. Requirements differ substantially between material families, with semi-crystalline and glass-filled grades needing more. This step decides whether the joint can be made at all — it sets the ceiling.
Second, find the force window at that amplitude. Start low and increase, watching weld time and joint quality. There is a band: below it melting starts poorly; above it flash increases while strength does not.
Third, and only then, adjust time or energy. Without the first two settled, this step merely compensates for earlier problems.
A diagnostic
If adding force shortens weld time and raises strength — force was previously too low and seating was poor.
If adding force barely changes weld time but increases flash and marking — the useful band has been passed; go back.
If adding force lengthens weld time — force is now clearly excessive and interface motion is being suppressed.
Amplitude requirements by material family are in the Amplitude Reference Guide on the downloads page. Amplitude ranges and force control by machine are on the ultrasonic welding machine pages.