
Why the Energy Director Is One-Eighth of the Wall Thickness
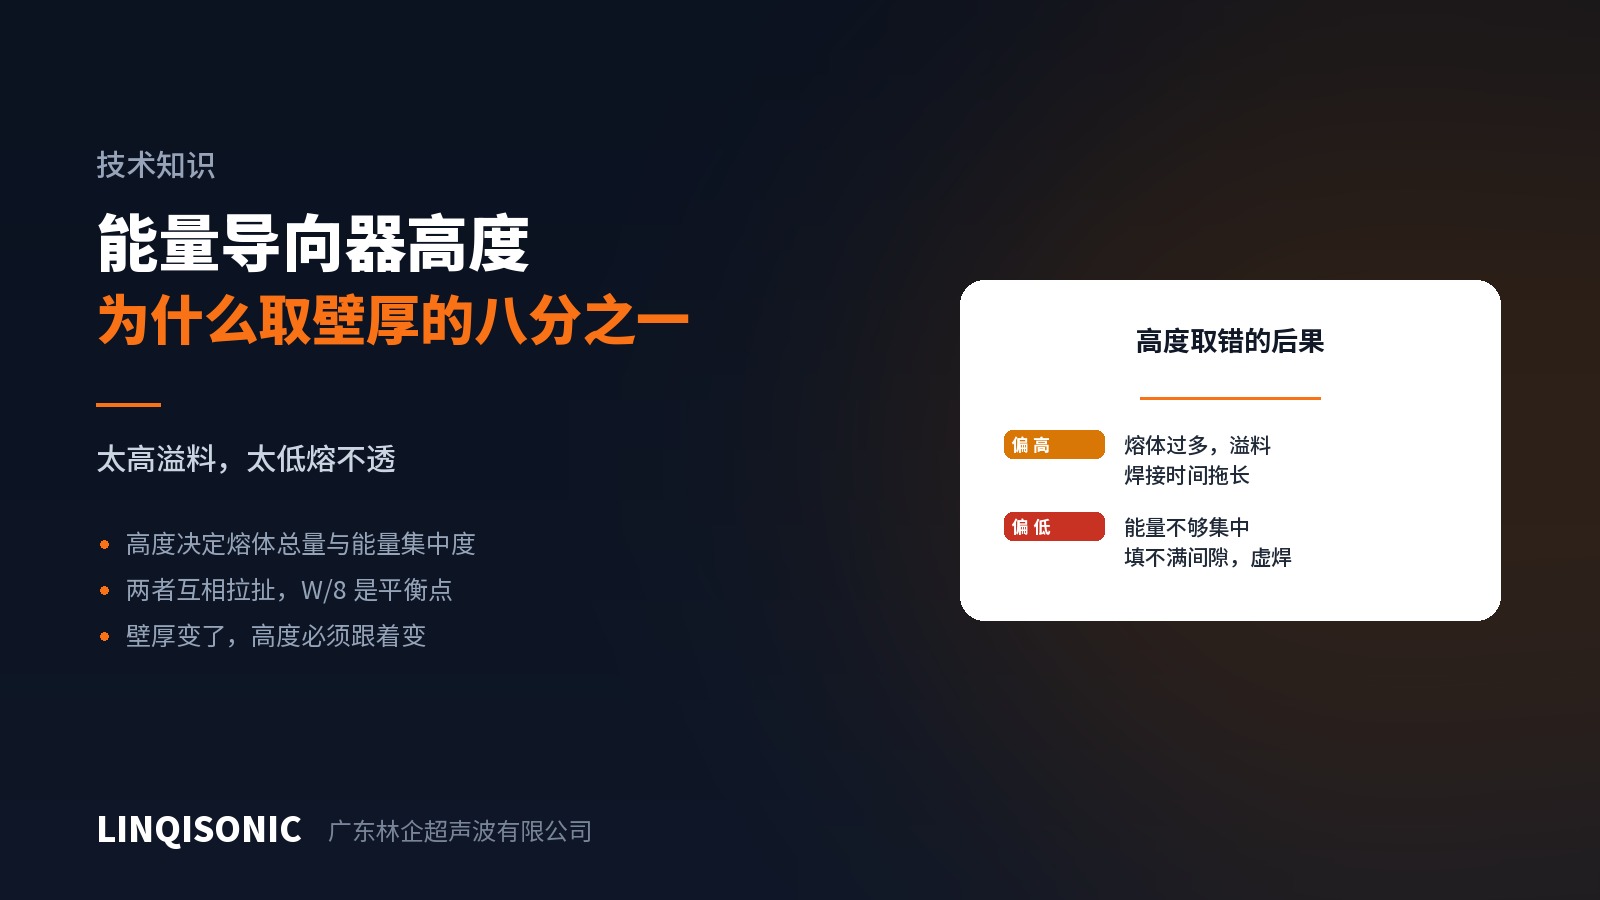
The most widely quoted rule in ultrasonic joint design is that the energy director should be one-eighth of the wall thickness.
Where does that come from, and why not a tenth, or a fifth?
Height governs two things at once
The energy director is a triangular ridge along the joint line. At the start of the weld only its tip touches the opposing face, so all the energy concentrates on that very fine line and melts it rapidly; as melting advances the contact area grows and melt flows out to fill the gap.
Its height sets two things simultaneously.
The volume of resin available to melt. Melt has to fill the gap between the two faces for a complete weld. Too little height means too little melt, and unfilled regions remain along the joint — invisible from outside, but that is where hermeticity and strength are lost.
The concentration of initial energy. A taller, sharper director gives a smaller initial contact area, higher energy density and faster onset of melting. A short director starts with a larger contact area, so energy is spread and heat dissipates before the interface melts.
Why these pull against each other
Taller looks better — more melt, faster start. But as height increases:
melt volume exceeds the gap and the surplus is squeezed out as flash, which is not only unsightly but interferes with assembly and sealing faces;
the melt path lengthens and weld time grows, giving heat more opportunity to spread into the part body and cause overheating or distortion around the joint;
the director itself becomes harder to mould, with short shots or rounded tips at the apex, so consistency falls rather than rises.
W/8 is the empirical value where those constraints meet — enough melt for a typical gap, a small enough initial contact area for rapid onset, and a feature that still moulds reliably.
When to depart from it
It is a starting point, not a conclusion. Adjust where:
hermeticity is required — usually more melt is needed, so height can increase, together with adequate weld depth;
the resin is glass-filled — there is less resin to melt in the first place, and simply raising the director achieves little; the joint form usually has to change;
the resin is semi-crystalline — the instantaneous melt-and-flow the director depends on is hard to reproduce, and a shear joint is generally better;
wall thickness varies — director height should follow local wall thickness rather than one dimension all the way round.
The more common mistake
In practice the usual error is not picking the wrong ratio but changing the wall thickness and forgetting to change the director. Wall goes from 2mm to 3mm, the director stays as it was, and weld quality degrades for reasons nobody can trace.
Included angle, weld depth, interference bands and the full dimensional system for eight joint types are in the Energy Director & Joint Design Guide, available from the downloads page.
Send part drawings to 1427498429@qq.com, or call +86 769 8202 9510 / +86 137 6001 0932. Equipment is on the ultrasonic welding machine pages.